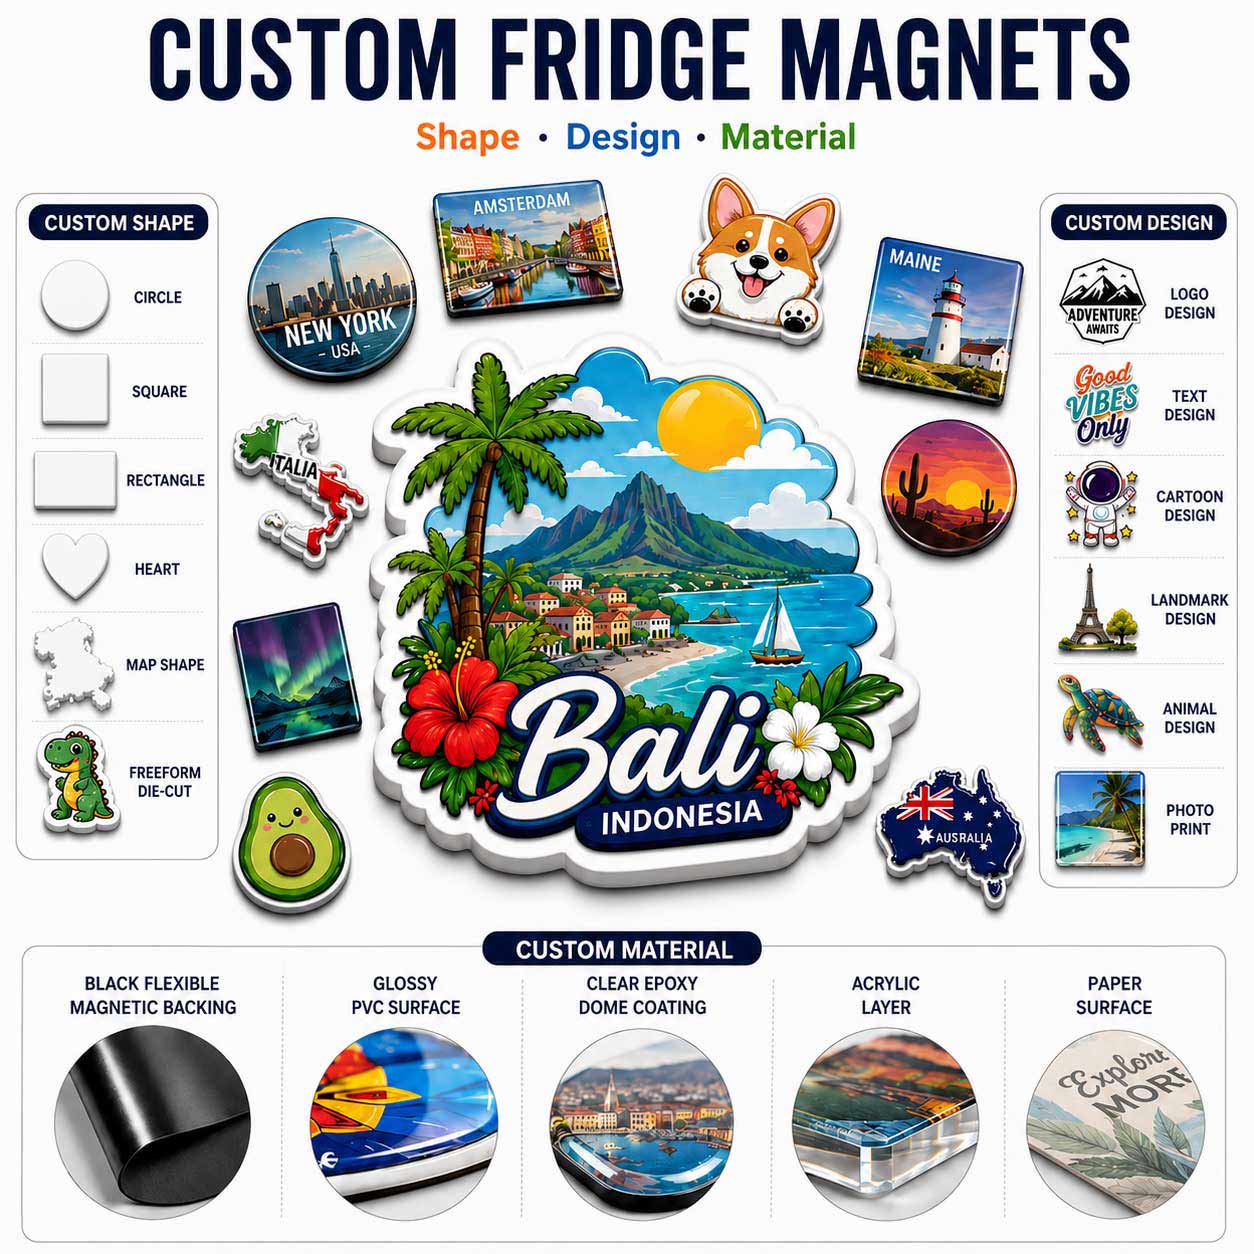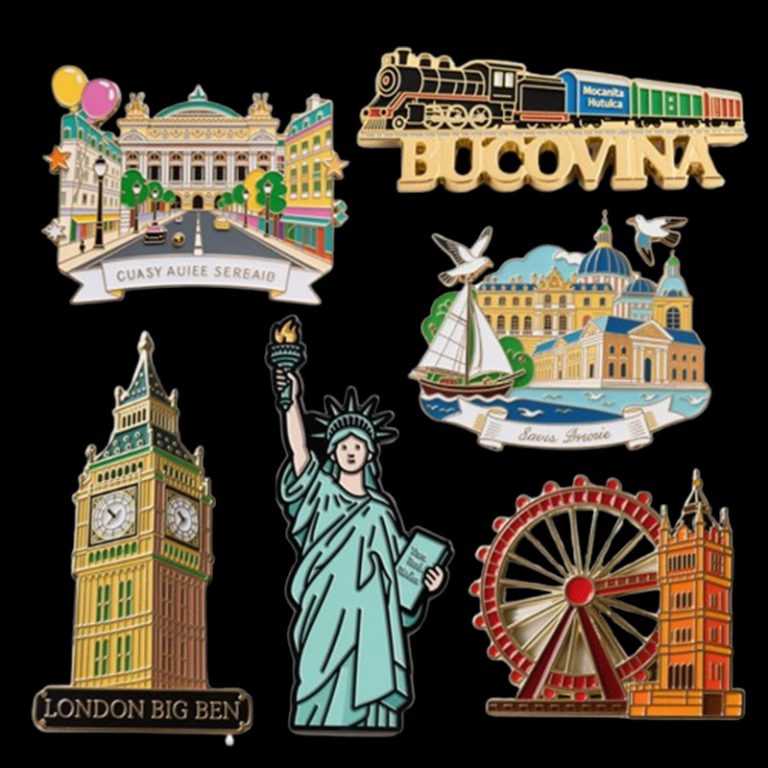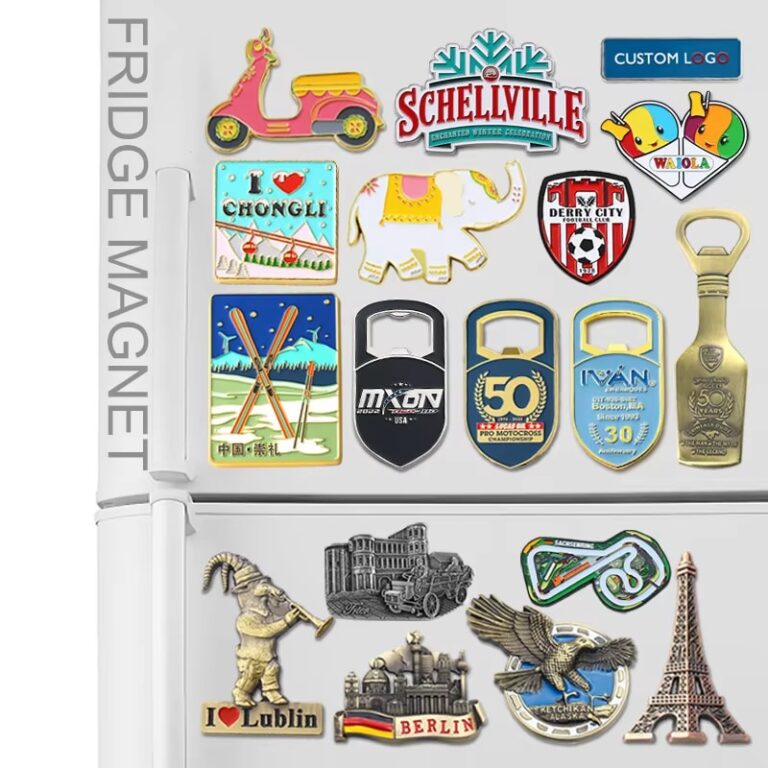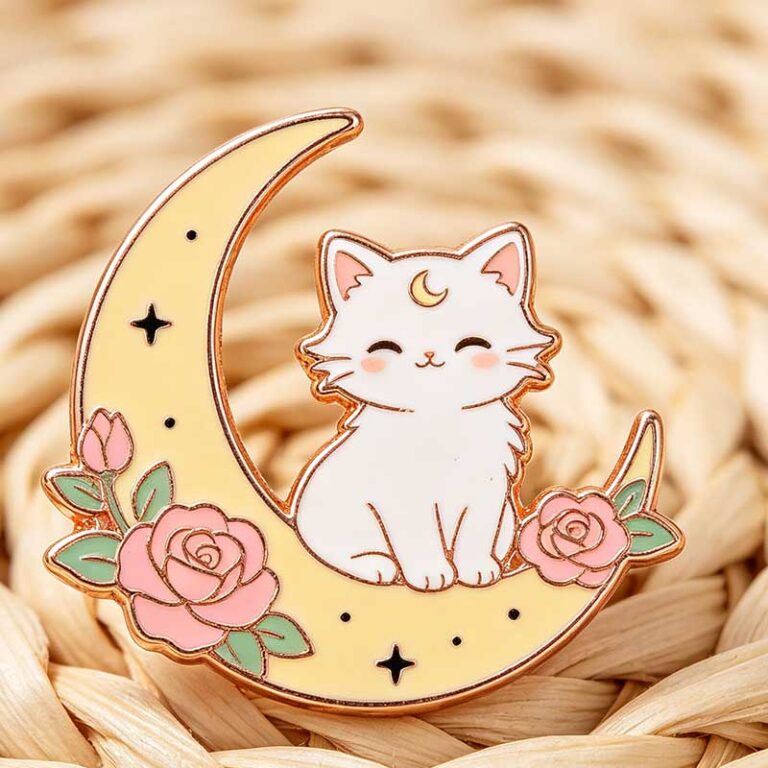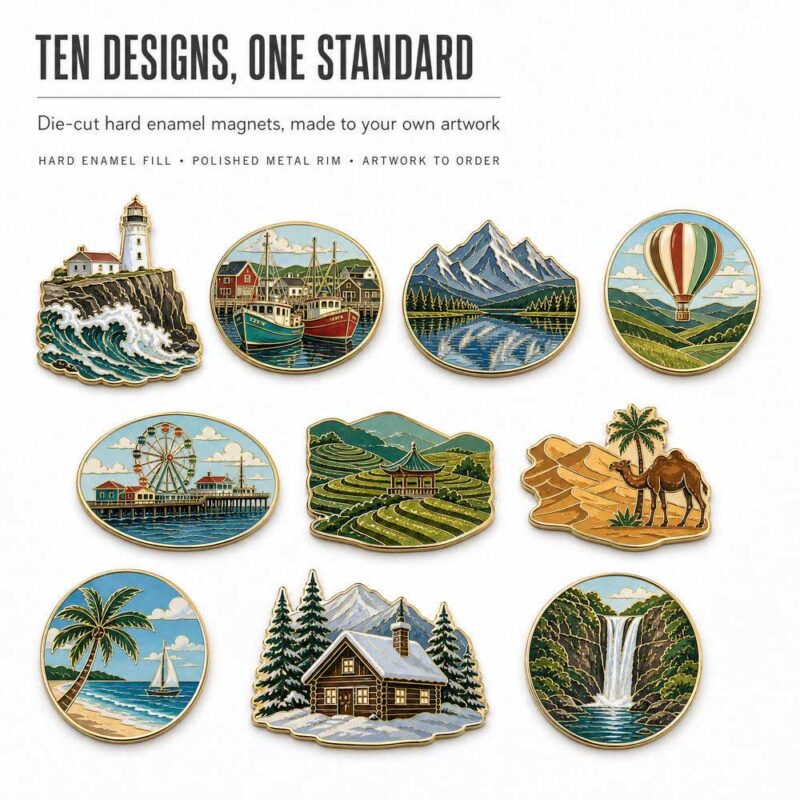
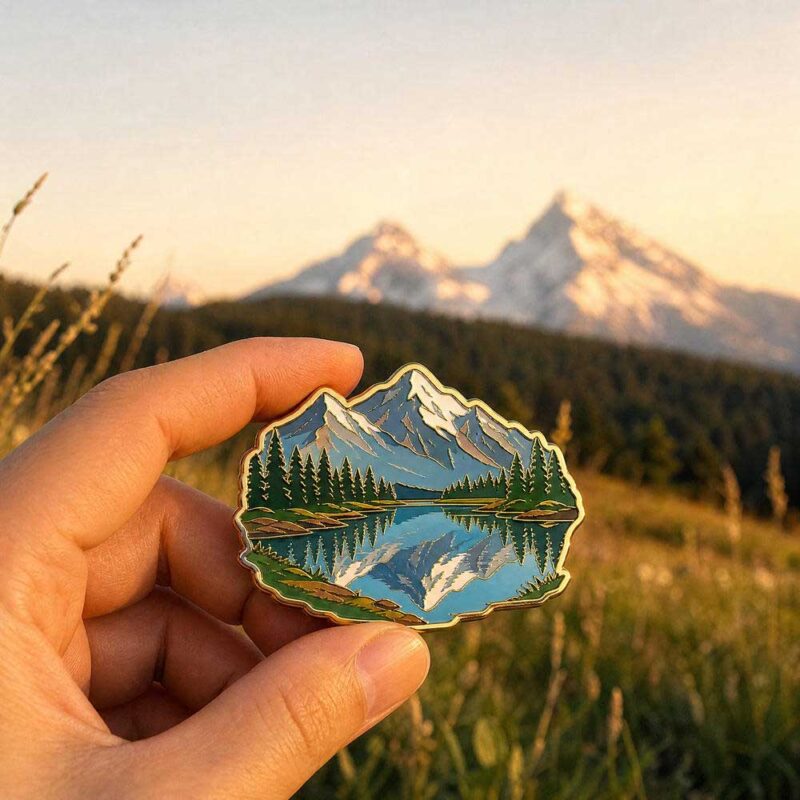
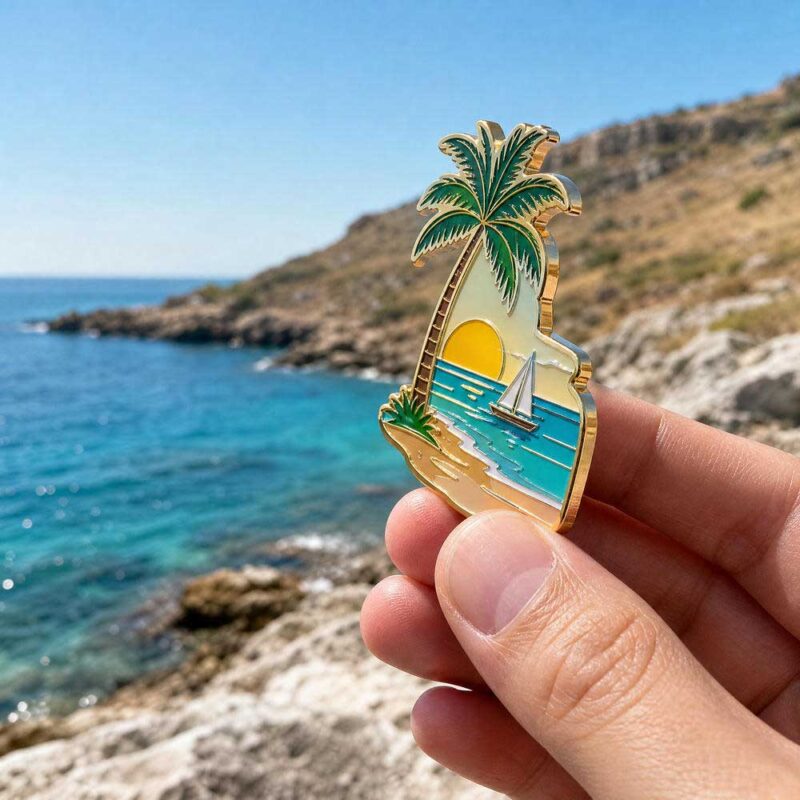
Custom Enamel Fridge Magnets for Souvenir Programs

product banner
主图 05
主图 03
主图 02
nature desert camel irregular white processed
nature alpine cabin irregular white processed
nature tropical beach round white processed
nature lighthouse cliff irregular white processed
nature lighthouse peak irregular white processed
主图 06
主图 05
主图 03
主图 02
nature desert camel irregular white processed
nature alpine cabin irregular white processed
nature tropical beach round white processed
nature lighthouse cliff irregular white processed
nature lighthouse peak irregular white processed
主图 06
Custom Enamel Fridge Magnets for Souvenir Programs
Description :
  • Porcelain-smooth tactile prestige with razor-sharp artwork fidelity. Die-cast from dense Zamak 3 zinc alloy (6.6-6.7 g/cm³) and hand-filled with mineral enamel pastes. Successive water-stone lapping polishes the metal retaining ridges and rich color fields to a co-planar, glass-smooth finish (3.5H-4H surface hardness) that will not snag fabrics or collect grime on tourist gift racks.
  • Sub-flush neodymium holding power with surface protection. Fitted with dual sintered NdFeB N35 rare-earth disc magnets anchored inside molded sub-flush pockets with cross-pattern air relief channels. Delivers verified vertical shear capacity holding 6 to 8 sheets of A4 copy paper on steel panels without downward drift, backed by full-coverage microfiber velvet pads to shield appliance finishes from contact scuffs.
  • Rapid 2-4h engineering proofs with 2-year factory mold archive. Receive complimentary production-ready color layout proofs within 2 to 4 working hours, physical evaluation samples in 5 to 7 working days, and your custom tooling stays cataloged in our factory archive for 2 years with zero reorder mold fees.
Base Metallurgy & Density High-pressure die-cast Zamak 3 zinc alloy (6.6-6.7 g/cm³)
Standard Dimensions Length: 55 mm to 80 mm (2.17″ to 3.15″); width: 45 mm to 65 mm; thickness: 3.0 mm to 4.0 mm
Enamel Technique & Surface Flush stone-polished imitation hard enamel (coplanar surface); mirror gold or nickel plating
Magnet Retention System Dual sub-flush sintered NdFeB N35 discs (11.7-12.2 kGs); Ni-Cu-Ni triple plating
Production Turnaround 3D proof: 2-4 working hours | Samples: 5-7 working days | Mass run: 12-18 working days
Tooling Retention 2 years free archive retention (renewed automatically on reorders); $0.00 mold fee on reorders
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Metallurgy & Density High-Pressure Die-Cast Zamak 3 Zinc Alloy (6.6-6.7 g/cm³) Explore Custom Fridge Magnets Collection
Enamel Technique & Surface Finish Imitation hard enamel (Epola resin); multi-stage rotary stone lapping to 100% flush coplanar finish (3.5H-4H surface hardness)
Dimensional Envelope Length: 55 mm to 80 mm (2.17″ to 3.15″); width: 45 mm to 65 mm (1.77″ to 2.56″); overall plate thickness: 3.0 mm to 4.0 mm
Tooling & Outer Boundary Tolerances Tooling cavity CNC tolerance: ±0.03 mm (±0.0012″); finished die-cut casting profile: ±0.08 mm to ±0.12 mm after edge buffing
Line Width & Enamel Recess Depth Minimum metal separating line width: ≥ 0.25 mm (0.010″); minimum enamel reservoir depth: ≥ 0.35 mm
Magnet Assembly & Magnetic Strength Dual sub-flush sintered NdFeB N35 rare-earth discs (residual induction 11.7-12.2 kGs); Ni-Cu-Ni triple electroplated
Magnet Retention & Safety Cavity Molded sub-flush pocket (0.08 mm deeper than magnet); cross-pattern air relief vents; structural epoxy pull resistance ≥ 50 N
Holding Performance Benchmark Vertical holding capacity supports ≥ 6 to 8 sheets of 80g A4 copy paper on standard cold-rolled steel panels
Surface Plating & Protective Sealing Genuine gold plating, bright imitation rhodium/nickel, black nickel; sealed under baked acrylic clear coat (8-12 μm, 3H)
Corrosion & Adhesion Certification 48-Hour Neutral Salt Spray (ASTM B117) with zero blistering or plating peel; cross-hatch tape adhesion to ASTM D3359 Grade 5B
Safety & Environmental Compliance CPSC 16 CFR Part 1262 (magnetic flux index ≤ 50 kG²mm²); ASTM F963-23; RoHS 2.0 10-substance limits; REACH Annex XVII

Flush Stone-Polished Hard Enamel or Dimensional Recessed Soft Enamel?

Selecting between stone-polished imitation hard enamel and dimensional recessed soft enamel determines the tactile feel, scratch resistance, and retail presentation of your souvenir magnets. Both techniques utilize die-cast Zamak 3 zinc alloy bases, but their finishing stages deliver distinct commercial strengths for museum gift shops and tourism programs.

• Flush Stone-Polished Hard Enamel (Jewelry-Grade Heirloom Keepsake)

Best for: National park visitor centers, museum retail boutiques, botanical garden collections, and premium landmark souvenir lines where customers value smooth porcelain-like refinement and permanent resistance to daily scuffing.

  • Flat Coplanar Surface & Smooth Hand-Feel: After baking mineral color pastes, the entire face undergoes progressive wet stone grinding. Metal divider lines and enamel fills level into a silky, uninterrupted plane that feels cool and luxurious beneath the fingertips.
  • Scratch & Abrasion Resistance: Hard-cured resin cured at high temperatures reaches 3.5H to 4H surface hardness. It resists contact friction from kitchen keys, utensils, and cleaning cloths without scratching or losing its glossy luster over decades of display.
  • Retail Margin & Collectibility: The jewelry-grade finish commands higher retail pricing in tourist boutiques, making it the preferred standard for licensed artist series and collectible travel badge editions.

• Dimensional Recessed Soft Enamel (Tactile Relief & Vivid Contrast)

Best for: High-volume municipal tourism promotions, festival merchandise, and outdoor travel clubs seeking pronounced tactile metal ridges and high visual punch at an economical unit cost.

  • Tactile Ridge Depth: Enamel pastes settle naturally into recessed cavities below the polished metal rims, preserving a distinctive stepped, multi-level relief that fingers can trace across skylines and mountain peaks.
  • Bold Graphic Separation: Raised electroplated metal borders act as bright, shining frames around each color field, creating sharp optical contrast suited for bold graphic logos and vibrant pop-art designs.
  • Economical Unit Cost: Skipping the intensive manual stone-polishing phase shortens production cycles and reduces unit costs on high-volume runs. For sculpted non-colored architectural landmarks, explore our Explore 3D Cast Metal Fridge Magnets.
💡 Practical Craft Selection Tip: 💡 Factory Sourcing Rule of Thumb: When producing commemorative art for museum stores, national heritage destinations, or artist collaboration drops where patrons handle the magnet like fine jewelry, stone-polished hard enamel delivers superior scratch resistance and retail prestige. When producing high-volume event souvenirs with tight unit cost targets, specify recessed soft enamel.

Magnetic Retention & Surface Protective Architecture

A souvenir magnet must hold firmly to refrigerator doors without slipping or scratching appliance finishes. We engineer every element from sintered rare-earth magnetic flux to sub-flush cavity venting and cushioned backing pads to guarantee decades of reliable display.

Recessed Sintered NdFeB N35 Magnets

Heavy-duty vertical shear retention

Dual sintered neodymium rare-earth discs (11.7-12.2 kGs) press-fitted into dedicated rear sockets. Provides robust vertical shear resistance holding the heavy die-cast metal body plus multiple memos on cold-rolled steel panels without sliding.

Stone-Polished Flush Enamel Surface

Jewelry-grade coplanar refinement

Successive rotary water-stone grinding polishes the hardened enamel and metal divider lines to an identical level. The resulting surface is glassy, flat, and completely snag-free, reflecting light with mirror-like clarity.

Cross-Pattern Air Vent Channels

Zero-airlock structural bonding

Molded cross grooves in the floor of each magnet cavity allow displaced air and excess epoxy to escape cleanly during assembly, preventing trapped air pockets from pushing magnetic discs proud of the metal rim.

High-Density Anti-Scratch Velvet Pad

High-gloss appliance protection

Die-cut dense microfiber velvet or soft closed-cell EVA is adhered across the rear plate. This creates a soft protective cushion that shields glossy enameled or painted refrigerator surfaces from contact scratches.

Organic Die-Cut Perimeter Tooling

Silhouette matching landscape contours

Hardened steel stamping dies trim the perimeter along natural shoreline waves, mountain ridges, and cloud borders. Every outer contour undergoes manual cloth-wheel buffing to remove all parting lines and sharp burrs.

Sub-Flush 0.08mm Safety Inset

Zero-contact appliance clearance

Each magnet cavity is cast 0.08 mm deeper than the disc thickness. Sinking the metallic magnet marginally beneath the perimeter prevents hard magnet edges from dragging across appliances during repositioning.

Special Finishes & Compounding Visual Effects

Surface plating and specialty color effects dictate how coastal lighthouses, alpine peaks, and tropical sunsets capture ambient gallery lighting. We apply four specialized finishes sealed under baked protective clear coats.

Process / Effect Technical Formulation & Appearance Best Applications
Polished Genuine Gold Flash Multi-stage copper leveling under bright nickel, electroplated with genuine 18K/24K gold flash and sealed with baked acrylic clear coat (8-12 μm, 3H). Produces a radiant, jewelry-grade metallic rim that highlights warm landscape artwork. National park landmarks, UNESCO heritage gifts, luxury resort amenities
Polished Silver & Bright Chrome High-luster specular chrome plated over nickel and acid copper barriers. Delivers crisp, cool metallic reflection with high abrasion resistance, framing alpine peaks and icy coastal scenes. Alpine ski resorts, glacier monuments, modern architectural skylines
High-Contrast Black Nickel Electroplated dark gunmetal finish hand-buffed to a deep specular sheen. Creates dramatic dark metal lines that separate vibrant botanical greens and sunset gradients with striking visual pop. Botanical gardens, modern graphic art series, night tour merchandise
Translucent & Pearl Shimmer Enamel Optical-grade tinted resin formulations with embedded mica pearlescent flakes. Allows underlying metal textures to shimmer through ocean waves and sky gradients, simulating natural water reflections. Marine aquariums, coastal lighthouses, aurora borealis souvenirs

For complete electroplating bath standards, plating thickness certifications, and neutral salt spray data, review our Industrial Electroplating & Finishes Standard.

Presentation & Tourist Retail-Ready Packaging Solutions

Thoughtful packaging transforms a scenic collectible into an impulse purchase ready for airport boutiques, museum bookstores, and tourist gift displays.

Individual Peel-and-Seal Poly Sleeve (Included Default)
Crystal-clear heavyweight BOPP sleeve with resealable adhesive flap. Protects the stone-polished enamel face and velvet backing from transit friction while serving as an economical baseline for bulk packing.
Custom Full-Color Illustrated Backing Card (Retail Peg Upgrade)
350g rigid art paperboard printed in full-color CMYK with Euro-hook hanging slot. Displays regional history, artist bios, and retail barcodes for hanging carousel displays in tourist gift shops.
Clear Rigid Acrylic Archival Showcase (Archival Display Upgrade)
Two-piece optical acrylic showcase capsule fitted with a custom die-cut EVA foam insert. Keeps the scenic enamel magnet dust-free while functioning as an upright display frame on work desks or display shelves.
Magnetic Book-Style Rigid Gift Box (Executive Gift Presentation)
Premium rigid card box with magnetic flip-top lid, hot-stamped metallic foil lettering, and custom velour foam tray for commemorative gift sets and VIP delegation keepsakes.

主图 05

From Concept to Creation: Direct-Factory Production & Quality Assurance

1. CNC Tooling & Precision Die Engraving Tooling engineers translate your landscape illustrations and vector line artwork into matched H13 die steel blocks, carved with high-speed CNC milling cutters down to ±0.03 mm precision.
2. High-Pressure Hot-Chamber Die Casting Dense Zamak 3 zinc alloy is injected under high pressure into steel dies, capturing fine wave foam, mountain crags, and recessed magnet cavities with clean structural density.
3. Gate Trimming & Perimeter Buffing Castings undergo automated gate clipping, vibratory deburring, and multi-stage manual cloth-wheel buffing to eliminate parting lines and produce silky-smooth outer borders.
4. Multi-Layer Plating & Anti-Tarnish Sealing Parts pass through ultrasonic degreasing, copper strike, acid leveling, and bright gold electroplating, sealed with baked acrylic clear coat tested to 48h salt spray.
5. Mineral Color Dispensing & Stone Lapping Fluid enamel pastes matched to Pantone PMS standards are dispensed into recessed cells, heat-cured, and passed through rotary water-stone grinding to create a 100% flush face.
6. Magnet Press-Fit & 100% Pull Verification Technicians dispense structural epoxy into sub-flush cavities, press-fit twin N35 neodymium magnets, adhere velvet backing pads, and verify holding force against calibrated steel test plates.

主图 06

Factory Assurance: Tooling precision, enamel color consistency, and magnetic retention are certified under the personal oversight of Tooling & Quality Director Lin Jianhua (Gold Valley Dongguan Works). Our 3,000 m² manufacturing plant operates under ISO 9001:2015 quality certification and annual Sedex SMETA 4-Pillar ethical audits, with verified compliance to CPSC 16 CFR Part 1262 and ASTM F963-23 magnet standards.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or submit directly to our engineering team for rapid 2-4h factory pricing:

• Base Metallurgy: High-Pressure Die-Cast Zamak 3 Zinc Alloy (density 6.6-6.7 g/cm³)
• Surface Finish: Stone-polished imitation hard enamel (coplanar flush surface); 3.5H-4H hardness
• Dimensional Envelope: 55 mm to 80 mm × 45 mm to 65 mm (2.17″ to 3.15″ × 1.77″ to 2.56″); thickness 3.0 mm to 4.0 mm
• Magnet System: Dual recessed sintered NdFeB N35 discs (11.7-12.2 kGs); Ni-Cu-Ni triple plated; 0.08 mm sub-flush pocket
• Holding Performance: Vertical holding capacity supports ≥ 6 to 8 sheets of 80g A4 paper on cold-rolled steel panels
• Quality Benchmark: ISO 2859-1 AQL 1.0 Major / 2.5 Minor; CPSC 16 CFR Part 1262 magnet safety; ASTM B117 48h salt spray passed
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Custom Enamel Fridge Magnets: Ordering & Production FAQ

Will these heavy enamel magnets slide down refrigerator doors or fail to hold memos?

A: No. We install dual sintered NdFeB N35 rare-earth disc magnets that produce residual flux between 11.7 and 12.2 kGs. Unlike weak flexible rubber magnets that slide under their own weight, our neodymium system delivers strong vertical shear resistance. Each piece securely anchors its 50g to 75g metal body plus 6 to 8 sheets of A4 copy paper on standard cold-rolled steel refrigerator panels without slipping.

Will the hard enamel face scratch easily, or will the magnet scratch high-gloss appliance finishes?

A: Both surfaces are engineered for scratch resistance. The stone-polished imitation hard enamel face reaches 3.5H to 4H hardness, resisting contact scuffs from keys or kitchen utensils. On the reverse, magnet pockets are cast 0.08 mm deeper than disc thickness to keep metal magnets sub-flush, and we adhere full-coverage die-cut microfiber velvet pads across the base to shield glossy refrigerator paintwork.

Can these magnets attach to all styles of modern refrigerators?

A: Sintered neodymium magnets adhere firmly to traditional cold-rolled steel (SPCC) refrigerator doors and painted steel side panels. However, austenitic stainless steel (such as SUS304) and modern glass-faced door panels are non-magnetic. For clients featuring non-magnetic glass appliances, we supply auxiliary self-adhesive steel docking plates that adhere to glass surfaces to receive the magnetic souvenir.

What artwork formats do you require, and how quickly can we review production drawings?

A: We accept vector artwork in .AI, .EPS, .PDF, or high-resolution layered .PSD formats. If you only have scenic photographs, landscape sketches, or tourist postcards, our engineering department will extract dividing lines and construct a production-ready color layout proof within 2 to 4 working hours at no charge.

What are your minimum order quantities, sample lead times, and mass manufacturing schedules?

A: Pilot production runs start from 100 pieces per design, allowing national parks, museum stores, and independent illustrators to test retail response. Volume cost breaks scale significantly at 300, 500, and 1,000+ units where tooling costs amortize. Tooling and physical evaluation samples require 5 to 7 working days, while mass manufacturing takes 12 to 18 working days.

What factory credentials and product safety standards govern your magnet manufacturing?

A: Gold Valley operates an audited 3,000 m² facility in Dongguan under ISO 9001:2015 quality certification and annual Sedex SMETA 4-Pillar audits. For licensed souvenir programs, we maintain verified Disney FAMA (FAC-086164) and NBCUniversal (L-8360-DT-004) authorisations. The product complies with CPSC 16 CFR Part 1262 and ASTM F963-23 magnet retention standards (pull-out force ≥ 50 N), while our electroplated finishes conform to RoHS 2.0 and REACH Annex XVII Entry 27 nickel release thresholds (< 0.5 μg/cm²/week).
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email