Custom Metal Badges & Pins | Premium OEM/ODM Manufacturer & Factory Direct

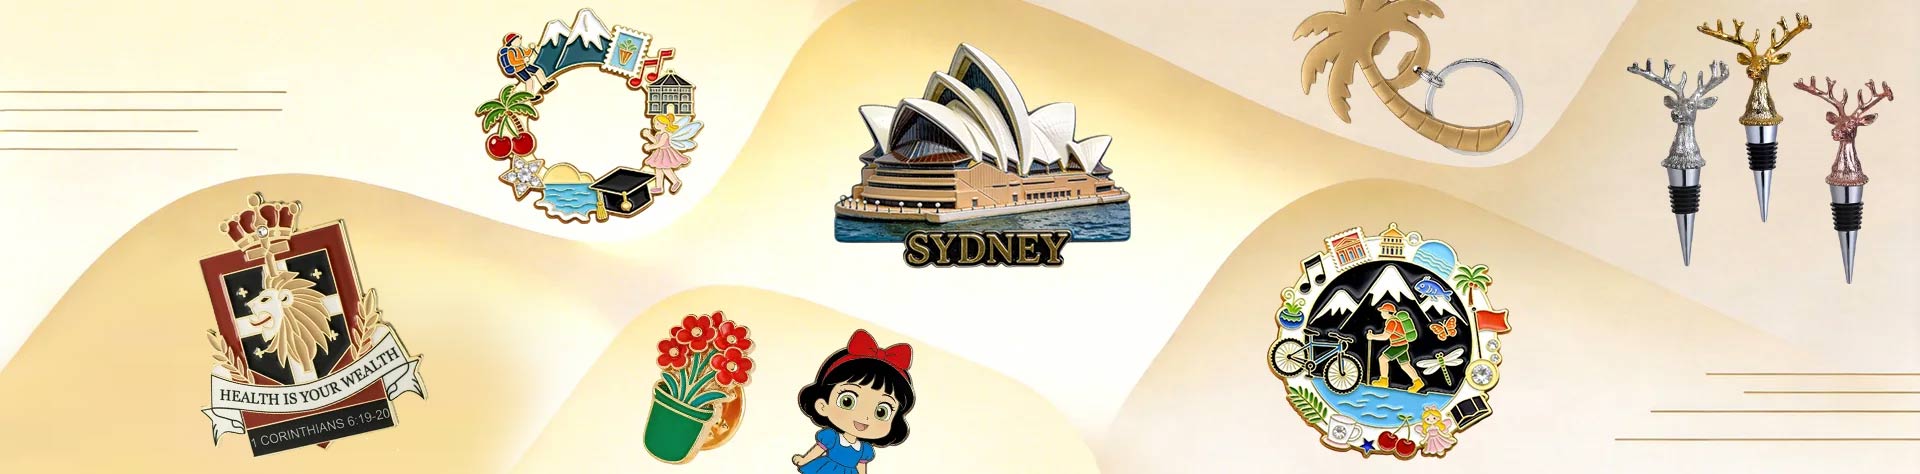
product banner
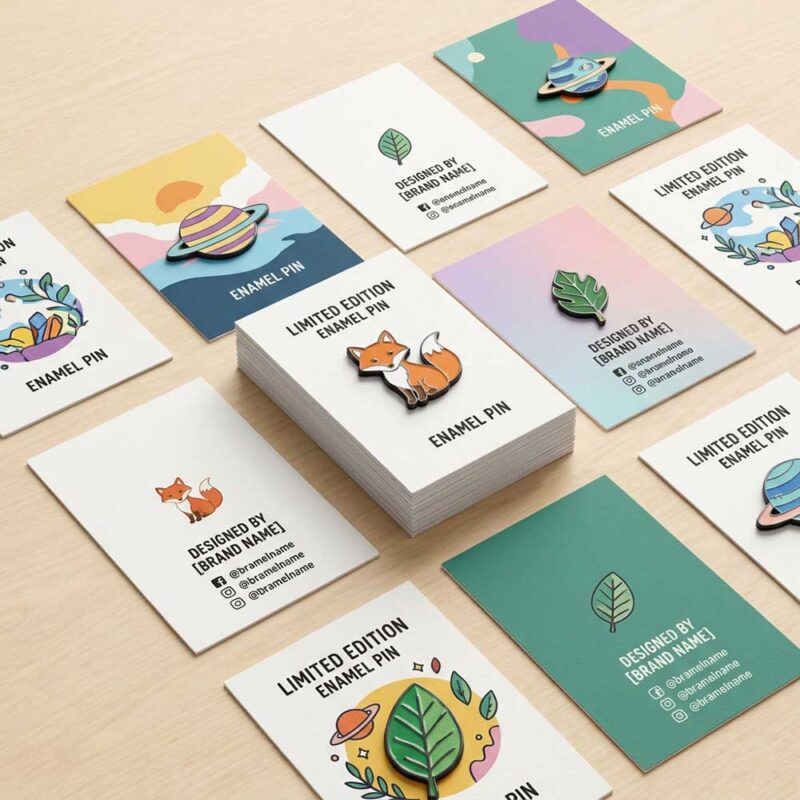
enamel fox pin
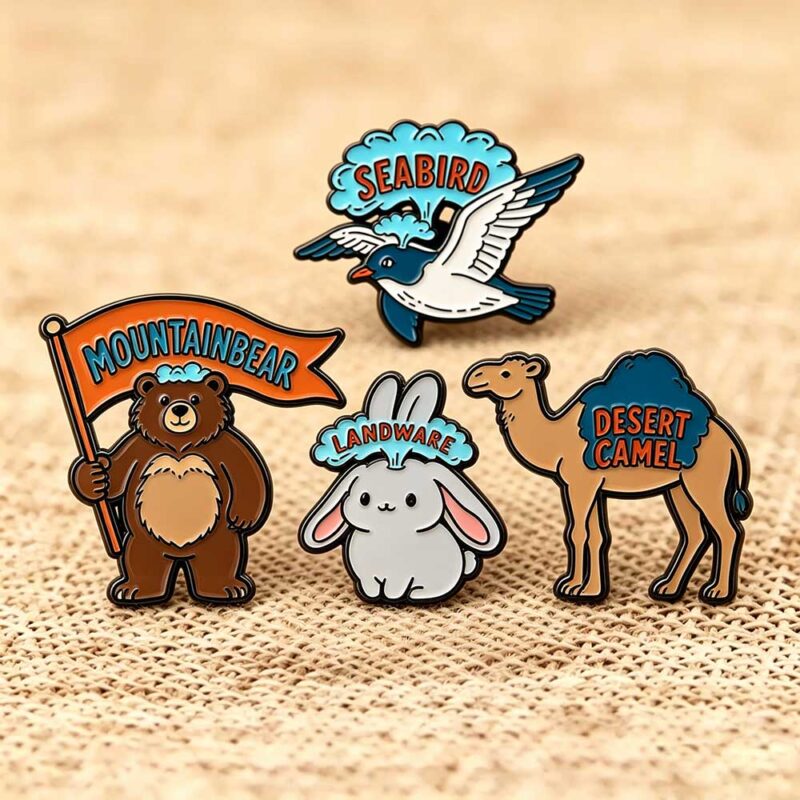
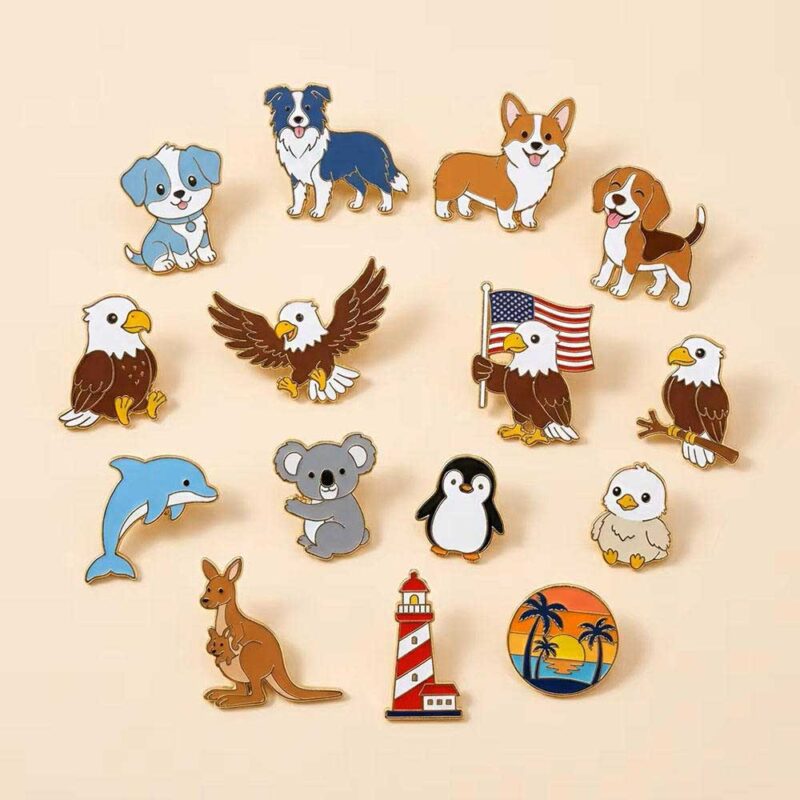
enamel animal pin
custom hard enamel pins
custom hard enamel lapel pins
custom hard enamel pins
enamel fox pin
enamel animal pin
custom hard enamel pins
custom hard enamel lapel pins
custom hard enamel pins
Custom Metal Badges & Pins | Premium OEM/ODM Manufacturer & Factory Direct
Description :
  • Your artwork keeps its edges. The metal lines that separate one color from the next are cut 0.25 mm (0.010″) wide or wider, and every fill is mixed to Pantone PMS Solid Coated. Adjacent colors stay where you put them instead of creeping into each other.
  • Solid metallurgy, durable plating. Engineered from dense H65 brass (8.4-8.5 g/cm³) or Zamak 3 zinc alloy rather than lightweight ferrous stampings. The tactile relief feels substantial in hand, while multi-layer barrier plating and a baked acrylic protective clear coat resist sweat corrosion and everyday handling wear.
  • Rapid engineering proofs, zero-cost mold archive. A 3D vector proof reaches you within 2 to 4 working hours, physical samples in 3 to 7 working days, and your tooling stays preserved in our archive for 2 years with zero reorder mold fees.
Base Material & Density Stamped H65 Brass (8.4-8.5 g/cm³) or Die-Cast Zamak 3 (6.6-6.7 g/cm³)
Standard Thickness 1.2-2.0 mm (0.047″-0.079″) stamped / 2.5-4.0 mm (0.098″-0.157″) die-cast
Minimum Order Pilot batches start from 50-100 pcs; price breaks scale at 300, 500, and 1,000+ units. Send artwork for an itemized quote.
Production Lead Time 3D proof: 2-4 working hours | Sample: 3-7 working days | Mass run: 12-18 working days
Tooling Retention 2 years free archive retention (renewed on reorders); $0.00 tooling fee on reorders

Send your artwork (.AI, .EPS, .PDF or .SVG) for an itemized factory quotation and a complimentary 3D production proof within 2 to 4 working hours.
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Material & Density Stamped H65 Brass (8.4-8.5 g/cm³) or Die-Cast Zamak 3 Zinc Alloy (6.6-6.7 g/cm³) Explore the Lapel Pin Series
Dimensional Tolerances Steel die machining precision: ±0.03 mm (±0.0012″); finished piece profile tolerance: ±0.10 mm (after edge buffing and plating)
Standard Thickness 1.2-2.0 mm (0.047″-0.079″) stamped brass / 2.5-4.0 mm (0.098″-0.157″) die-cast zinc
Color Channel Geometry Raised metal line ≥ 0.25 mm (0.010″); fill channel depth ≥ 0.35 mm (0.014″); minimum legible type 5.0 pt bold sans-serif
Plating & Surface Finishes Shiny gold, shiny nickel, black nickel, antique bronze, antique silver, rose gold, two-tone; multi-layer barrier plating under a baked acrylic protective clear coat
Corrosion & Adhesion Test 48-Hour Neutral Salt Spray (NSS) to ASTM B117 with no blistering or green rust; cross-hatch adhesion to ASTM D3359 Grade 5B
Attachment Pull Test Pin post solder joint shear ≥ 5.0 kgf (11 lbf); butterfly clutch rated for 500+ insertions without losing grip
Production Turnaround Digital 3D Vector Proof: 2-4 Working Hours | Physical Sample: 3-7 Working Days | Mass Run: 12-18 Working Days
Compliance Certifications ISO 9001:2015 · Sedex SMETA 4-Pillar · Disney FAMA (FAC-086164) · NBCUniversal (L-8360-DT-004) · EN 1811 nickel release · RoHS 2.0

Soft Enamel or Hard Enamel? Choosing the Right Surface

Both processes start from the same stamped or die-cast metal body. The difference is what happens after the color goes in, and that single step decides how the pin feels in the hand, how fine the artwork can go, and what it costs at volume.

• Soft Enamel (Recessed Color)

Best for: Brand merch, club and society pins, event giveaways, artist designs with bold flat color blocks.

  • Tactile Heft & Feel: Color sits below the metal, so the surface reads as a shallow relief you can trace with a thumb. On stamped H65 brass at 8.5 g/cm³ the piece carries a firm, solid weight for its size.
  • Visual Detail & Sharpness: Lines hold at 0.25 mm (0.010″) and colors stay in their own channels. Best suited to artwork with clear separations rather than photographic gradients.
  • Commercial Balance: One fewer polishing stage than hard enamel, which is why it is the volume choice for 500 to 50,000 piece runs.

• Synthetic Hard Enamel (Flush Surface)

Best for: Corporate crests, long-service awards, university and regimental badges, any design where fine text must stay legible.

  • Tactile Heft & Feel: Watering-stone polishing brings the color down level with the metal, so the face is smooth and cool. Hardness lands at 3H to 4H.
  • Visual Detail & Sharpness: Because the surface is one plane, light does not catch on every line. Fine lettering and geometric marks read cleanly, and raised lines are built at 0.35 mm (0.014″) to survive the grinding stage.
  • Commercial Balance: The extra stone-polishing stage raises unit cost, so it pays off on prestige programs rather than mass giveaways. For formal crests requiring a completely flat, stone-polished surface, review our Custom Hard Enamel Pins Specification.
💡 Practical Craft Selection Tip: If your artwork has more than two colors meeting in a tight corner, stay with soft enamel and give each line 0.25 mm of metal. Hard enamel only wins when the design relies on small type or a formal, flat crest — and it costs more to get there.

Backing Hardware: How the Pin Actually Stays On

Most complaints about pins are not about the front. They are about a pin that droops sideways on a lapel, or a clutch that stops gripping after a few months. The attachment layout is a design decision, and it changes with the size and weight of the piece.

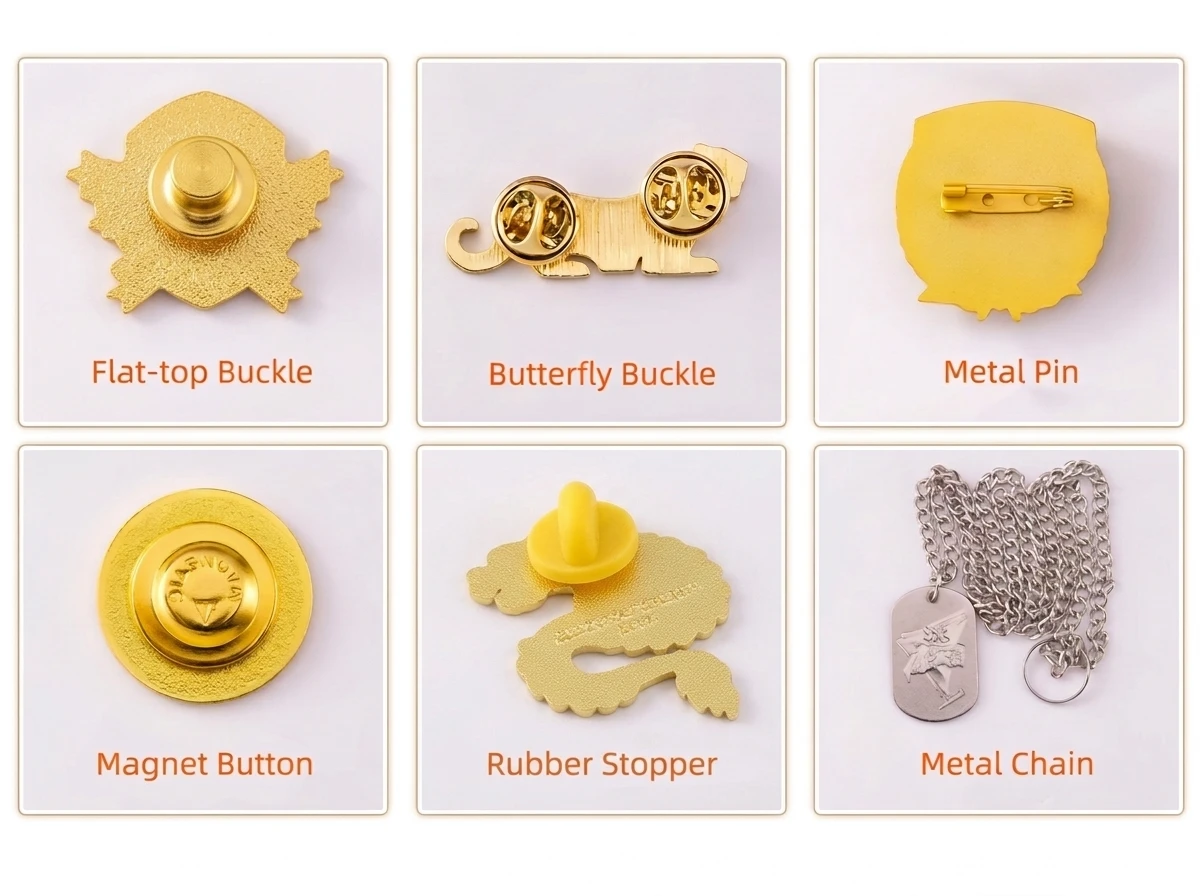
Spur Pin + Butterfly Clutch

Standard for pins up to 25 mm

Annealed brass post at 1.1-1.2 mm diameter in 8, 10 or 12 mm lengths, mated to a stamped brass clutch with a phosphor bronze spring inside. Shear strength at the solder joint holds at 5.0 kgf (11 lbf) or better, and the clutch is rated for 500+ insertions.

Deluxe Flat-Head Clutch

Premium lapel and collector pins

CNC-turned brass body with a ball-bearing spring lock. Axial pull-out resistance reaches 10.0 kgf (22 lbf), and the lock only releases when you pull the rear cap outward, so it will not work loose against a jacket or bag strap.

Double-Pin Anti-Spin Layout

Any pin wider than 30 mm

A single post lets a wide or top-heavy pin rotate on the fabric. Two posts set at least 15 mm apart lock the angle, so the design stays upright through a full day of wear. We specify this automatically on asymmetric shapes.

Rubber Clutch

Skin-adjacent and kids’ apparel

Molded PVC or silicone cap with no exposed metal edge. Friction hold runs 2.0-3.0 kgf and the material stays flexible from -10°C to 60°C. A common pick for school and youth program pins.

Safety Brooch Pin

Pieces over 40 mm

A stainless bar with a 360° revolving safety catch rated at 4.0 kgf. Deburred pivot edges prevent accidental unfastening or thread pulling on heavier jackets and overcoats.

Magnetic Backing (No Hole)

Cashmere, silk and fine suiting

Two sintered NdFeB N35 discs pulling against each other, holding 800 g or more vertically. Nothing pierces the fabric, so a wool blazer or silk shirt is not left with a permanent hole. Not for wearers with a pacemaker.

💡 Need help choosing the right backing for your fabric or event?
Compare retention benchmarks, tactile feel, and garment safety limits in our comprehensive engineering guide: Pin Attachment Hardware: 6 Lapel Pin Backings Compared →

pin attachment hardware

Special Finishes & Advanced Compounding Effects

The four effects below separate a pin that looks like every other giveaway from one people keep on the jacket. Each is applied on top of the standard plating stack, not instead of it.

Process / Effect Technical Formulation & Appearance Best Applications
Translucent Enamel over Guilloché A fine concentric wave pattern is cut into the metal before a semi-transparent color paste is laid over it. Light passes through the color, bounces off the engraving, and returns with a depth that an opaque fill cannot produce. Jewellery brands, art print editions, premium coin-adjacent programs
Glitter & Pearlescent Paste Heat-stable fine glitter or mica pearl powder is blended into the color paste before dispensing, so the effect runs through the fill rather than sitting on the surface. It survives the curing oven without dulling. Pop culture and anime merch, theme park souvenirs, wedding favors
Long-Afterglow Phosphor Strontium aluminate pigment is mixed into selected color channels. Fifteen minutes of light exposure returns several hours of glow, and because it is a pigment rather than a coating, it does not flake off. Night runs, Halloween and horror properties, tactical and unit insignia
Two-Tone Plating A high-viscosity masking lacquer is hand-applied to hold part of the face while the second metal is plated on. Masking placement is held to ±0.3 mm, which keeps the boundary between gold and black nickel clean at the edge. Corporate anniversary marks, association crests, two-color brand identities

For plating layer thickness and masking tolerances, review our Industrial Electroplating & Finishes Standard.

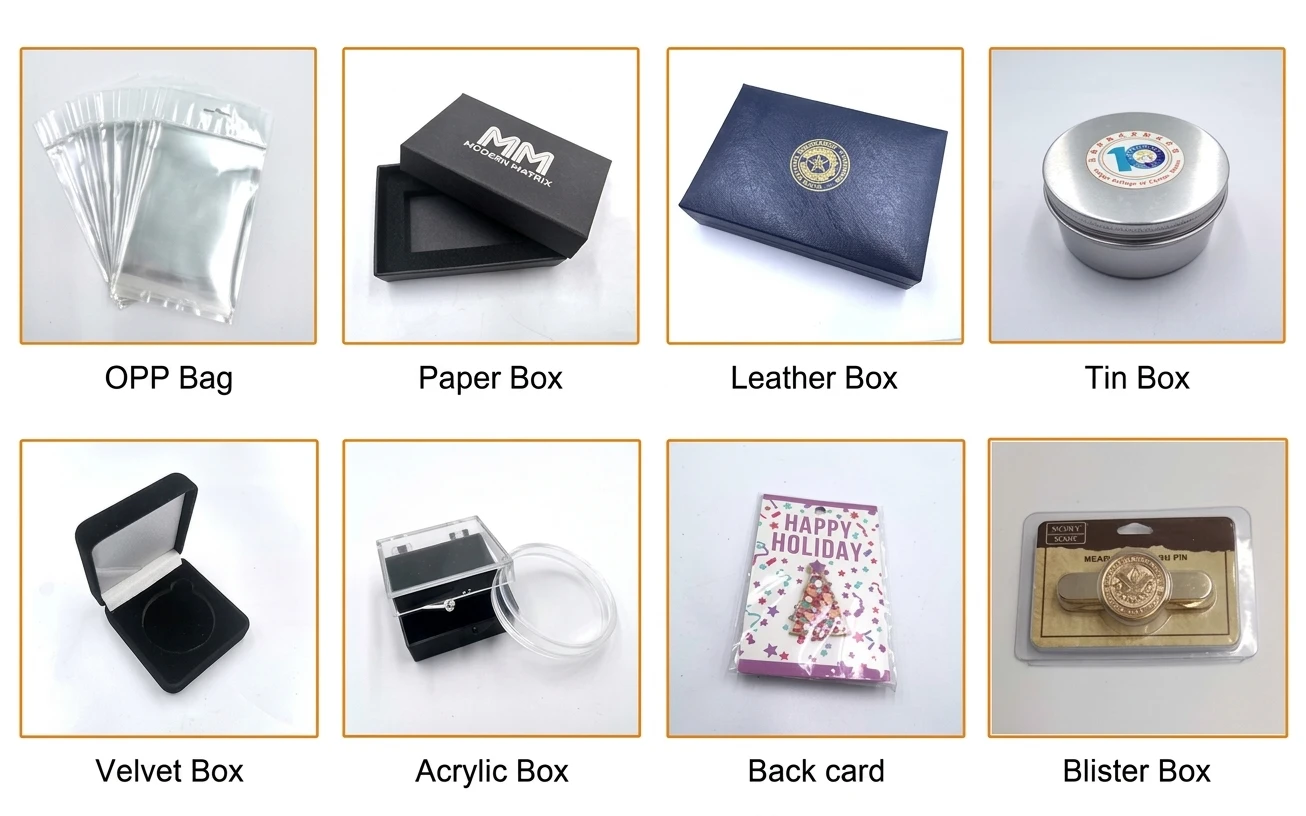
Retail Presentation & Archival Packaging Solutions

Packaging decides whether the pin arrives as a loose metal part or as something the recipient can hand over as a gift. Four levels, from bulk freight to retail shelf.

Individual Self-Sealing Polybag (Included Default)
The zero-cost baseline. Each pin is bagged separately so plated faces do not rub against each other in transit, which keeps freight weight and landed cost down on large runs.
Custom Printed Backing Card (Retail Peg Upgrade)
350 g art card printed in full color with a Euro-slot punch, so the pin hangs on a retail peg without extra hardware. Foil stamping is available for premium lines.
Optical Acrylic Capsule (Archival Display Upgrade)
A snap-fit clear case with a die-cut EVA gasket that holds the pin still. Nothing rattles in transit, and the pin stays visible without being handled.
Velvet Hinged Gift Box (Executive Presentation)
Hinged board box wrapped in velvet or textured paper, with a laser-cut EVA insert shaped to your pin. Standard for awards, ceremonial gifts and collector editions.
Custom enamel pin packaging with printed backing card and velvet hinged gift box

From Concept to Creation: Direct-Factory Production & Quality Assurance

1. 2D/3D Precision Tooling Your vector artwork is laid out 1:1 and cut into an H13 tool steel die using high-speed CNC engraving and sinker EDM, while perimeter blanking tools are wire-EDM cut. Every separation line is checked against the 0.25 mm floor before cutting starts to prevent color bridging.
2. High-Density Forming Stamped brass is coined on high-tonnage precision coining presses to force metal into every sharp recess; 3D zinc profiles are injected in hot-chamber die-casting machines at 410°C with 1.5° to 3.0° draft angles.
3. Hand Mirror Buffing & Deburring Polishing technicians run each piece across multi-stage cloth wheels to remove parting lines and soften the outer edge. That last step is what keeps a pin from snagging a silk blouse or a wool blazer.
4. Multi-Layer Plating & Anti-Tarnish Sealing Ultrasonic degreasing, alkaline copper strike, acid copper leveling, bright nickel, then the finish metal. A baked acrylic protective clear coat seals the whole face to protect against sweat corrosion and tarnishing.
5. Precision Enamel Color Dispensing Each color channel is filled with a pneumatically dispensed paste mixed to your Pantone reference, then cured in the oven. Filling color by color is what keeps a red and a green from meeting in the middle and turning brown.
6. 100% Piece-by-Piece Inspection Every finished pin is checked by hand under magnifying lamps for plating pinholes, color creep and burrs, then batch-tested for attachment strength. Defective pieces are reworked or remade before packing.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or submit directly to our Direct Engineering Desk for rapid 2-4h factory pricing:

• Base Metallurgy: Stamped H65 Brass (8.4-8.5 g/cm³) or Die-Cast Zamak 3 Zinc Alloy (6.6-6.7 g/cm³)
• Critical Geometry: Raised metal line ≥ 0.25 mm (0.010″); fill channel depth ≥ 0.35 mm (0.014″); body thickness 1.2-2.0 mm (0.047″-0.079″) stamped or 2.5-4.0 mm (0.098″-0.157″) die-cast
• Tooling & Tolerances: Steel die CNC machining: ±0.03 mm (±0.0012″); finished part profile tolerance: ±0.10 mm; 1.5°-3.0° draft angle; minimum legible type 5.0 pt bold
• Plating & Corrosion: Multi-layer barrier plating with baked protective clear coat; 48-hour ASTM B117 neutral salt spray passed
• Attachment: Pin post shear ≥ 5.0 kgf (11 lbf); double-post layout mandatory above 30 mm width
• Quality Benchmark: ASTM D3359 Grade 5B adhesion; ISO 2859-1 AQL 1.5 Major / 4.0 Minor; Delta E ≤ 1.5 under D65
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Custom Soft Enamel Pins: Ordering & Production FAQ

What is the difference between soft enamel and hard enamel pins?

A: Soft enamel leaves the metal lines raised above the color, so the surface has a tactile contour and the unit cost stays lower. Hard enamel is ground flat with the metal until the face is one smooth plane, which suits formal crests and fine lettering. We produce both in the same Dongguan plant, so you can compare physical samples before committing.

What is the minimum order quantity for custom soft enamel pins?

A: Pilot evaluation batches start from 50 to 100 pieces (with one-time mold setup). Unit economics become significantly advantageous at 300, 500, and 1,000+ units where fixed tooling cost is fully amortized. Several designs can travel in one shipment. Send your artwork for an itemized quotation.

How thin can the raised metal lines be before colors bleed together?

A: We hold raised lines at 0.25 mm (0.010″) or wider and cut fill channels at least 0.35 mm (0.014″) deep. Below roughly 0.15 mm the electroplating builds up across the gap and bridges it shut, so two colors end up touching. If your design has finer detail than that, we will flag it on the artwork proof before tooling starts rather than after.

Can you match our exact brand colors, and what file formats do you need?

A: We mix enamel paste against the Pantone Formula Guide Solid Coated standard and verify under a D65 daylight booth, holding spectrophotometer Delta E within 1.5. Send vector artwork in .AI, .EPS, .PDF or .SVG. If all you have is a raster sketch or a photo of a physical sample, our engineering team will build the 3D production proof for you within 2 to 4 working hours at no charge. Submit files through our Direct Engineering RFQ Desk.

Can you hit a deadline for a trade show or a fixed event date?

A: Standard sampling takes 3 to 7 working days and mass production 12 to 18 working days. For dated events we run a dedicated rush tooling shift that can turn physical prototypes around in 48 to 72 hours. Express air freight reaches most destinations in 3 to 5 business days.

Which factory credentials apply to this product?

A: Our 3,000 m² Dongguan facility operates under ISO 9001:2015 quality certification and a Sedex SMETA 4-Pillar ethical audit. For licensed metal programs we hold Disney FAMA authorization (FAC-086164) and NBCUniversal approval (L-8360-DT-004). Skin-contact components are tested for nickel release under EN 1811 and the plating stack meets RoHS 2.0 limits. These are facility-level credentials; where a program needs product-level test reports, we arrange third-party testing per order.
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email