Custom Military Challenge Coins

product banner
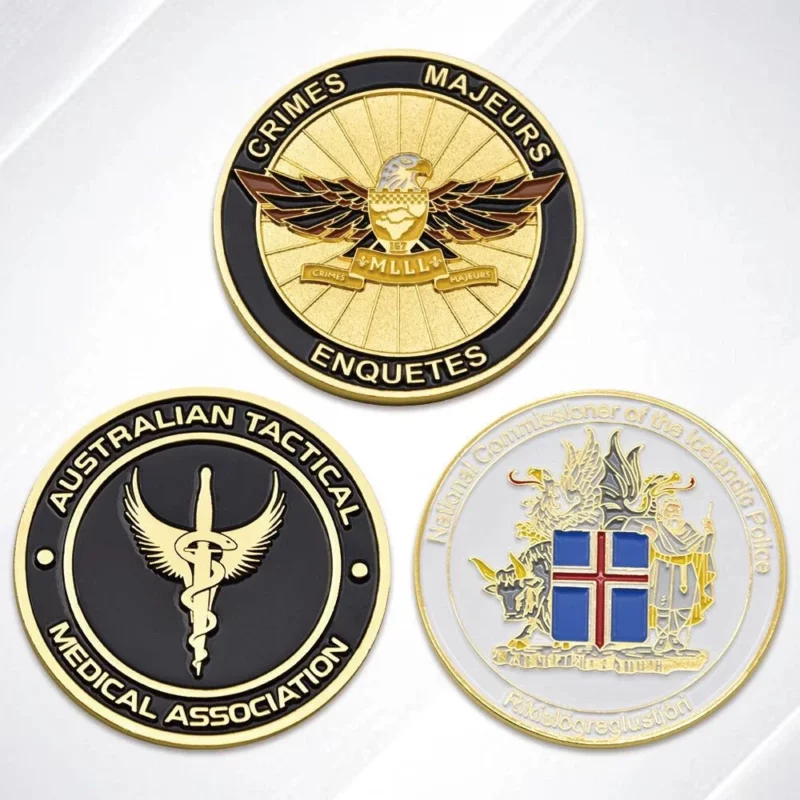
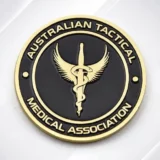
crimes majeurs australian tactical iceland round white sku grid processed
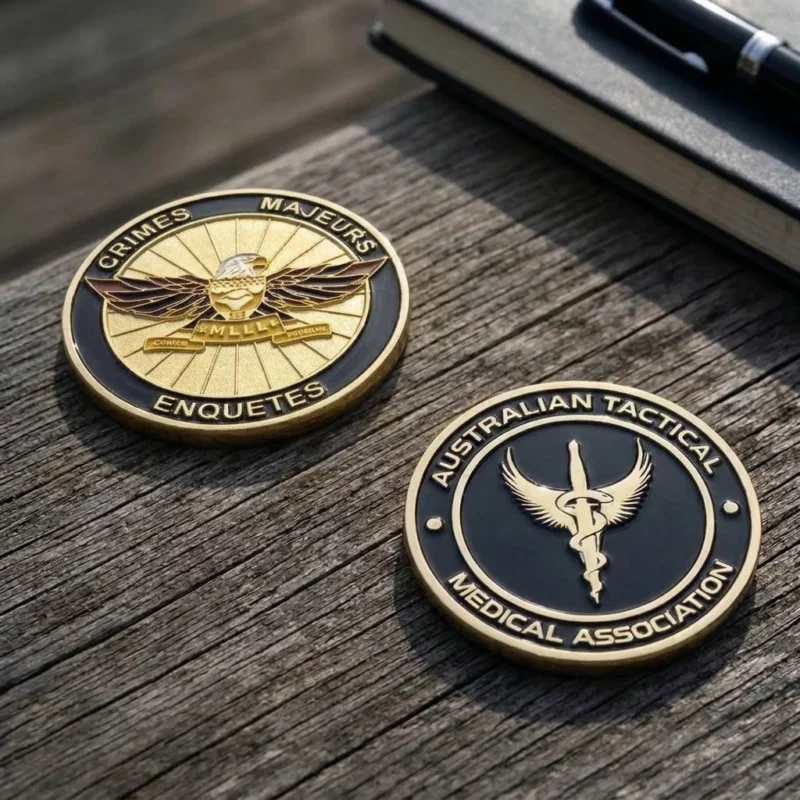
crimes majeurs australian tactical pair round scene processed
crimes majeurs plain round white processed
australian tactical plain round white processed
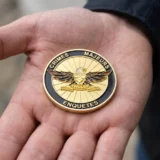
Man holding custom challenge coin 0d18bc5a processed
crimes majeurs australian tactical iceland round white sku grid processed
crimes majeurs australian tactical pair round scene processed
crimes majeurs plain round white processed
australian tactical plain round white processed
Man holding custom challenge coin 0d18bc5a processed
Custom Military Challenge Coins
Description :
  • Uncompromising heft and sovereign metallic chime. Minted from solid H65 brass blanks (density 8.4-8.5 g/cm³) under high-tonnage hydraulic coining presses, our military challenge coins deliver the authoritative hand weight and resonant acoustic chime demanded by armed forces traditions. Each 1.75″ to 2.0″ medallion lands in the palm with a solid 50 to 75 g heft that lightweight cast pewter cannot match.
  • Precision tactical heraldry and authentic metal textures. Engineered with high-speed CNC-machined tool steel dies that capture intricate unit crests, sunburst radial guilloché backgrounds, fine checkered shield fields, and razor-sharp typographic mottos. Hand-filled with durable opaque enamel that cures flush or slightly recessed, preserving the cold, tactile feel of bare metal without cloudy epoxy coatings.
  • Battle-ready corrosion barrier and archival presentation. Finished with precision perimeter reeding or diamond-cut edge treatments, then sealed beneath an oven-cured baked acrylic protective clear coat tested to 48 hours of ASTM B117 salt spray. Available with sequential 4-axis laser serial numbers, housed in airtight snap-fit optical capsules, with tooling preserved for 2 years of free die retention on reorders.
Base Metallurgy & Density High-Density Stamped H65 Brass (8.4-8.5 g/cm³) or Die-Cast Zamak 3 (6.6-6.7 g/cm³)
Standard Diameter & Profile 44 mm, 50 mm, 57 mm (1.75″, 2.00″, 2.25″); thickness 3.5-4.5 mm (0.138″-0.177″)
Surface Contrast & Enamel Polished 24K real gold, tactical matte black, or hand-relieved antique bronze; zero epoxy dome
Edge Treatment Standard Precision reeded / serrated coin edge (0.6 mm pitch); optional CNC diamond cut or laser serializing
Serialization & Anti-Counterfeit Optional 360° rotational laser rim engraving (e.g., UNIT-001/300) for limited edition runs
Minimum Order Quantity Pilot batches from 50-100 pcs; volume price breaks at 300, 500, and 1,000+ units
Production Turnaround 3D proof: 2-4 working hours | Physical sample: 3-7 working days | Mass run: 12-18 working days
Tooling Retention Policy 2 years free archive retention (renewed automatically on reorders); $0.00 tooling fee on reorders
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Material & Density Stamped High-Tensile H65 Brass (8.4-8.5 g/cm³) or Hot-Chamber Die-Cast Zamak 3 (6.6-6.7 g/cm³) Explore Custom Challenge Coins Collection
Coining Precision & Tolerances CNC tool steel die cavity precision: ±0.03 mm (±0.0012″); finished coin outer diameter tolerance: ±0.08 mm; thickness tolerance: ±0.10 mm
Standard Dimensions & Weight Diameter: 44 mm, 50 mm, 57 mm (1.75″, 2.00″, 2.25″); body thickness: 3.5-4.5 mm (0.138″-0.177″); solid weight: 50-80 g per piece
Heraldic Detailing & Sunburst Optics Micro-radial sunburst guilloché lines (0.12 mm width), fine checkered shield patterns, and crisp raised serif/sans-serif typography down to 4.5 pt
Edge Treatments & Perimeter Styles Classic reeded / milled edge (0.6 mm pitch); inner beaded border; CNC diamond cut (rope, wave, cross-cut); 4-axis laser serial numbering
Electroplating & Surface Barrier Multi-stage copper and bright nickel barrier (≥ 8-10 μm) with 24K real gold flash, tactical black nickel, or antique bronze; baked acrylic clear coat (3H hardness)
Enamel Chemistry & Dome Policy Thermosetting synthetic opaque enamel; 100% bare metal and enamel tactile finish; strictly zero epoxy dome to prevent yellowing and scratching
Environmental & Corrosion Testing 48-Hour Neutral Salt Spray (NSS) to ASTM B117 with zero blistering or green corrosion; cross-hatch adhesion to ASTM D3359 Grade 5B (0% flaking)
Individual Archival Packaging Snap-fit optical clear acrylic capsule (Air-Tite style) with zero-rattle precision fit; optional micro acrylic display easel or luxury velvet presentation box
Production & Sampling Timeline Digital 3D Vector Proof: 2-4 Working Hours | Physical Pre-Production Sample: 3-7 Working Days | Mass Production: 12-18 Working Days
Factory Compliance & Audits ISO 9001:2015 · Sedex SMETA 4-Pillar · Disney FAMA (FAC-086164) · NBCUniversal (L-8360-DT-004) · EN 1811 nickel release · RoHS 2.0

Stamped H65 Brass vs Die-Cast Zamak 3: Selecting Your Unit Coin Architecture

Military and law enforcement challenge coins require uncompromising material integrity. We manufacture both stamped brass and die-cast zinc alloy architectures in our Dongguan facility, allowing commanders and coordinators to match physical specifications with mission requirements.

• Stamped H65 Brass (Hydraulic Coining)

Best for: Traditional circular military unit coins, sovereign command honors, deployment milestones, and medallions requiring authoritative heft and acoustic resonance.

  • Tactile Heft & Acoustic Chime: Coined from solid H65 brass blanks under 500-ton to 1000-ton hydraulic presses, brass achieves an authentic 8.4-8.5 g/cm³ density. Striking the coin produces a clear, sustained metallic ring that serves as a hallmark of traditional military coin-check ceremonies.
  • Surface Density & Edge Crispness: High hydraulic pressure compresses the brass blank, eliminating surface porosity and producing razor-sharp lettering, flat mirror planes, and distinct radial sunburst patterns that endure decades of handling.
  • Commercial Balance: The standard baseline for circular military and naval coins. Tooling costs are fully amortized across runs of 300 pieces or more, providing lifetime heirloom value for service personnel.

• Die-Cast Zamak 3 (Intricate 3D & Pierced Cutouts)

Best for: Complex multi-tier unit crests, sculptural eagle emblems, irregular shield contours, and coins featuring interior pierced cutout apertures.

  • Tactile Heft & Acoustic Chime: Molten Zamak 3 injected at 410°C fills intricate die geometry with fluid precision. At 6.6-6.7 g/cm³ density, a 4.0 mm thick coin remains pleasantly substantial in hand, though its acoustic feedback is shorter and more dampened than brass.
  • Surface Density & Edge Crispness: Enables true 3D anatomical sculpture, steep draft angles, and pierced open-hole apertures through the coin body that mechanical stamping cannot execute. When your design requires high 3D sculptural reliefs, review our Custom 3D Challenge Coins specification.
  • Commercial Balance: Highly cost-effective for non-circular shield outlines and multi-level sculpted emblems, eliminating secondary stamping operations and reducing tooling setup overhead on pilot batches.
💡 Practical Craft Selection Tip: For traditional military command coins, circular deployment tokens, and pieces where hand heft and acoustic chime are paramount, select stamped H65 brass. When your unit insignia features irregular shield contours, pierced cutouts, or extreme 3D sculptural elevations, select die-cast Zamak 3.

Coin Rim & Edge Engineering: Six Precision Tactical Border Treatments

The perimeter edge of a military challenge coin defines its tactile grip and prevents palm slippage during formal coin checks. We offer six dedicated mechanical rim styles engineered on specialized secondary tooling.

Precision Reeded / Serrated Edge

Classic armed forces issue serration

Continuous vertical serrations cut at a uniform 0.6 mm pitch around the perimeter rim. Delivers crisp tactile friction, prevents slippage, and mirrors sovereign currency minting standards.

Stepped Tactical Rim with Recessed Rivets

Armored units, SWAT, and tactical teams

A raised cylindrical outer rim punctuated by precision-milled circular rivet indentations. Conveys armored vehicle plating, tactical field gear, and heavy mechanical durability.

CNC Diamond-Cut Rope & Wave Edge

Naval command and coast guard awards

Diamond-tipped cutters carve angled, light-reflecting wave facets directly into the metal rim. Rotates under light to create a radiant, beveled jewelry border framing central naval crests.

Cross-Cut / Swirl Diamond Serration

Police departments and special operations

Dual-axis intersecting diagonal cuts produce a knurled diamond texture around the coin edge. Offers maximum grip in gloves or wet field environments while framing unit mottos cleanly.

Flat Rim with Rotational Laser Serializing

Limited edition roster coins and serial numbers

The outer 3.5 mm to 4.5 mm cylindrical wall is polished completely flat and marked via 4-axis rotational fiber laser. Encodes permanent unit numbers (e.g., SQD-042/100) around the perimeter.

Inner Beaded Rim & Concentric Grooves

Municipal police commissions and federal bureaus

A polished outer retaining rim enclosing a concentric bead chain ring. Frames high-relief heraldic eagles, municipal crests, and state seals with timeless institutional dignity.

Special Electroplated Finishes & Contrast Techniques

Military challenge coins require surface treatments that honor heritage while resisting wear from everyday carry. We deposit industrial-grade electroplated barrier layers sealed with baked protective clear coats.

Process / Effect Technical Formulation & Appearance Best Applications
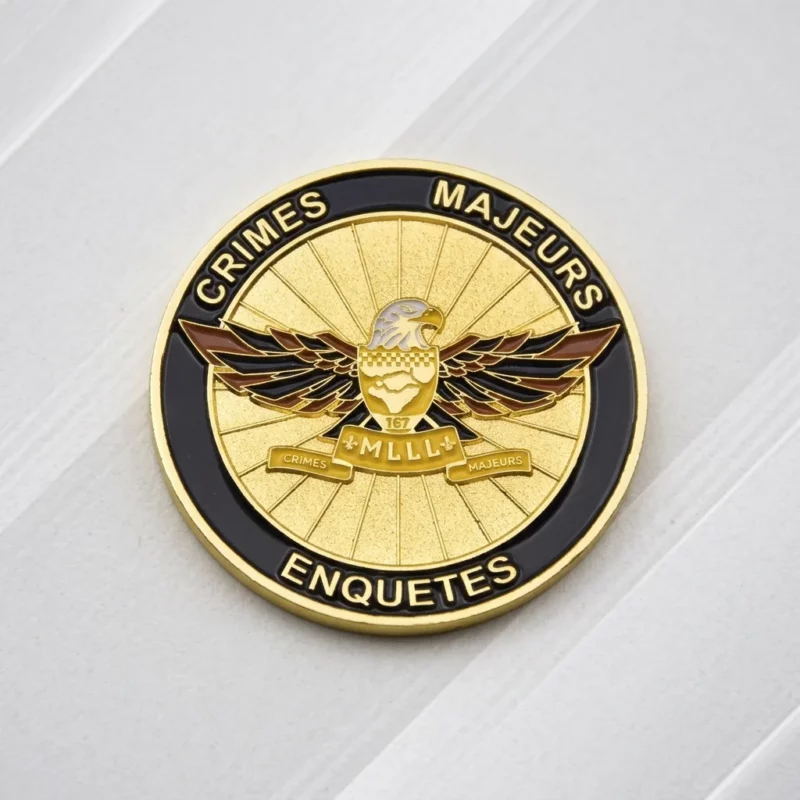
Polished 24K Gold & Matte Black Enamel High-purity 24K gold electroplated over bright nickel, paired with deep matte black enamel fills. Creates striking tactical contrast between specular golden emblems and light-absorbing fields. Tactical medical associations, executive leadership coins, special task forces
Antique Bronze & Hand-Relieved Patina Solid brass or alloy darkened in chemical sulfide baths and hand-buffed across soft sisal wheels. Crevices retain deep vintage charcoal shadows while raised surfaces expose warm brass highlights. Veterans associations, historical infantry regiments, retirement ceremonies
Two-Tone 24K Gold and Bright Nickel Plating Selective masking lacquer seals background areas while alternating plating baths deposit gold over a mirror-polished nickel or silver base, holding boundary alignment within ±0.3 mm. Joint-service command commands, multi-agency task forces, commemorative milestones
Tactical Matte Black Nickel / Gunmetal Dark charcoal electroplated barrier layer providing a stealth, subdued aesthetic that resists reflective glare in tactical environments, sealed with baked protective lacquer. Night operations teams, reconnaissance units, law enforcement SWAT details

For complete specifications on plating layer thicknesses, salt spray ratings, and barrier metallurgy, review our Industrial Electroplating & Finishes Standard.

Retail Presentation & Archival Packaging Solutions

Proper presentation packaging honors the service of recipients and protects electroplated surfaces from fingerprint oils and atmospheric oxidation.

Heavyweight OPP Envelope (Included Default)The zero-cost factory baseline. Crystal-clear archival polypropylene envelope heat-sealed to protect against dust, surface contact, and friction during bulk transit. Snap-Fit Optical Acrylic Capsule (Archival Display Upgrade)High-clarity polystyrene capsule with an engineered snap-fit rim. Secures the coin firmly with zero internal rattle, permitting 360-degree viewing without fingerprint contact. Micro Acrylic Display Easel Stand (Curated Collector Upgrade)Transparent mini triangular easel stand designed to hold 44 mm to 57 mm challenge coins upright on duty desks, barracks shelves, or commemorative trophy display cases. Hinged Velvet Presentation Box (Executive Gift Presentation)Heavy-gauge steel clamshell lined in royal blue, midnight navy, or black velvet with white silk satin lid lining and custom die-cut EVA recess molded to the encapsulated coin.
coins packaging method

coins packaging method

From Concept to Creation: Direct-Factory Production & Quality Assurance

1. Unit Crest Vector Engineering & Die Engraving Customer unit patches, heraldic crests, and mottos are converted into precision CAD toolpaths. Hardened Cr12MoV tool steel dies are machined via high-speed CNC milling and precision sinker EDM, then hand-polished under stereo microscopes to eliminate tooling lines.
2. High-Tonnage Hydraulic Coining or Die Casting Stamped brass blanks are annealed, deoxidized, and struck on 500T to 1000T hydraulic coining presses to compress metal grain into microscopic die details. Die-cast designs are injected with molten Zamak 3 under continuous hydraulic clamping pressure.
3. Rotary Edge Serration & Rim Turning Coin blanks are transferred to secondary lathe stations where outer cylindrical walls receive precision reeding at 0.6 mm pitch, stepped rivet recesses, or CNC diamond-cut rope bevels before electroplating.
4. Multi-Layer Barrier Electroplating Raw blanks undergo ultrasonic alkaline degreasing, copper strike, acid leveling copper, and bright nickel barrier plating (≥ 8-10 μm). Parts receive final 24K real gold flash, bright silver, or chemical sulfide antique bronze darkening.
5. Opaque Enamel Application & Infrared Curing Skilled technicians dispense high-adhesion opaque enamel into recessed heraldic fields using pneumatic dispensers. Filled parts cure in temperature-controlled infrared ovens, ensuring a dense, scratch-resistant surface with zero soft spots.
6. 100% Optical Inspection & Capsule Mounting Every single coin is inspected by hand under 1000-lux daylight inspection lamps for enamel bleed, plating voids, or rim burrs. Qualified pieces are packaged into optical acrylic capsules by technicians wearing lint-free antistatic gloves.
Factory Assurance: Manufacturing standards, metallurgical integrity, and dimensional tolerances are certified by the Director of Quality & Engineering at our Dongguan manufacturing facility. The 3,000 m² plant operates under ISO 9001:2015 quality certification, Sedex SMETA 4-Pillar compliance, and holds authorized Disney FAMA (FAC-086164) and NBCUniversal (L-8360-DT-004) manufacturing approvals.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or contact our engineering team for an itemized factory quotation within 2 to 4 working hours:

• Base Metallurgy: High-tensile stamped H65 brass (density 8.4-8.5 g/cm³) or hot-chamber die-cast Zamak 3 (6.6-6.7 g/cm³)
• Dimensional Range: Standard diameter 44 mm, 50 mm, 57 mm (1.75″, 2.00″, 2.25″); body thickness 3.5-4.5 mm (0.138″-0.177″)
• Tooling Tolerances: Coining die CNC machining: ±0.03 mm (±0.0012″); finished coin outer diameter: ±0.08 mm; thickness: ±0.10 mm
• Heraldic Detailing: Micro-radial sunburst guilloché, fine checkered shield pattern, and raised serif/sans-serif typography
• Edge Treatment: Precision reeded serrated coin rim (0.6 mm pitch), tactical stepped rivets, CNC diamond cut, or laser serialization
• Plating & Coating: Multi-layer barrier plating with polished 24K real gold flash, tactical black, or antique bronze; baked acrylic clear coat
• Quality Benchmark: 48-Hour ASTM B117 Neutral Salt Spray (NSS) passed; ASTM D3359 Grade 5B adhesion; AQL 1.5 Major / 4.0 Mino
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Custom Military Challenge Coins: Ordering & Production FAQ

Why do military commanders insist on stamped brass over zinc alloy for unit coins?

A: Solid H65 brass features a high density of 8.4-8.5 g/cm³, giving each piece substantial physical heft and an authentic metallic chime when tapped during traditional coin-check ceremonies. High-tonnage hydraulic stamping compresses the brass blank, producing razor-sharp typographic edges and flat, flaw-free mirror planes that die casting cannot replicate. Die-cast Zamak 3 is preferred when unit insignia require extreme 3D high relief exceeding 1.5 mm, irregular shield outlines, or pierced interior apertures.

What is the minimum order quantity for custom military challenge coins?

A: Our pilot evaluation batch starts at 50 to 100 pieces (with one-time custom steel tooling). Production economics improve significantly at volume breaks of 300, 500, and 1,000+ units, where initial die machining costs are distributed across the full run. Different plated finishes (such as polished 24K gold for officers and antique bronze for enlisted personnel) sharing identical die geometry can be combined in a single order batch.

Can you match exact military unit colors and insignia specifications?

A: Yes. We match enamel colors directly to official military pantone standards (PMS Solid Coated) under calibrated D65 daylight inspection lighting with color delta held to ΔE ≤ 1.5. If your unit crest contains complex gradients or photographic elements that cannot be rendered in traditional enamel, our engineering team will provide optimized vector proofs incorporating precision screen printing or micro-relief detailing.

How do we initiate artwork evaluation and verify die feasibility?

A: Simply provide your unit patch, digital vector file, or even a clear photograph of an existing challenge coin. Our CAD engineering team will evaluate draft angles, lettering legibility, and relief elevations, delivering a production-ready 3D rendering within 2 to 4 working hours. You can submit your unit insignia or vector files to receive an itemized factory quotation with zero obligation.

How long are unit dies stored for future deployment reorders?

A: We store all custom CNC-machined tool steel dies in our climate-controlled archive for a standard period of 2 years free die retention on reorders (renewed automatically on each production run). Subsequent reorders for upcoming deployments, change-of-command ceremonies, or annual rotations incur a $0.00 tooling fee.

What ethical audits and environmental certifications verify your manufacturing?

A: Gold Valley operates an audited 3,000 m² direct-manufacturing facility in Dongguan certified to ISO 9001:2015 quality standards and audited under Sedex SMETA 4-Pillar ethical guidelines. We hold official Disney FAMA authorization (FAC-086164) and NBCUniversal compliance approval (L-8360-DT-004) for licensed metal manufacturing. All electroplating finishes comply with European EN 1811 nickel release limits (< 0.5 μg/cm²/week) and RoHS 2.0 heavy metal directives.
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email