Wholesale Custom Blank Metal Cufflinks

product banner
round cufflinks
tuxedo buttons and cufflinks
tuxedo studs and cufflinks
cufflink sets
cufflinks wedding gift
custom yellow gold cufflinks
personalised gold cufflinks
personalized gold cufflinks
round cufflinks
tuxedo buttons and cufflinks
tuxedo studs and cufflinks
cufflink sets
cufflinks wedding gift
custom yellow gold cufflinks
personalised gold cufflinks
personalized gold cufflinks
Wholesale Custom Blank Metal Cufflinks
Description :
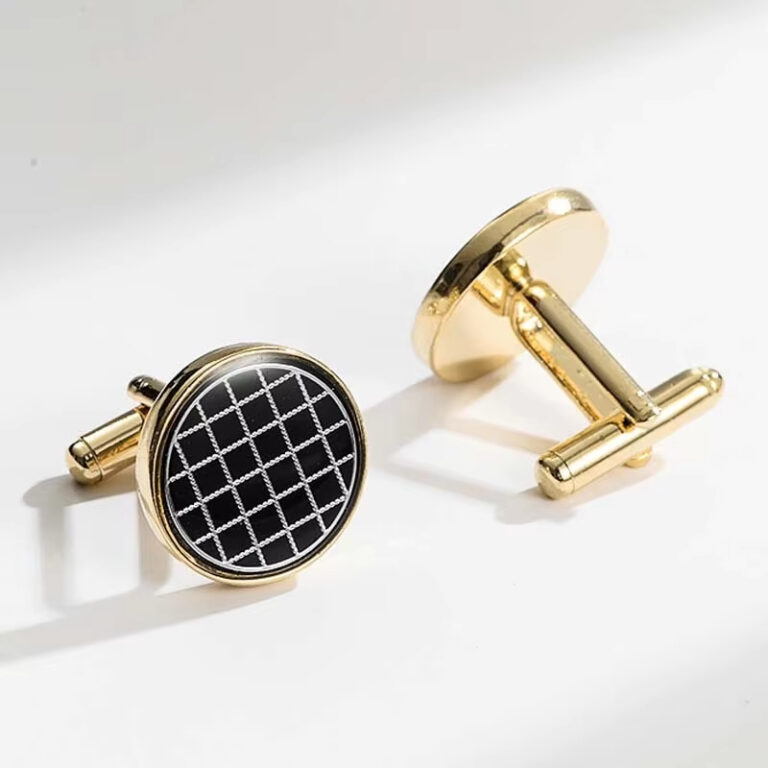
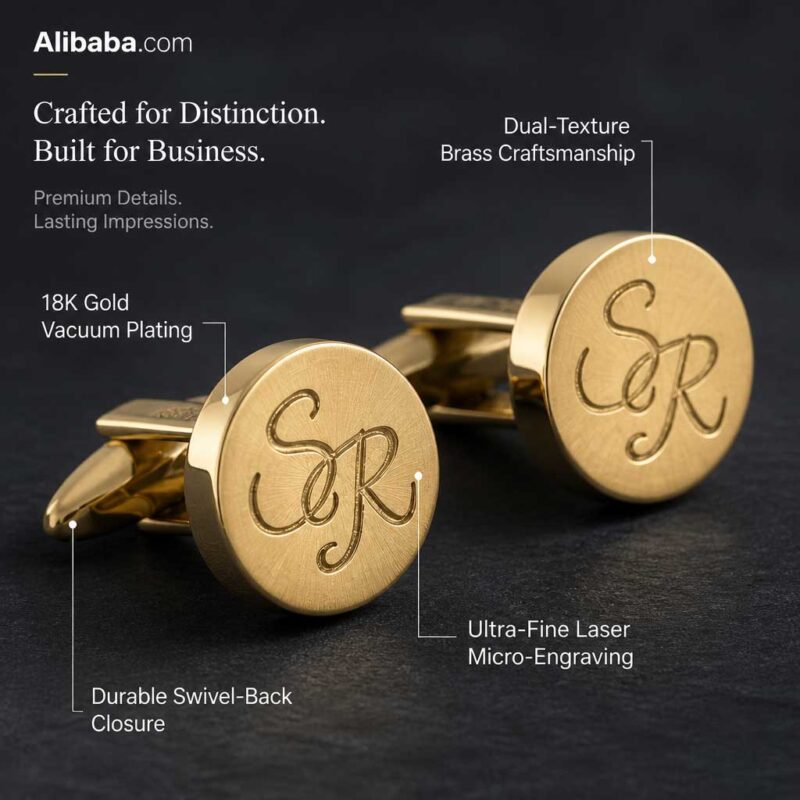
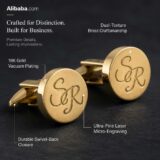
  • Engineered joint strength, zero detached posts. Stamped from solid H65 brass (8.4-8.5 g/cm³) and joined using high-temperature silver brazing with a melting point above 600°C. Each post resists an axial tensile pull of 80 to 100 N (8-10 kgf), eliminating the common industry failure where glued or soft-soldered posts snap off inside tight French cuffs.
  • Snag-free 360° contours and calibrated buttonhole fit. The stem height is calibrated to 7.5-8.5 mm (0.295″-0.335″) to clear four layers of stiff French cuff fabric without pinching, while the 2.8 mm bullet toggle slides effortlessly through 10.0-12.0 mm buttonholes. Every perimeter edge undergoes multi-stage magnetic deburring and cloth-wheel chamfering (R ≥ 0.2 mm) so it will not catch on fine silk linings or tailored wool suit sleeves.
  • Jewelry-grade barrier plating and skin-contact safety. Finished in mirror rhodium, 18K/24K real gold flash, or gunmetal over a heavy bright nickel barrier layer, sealed with an oven-cured baked acrylic protective clear coat (ASTM B117 48h salt spray certified). Fully certified under European EN 1811:2023 for nickel release under 0.5 μg/cm²/week, with dies preserved in our archive for 2 years with zero reorder mold fees.
Base Metallurgy & Density Stamped H65 Brass (8.4-8.5 g/cm³) or Hot-Chamber Die-Cast Zamak 3 (6.6-6.7 g/cm³)
Face Dimensions & Profile Circular bezel: Φ16-20 mm (0.63″-0.79″); square/shield: 15-18 mm; face thickness: 1.8-2.5 mm
Backing Mechanism & Fit Bullet-back toggle with 90° spring-loaded detent; stem height: 7.5-8.5 mm; bullet thickness: 2.5-3.2 mm
Joint Joining Standard High-temperature silver brazing (> 600°C); static axial tensile pull strength ≥ 80-100 N (8-10 kgf)
Skin-Contact Certification European EN 1811:2023 compliant nickel release rate < 0.5 μg/cm²/week; RoHS 2.0 certified
Minimum Order Quantity Pilot batches from 50-100 pairs; volume price breaks at 300, 500, and 1,000+ pairs
Production Turnaround 3D proof: 2-4 working hours | Physical sample: 3-7 working days | Mass run: 12-18 working days
Tooling Retention Policy 2 years free archive retention (renewed automatically on reorders); $0.00 tooling fee on reorders
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Material & Metallurgy High-Tensile Stamped H65 Brass (8.4-8.5 g/cm³) or Die-Cast Zamak 3 (6.6-6.7 g/cm³) Explore Custom Cufflinks Collection
Face Dimensions & Clearance Bezel diameter: Φ16-20 mm (0.63″-0.79″); face thickness: 1.8-2.5 mm; stem clearance height: 7.5-8.5 mm (0.295″-0.335″)
Tooling & Dimensional Tolerances CNC steel die machining precision: ±0.03 mm (±0.0012″); finished face diameter tolerance: ±0.08 mm; stem height tolerance: ±0.15 mm
Post Joining & Tensile Strength High-temperature silver brazing (silver-copper alloy wire, melting point > 600°C); axial pull-test benchmark: ≥ 80-100 N (8-10 kgf / 18-22 lbf) without joint failure
Backing Closure Mechanism Classic bullet-back toggle with internal phosphor bronze spring leaf; 90° positive locking detent; tested to 2,000+ cycle rotation life without loosening
Anti-Snagging Perimeter Finish 360° magnetic fluid deburring and manual cloth-wheel edge chamfering (R ≥ 0.2 mm) to prevent thread pulling on delicate silk suit linings
Plating & Surface Protection Mirror rhodium, 18K/24K real gold flash, rose gold, gunmetal, antique bronze; multi-layer barrier electroplating with baked acrylic protective clear coat (cured at 150°C, 3H hardness)
Corrosion & Adhesion Standards 48-Hour Neutral Salt Spray (NSS) to ASTM B117 with zero blistering or green tarnish; cross-hatch adhesion to ASTM D3359 Grade 5B (0% flaking)
Skin-Adjacent Chemical Safety EN 1811:2023 certified nickel release rate < 0.5 μg/cm²/week (prolonged skin contact standard); EU REACH Annex XVII Entry 27; RoHS 2.0 compliant
Production & Delivery Lead Time Digital 3D Vector Proof: 2-4 Working Hours | Physical Pre-Production Sample: 3-7 Working Days | Mass Production: 12-18 Working Days
Factory Compliance & Audits ISO 9001:2015 · Sedex SMETA 4-Pillar · Disney FAMA (FAC-086164) · NBCUniversal (L-8360-DT-004)

Stamped H65 Brass vs Die-Cast Zamak 3: Selecting the Cufflink Substrate

A pair of cufflinks must balance sharp decorative definition on the front face with mechanical joint integrity on the reverse post. We evaluate the optimal base metal according to sculptural complexity, volume requirements, and post-assembly methods.

• Stamped H65 Brass (High-Tensile Silver Brazing)

Best for: Classic circular and rectangular bezels, flat-polished synthetic hard enamel crests, corporate logo marks, and heirloom gift editions.

  • Tactile Heft & Density: Stamped from dense H65 brass blanks at 8.4-8.5 g/cm³ under high-tonnage friction presses. The piece carries an authoritative, luxurious weight on the wrist, pairing crisp typographic edges with a dense, balanced center of gravity.
  • Structural Joint Integrity: Brass permits high-temperature silver brazing (> 600°C) between the face plate and post stem. The silver-copper filler metal forms a continuous metallurgical bond rated to ≥ 80-100 N tensile pull, completely eliminating post snap-off during daily dressing.
  • Commercial Balance: The standard baseline for fine men’s formalwear and corporate anniversary gifts. For formal lapel badges sharing identical flat enamel finishing techniques, review our Custom Hard Enamel Pins Specification.

• Die-Cast Zamak 3 Zinc Alloy (Intricate 3D Sculptures)

Best for: Complex organic figurines, animal heads, miniature mechanical gear assemblies, and irregular sculptural silhouettes.

  • Tactile Heft & Density: Hot-chamber die-cast at 410°C into pre-hardened H13 steel dies. With a density of 6.6-6.7 g/cm³, Zamak 3 delivers substantial wrist weight while accommodating intricate multi-level sculptural relief up to 2.5 mm depth.
  • Structural Joint Integrity: Zinc alloys melt at ~385°C and cannot withstand high-temperature silver brazing. Posts are secured via low-temperature soldering or recessed mechanical sockets bonded with structural epoxy, holding pull strength to approximately 40-60 N.
  • Commercial Balance: An economical, highly expressive choice for novelty, pop culture, and character-driven menswear programs where 3D sculptural complexity outweighs high-tensile joint demands.
💡 Practical Craft Selection Tip: For formal business shirts, executive anniversary gifts, and designs requiring maximum tensile pull-strength and flat hard enamel, stamped H65 brass is the industry standard. Choose die-cast Zamak 3 when your design features organic 3D figurines, animal heads, or deep multi-level bas-reliefs.

Cufflink Hardware & Bezel Configurations: Six Engineering Variations

The reverse closure and front bezel geometry determine how smoothly a cufflink threads through four fabric layers and stays locked across a full day of movement. We offer six production-tested variations.

Bullet-Back Toggle Closure

Universal French cuff standard

The industry baseline. Consists of a hollow brass post and a torpedo-shaped toggle holding an internal phosphor bronze spring. Rotates parallel to thread through 10 mm buttonholes, then snaps 90° into a locked detent.

Whale-Back Flat Toggle

Sleek modern profile

Features a broad, flat whale-tail closure that pivots smoothly on a stainless steel hinge pin. Lies exceptionally flat against the inner wrist, minimizing bulk under fitted suit sleeves.

Fixed Ball-Return Post

Classic heritage formalwear

A rigid, one-piece curved stem ending in a solid Φ7.0 mm brass sphere. Eliminates all moving mechanical joints for infinite wear life; slips through buttonholes with classic vintage charm.

Traditional Chain-Link Assembly

Tuxedo galas and white-tie events

Connects double decorative face plates via 3 to 4 welded curb chain links (15 mm span). Allows the cuff to drape naturally with generous ease, showing finished jewelry marks on both sides.

Cabochon Bezel Frame with Crystal Dome

Archival prints and vintage cartography

A raised outer retaining bezel housing high-resolution full-color micro-artwork protected beneath an optical-grade crystal-clear dome. Resists everyday scuffing while magnifying fine graphic details.

Recessed Stone & Shell Bezel Inlay

Natural mother-of-pearl and onyx

Precision CNC-milled face pocket with a micro-rolled metal bezel lip. Precision-cut slices of black mother-of-pearl or natural onyx are seated and mechanically crimped, eliminating glue separation.

Special Electroplated Finishes & Compounding Effects

Cufflinks operate adjacent to skin oils, wrist sweat, and suit linings. We apply multi-layer electroplating barriers protected by thermal-cured clear coats to maintain brilliant luster across years of wear.

Process / Effect Technical Formulation & Appearance Best Applications
Mirror Rhodium & Bright Silver Alkaline copper strike, acid leveling copper, and bright nickel barrier (≥ 8-10 μm) followed by precious rhodium or fine silver flash. Delivers a cool, scratch-resistant white metal luster certified to EN 1811. Formal weddings, boardroom business suits, corporate anniversary gifts
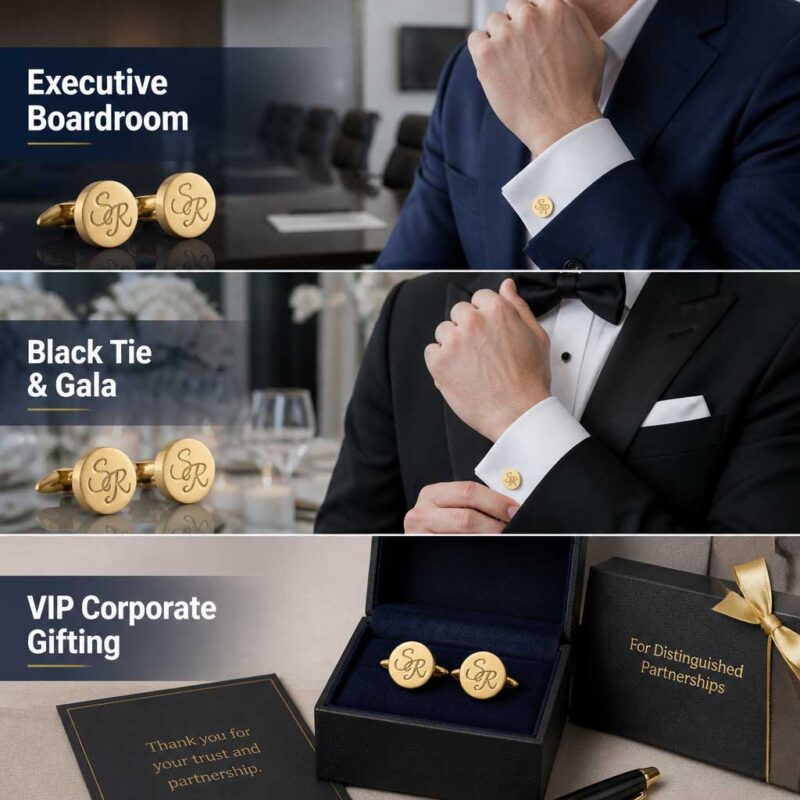
18K Real Gold & Rose Gold Flash High-purity 18K or 24K real gold electroplated over an anti-diffusion nickel barrier layer, sealed with a baked acrylic protective clear coat to maintain warmth without premature rub-off. Black-tie galas, diplomatic presentation sets, executive milestone tokens
Hand-Polished Synthetic Hard Enamel Thermosetting enamel paste is cured at 180°C and ground flat with the surrounding metal lines using oil-stone abrasive wheels. Yields a smooth porcelain finish rated at 3H-4H pencil hardness. Corporate brand seals, heraldic crests, university alumni insignia
Archival Print under Optical Cabochon Dome Micro-offset prints on acid-free substrate sealed under an optical-grade domed resin or mineral glass cabochon. Preserves delicate historical maps and miniature art with dramatic visual depth. Heritage institutions, museum gift collections, bespoke travel commemoratives

For technical electroplating specifications, salt spray ratings, and barrier layer thickness, review our Industrial Electroplating & Finishes Standard.

Retail Presentation & Archival Packaging Solutions

Presentation packaging elevates fine metal cufflinks into store-ready retail accessories and corporate presentation gifts. We configure four standard packaging tiers.

Individual Crystal-Clear Polybag (Included Default)
The zero-cost baseline. Each pair is packed in an anti-tarnish crystal-clear polybag with protective dividers, keeping landed freight weight low on large promotional distributions.
Custom Printed Backing Card with Elastic Tie (Retail Peg Upgrade)
350 g/m² art card printed in full color with elastic mounting loops and a Euro-slot punch. Secures the cufflink pair flat for retail peg hanging while presenting brand graphics.
Optical Clear Snap Capsule with Flocked Inset (Archival Display Upgrade)
Rigid clear polystyrene capsule with a custom die-cut high-density EVA insert flocked in black velvet. Holds cufflinks suspended for 360-degree viewing without handling.
Hinged Velvet or Piano-Lacquer Box (Executive Presentation)
Sturdy hinged steel or wooden presentation box wrapped in plush royal navy velvet or high-gloss piano black lacquer, featuring custom laser-cut velvet recesses for cufflinks and tie bars.
 

From Concept to Creation: Direct-Factory Production & Quality Assurance

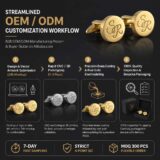
1. Vector Artwork Analysis & Die Machining Your vector artwork is checked 1:1 for line widths and bezel pocket clearances. Tool steel coining dies or injection cavities are machined via high-speed CNC engraving and sinker EDM, holding details down to ±0.03 mm precision.
2. High-Density Stamping or Die Casting Face plates are coined from solid H65 brass on high-tonnage friction presses to achieve razor-sharp typographic edges, or hot-chamber die-cast in Zamak 3 for 3D sculptural reliefs.
3. High-Temperature Silver Brazing Stamped brass face plates and turned stem posts are assembled on ceramic alignment fixtures and brazed using silver-copper filler metal at > 600°C, producing a permanent structural joint.
4. 360° Magnetic Deburring & Mirror Buffing Assembled pieces undergo centrifugal magnetic pin deburring to eliminate micro-burrs, followed by multi-stage manual cloth-wheel buffing to achieve silky, snag-free perimeter edges (R ≥ 0.2 mm).
5. Multi-Layer Plating & Clear Coat Sealing Parts pass through ultrasonic degreasing, copper leveling, bright nickel barrier plating (≥ 8-10 μm), and precious rhodium or 24K gold flash. A baked acrylic protective clear coat is cured at 150°C for sweat tarnish protection.
6. 100% Inspection & Toggle Fatigue Testing Every pair is inspected under illuminated daylight lamps for plating pinholes and bezel alignment. Batch samples undergo 2,000-cycle 90° toggle fatigue tests and destructive 80 N tensile pull testing.
 
Factory Assurance: Manufacturing standards and metallurgical inspections are signed off by Tooling & Quality Director Lin Jianhua (Gold Valley Dongguan Works). The 3,000 m² facility operates under ISO 9001:2015 quality certification and a verified Sedex SMETA 4-Pillar audit.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or submit directly to our Direct Engineering Desk for rapid 2-4h factory pricing:

• Base Metallurgy: Stamped high-tensile H65 brass (8.4-8.5 g/cm³) or hot-chamber die-cast Zamak 3 (6.6-6.7 g/cm³)
• Dimensional Specs: Bezel diameter Φ16-20 mm (0.63″-0.79″); face thickness 1.8-2.5 mm; stem clearance height 7.5-8.5 mm (0.295″-0.335″)
• Joint Engineering: High-temperature silver brazing (> 600°C); static axial tensile pull strength ≥ 80-100 N (8-10 kgf)
• Backing Mechanism: Bullet-back toggle with phosphor bronze internal spring detent; 90° positive locking; 2,000+ cycle fatigue rating
• Edge Treatment: 360° magnetic fluid deburring and cloth-wheel chamfering (R ≥ 0.2 mm) for snag-free suit contact
• Plating & Coating: Multi-layer barrier plating (bright nickel barrier ≥ 8-10 μm) with precious rhodium or 24K gold flash + baked acrylic clear coat
• Compliance Standards: European EN 1811:2023 nickel release < 0.5 μg/cm²/week; ASTM B117 48h NSS passed; ASTM D3359 Grade 5B adhesion
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Custom Cufflinks for Men: Ordering & Production FAQ

Why do you specify high-temperature silver brazing instead of soft solder or glue for cufflink posts?

A: Soft solder (tin-lead) and structural adhesives fail under the torsional leverage applied when threading cufflinks through stiffly starched French cuffs. We use silver-copper brazing filler wire with a melting point above 600°C on our brass cufflinks. This forms an atomic metallurgical bond between the face plate and post, guaranteeing a static tensile pull strength of 80 to 100 N (8-10 kgf) that will not shear off during daily wear.

What is the minimum order quantity for custom cufflinks?

A: Pilot production batches start at 50 to 100 pairs (with one-time mold setup). Pricing scales advantageously at 300, 500, and 1,000+ pairs where fixed tooling costs are fully distributed. Multiple plated finishes (such as mirror rhodium and 24K gold) sharing the same die tooling can be produced within a single order. Contact our desk for an itemized quotation based on your target quantity.

How do you ensure the cufflinks fit standard shirt buttonholes without slipping out?

A: Standard French cuff buttonholes measure 10.0 to 12.0 mm in length. Our bullet toggles are engineered to a cross-sectional thickness of 2.8 mm and rotate parallel to pass smoothly through all four cuff layers. Once rotated 90°, the toggle locks into an internal spring detent, presenting an effective 18 mm anchor width that prevents accidental slip-out. The 7.5-8.5 mm stem height accommodates thick fabric folds without pinching.

Can you match our exact corporate colors and brand graphics?

A: Yes. For enameled designs, we formulate synthetic enamel paste against Pantone Solid Coated references verified under a D65 daylight viewing booth to keep Delta E within 1.5. For printed art cabochons, we use high-definition micro-offset printing protected beneath optical domes. If you only have a rough sketch or logo file, our engineering team will produce a 3D vector proof within 2 to 4 working hours at zero charge. Submit files through our Direct Engineering RFQ Desk.

Are your plated finishes safe for prolonged skin contact and sensitive wrists?

A: Yes. All cufflink components are certified to European standard EN 1811:2023, guaranteeing a nickel release rate below 0.5 μg/cm²/week. The electroplating stack uses an alkaline copper strike, leveling acid copper, and an impenetrable barrier layer sealed beneath a baked acrylic protective clear coat, preventing allergic skin reactions and sweat tarnish.

Can you deliver on tight deadlines for weddings, galas, or corporate events?

A: Standard sampling requires 3 to 7 working days, and full mass production takes 12 to 18 working days. For date-sensitive galas or wedding dates, we offer dedicated rush tooling schedules that deliver physical pre-production samples in 48 to 72 hours. International express air freight reaches North America and Western Europe within 3 to 5 business days.
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email