Custom Metal Belt Buckles | 3D Sculpted Alloy Buckle Manufacturer

product banner
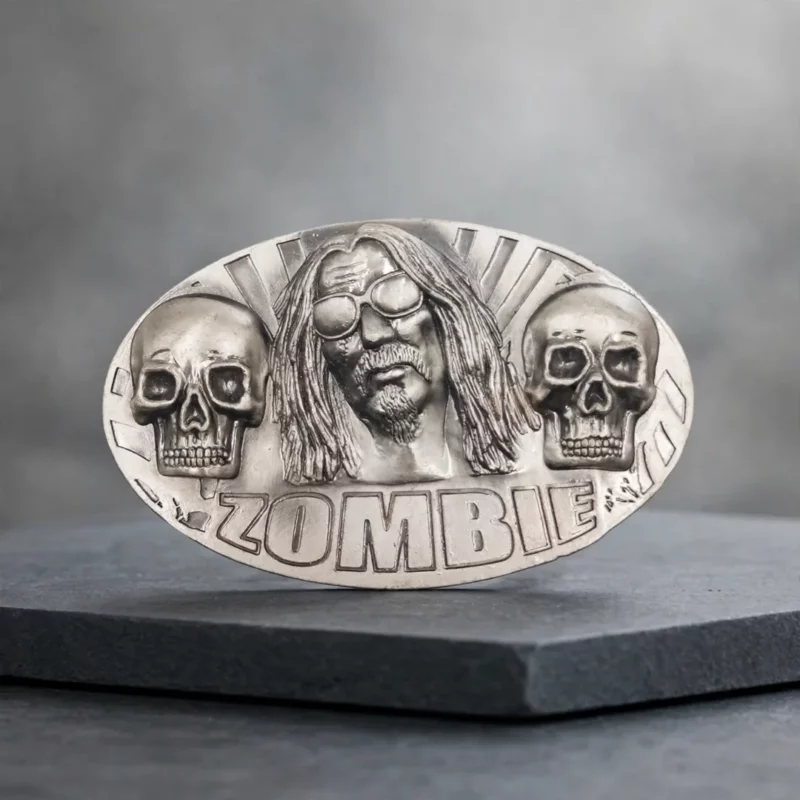
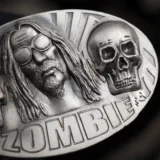
zombie twin skulls oval front studio processed
zombie twin skulls oval front white processed
zombie twin skulls oval macro detail processed
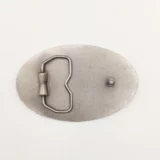
zombie twin skulls oval back white processed
zombie twin skulls oval front studio processed
zombie twin skulls oval front white processed
zombie twin skulls oval macro detail processed
zombie twin skulls oval back white processed
Custom Metal Belt Buckles | 3D Sculpted Alloy Buckle Manufacturer
Description :
  • High-pressure Zamak 5 die casting with 1,000 N tensile resistance. Die-cast in high-grade Zamak 5 zinc alloy (density 6.6-6.7 g/cm³, 330 N/mm² tensile yield strength, 260 N/mm² shear strength), delivering an authentic 120 g to 150 g weighted handfeel. Pinned with a Φ4.0 mm solid steel wire bail loop tested to withstand over 1,000 N (100 kgf / 220 lbs) of sustained axial pull without hinge fatigue or loop distortion.
  • Ergonomic anatomical contour profile eliminates abdominal pinching. Engineered with an intentional R160 mm to R180 mm horizontal curvature that follows natural pelvic contours. Unlike rigid flat plates that dig into the abdomen during seated desk work, driving, or crouching, this arched profile sits flush against leather belts for all-day comfort.
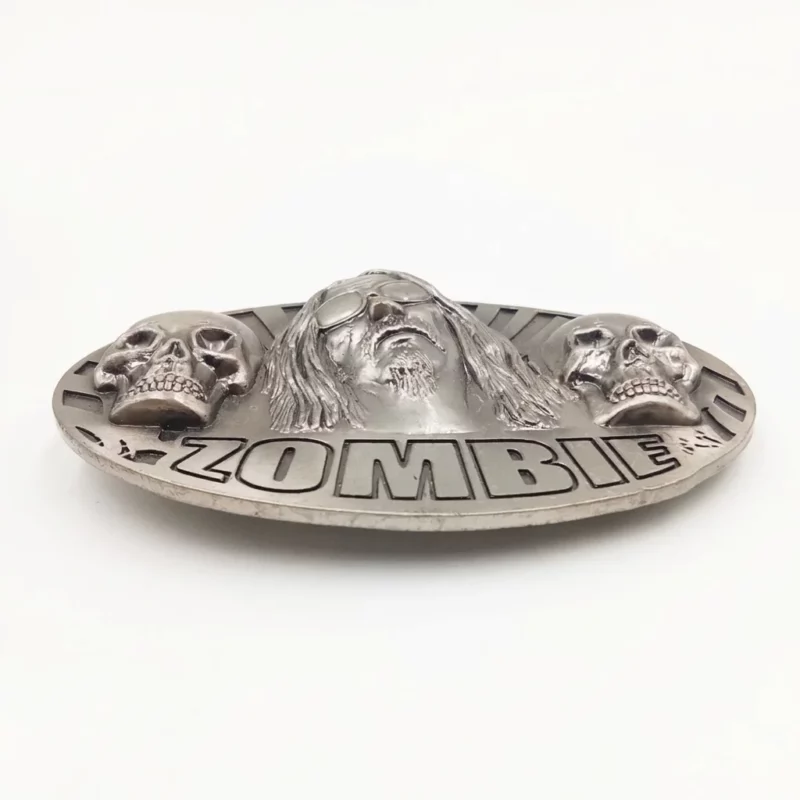
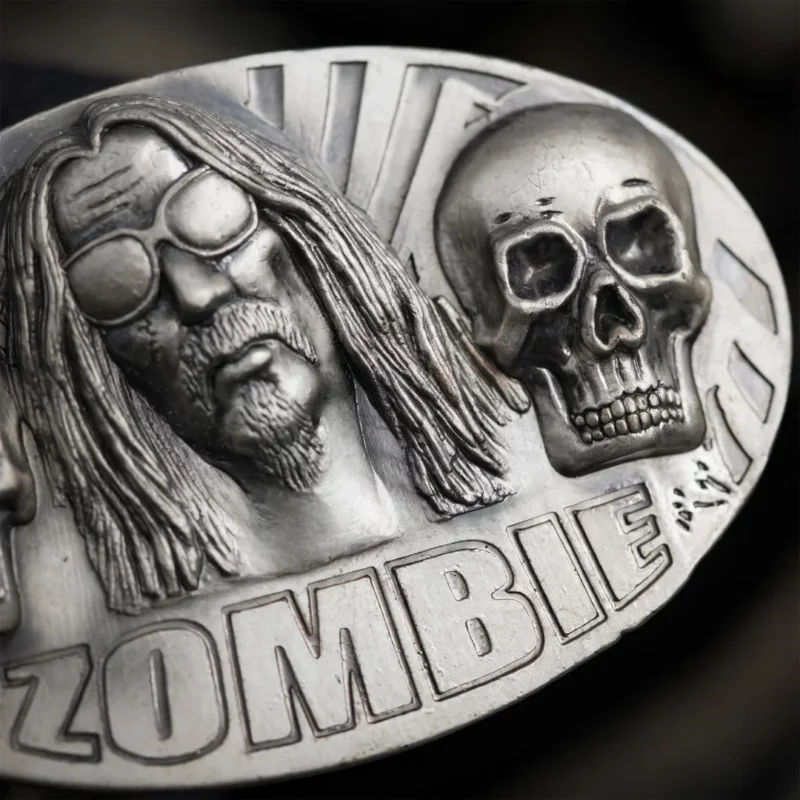
  • Multi-level 3D bas-relief sculpting with crystal protective dome. Precision sinker EDM tooling achieves intricate silhouette cuts, multi-tier parting borders, and contrasting color fills. Protected beneath a high-gloss, non-yellowing crystal polyurethane epoxy dome that guards full-color graphic artwork against buckle scratches and clothing friction.
Base Architecture 3D multi-level sculpted contour plate + integrated hinge brackets + swivel wire bail + fixed undercut prong
Structural Metallurgy High-pressure hot-chamber die-cast Zamak 5 zinc alloy (density 6.6-6.7 g/cm³)
Waist Fit Geometry Ergonomic anatomical contour profile (R160 mm to R180 mm radius curvature)
Hardware & Loop Clearance Φ4.0 mm heavy-gauge steel wire bail (40 mm / 1.57″ inner width) fitting 38 mm (1.5″) belts
Tensile Strength Rating ≥ 1,000 N (100 kgf / 220 lbs) sustained proof pull load on loop and prong
Production Turnaround 2D/3D layout: 2-4 working hours | Tooling & sample: 5-7 working days | Mass run: 12-16 working days
Tooling Retention Policy 2 years free climate-controlled vault storage (automatically renewed on reorders); $0.00 reorder mold fee
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Outer Silhouette Dimensions 108.0 mm × 58.0 mm (4.25″ × 2.28″) batwing contour profile Explore Custom Metal Belt Buckles
Structural Alloy Metallurgy High-pressure die-cast Zamak 5 zinc alloy (ASTM B240 / EN 1774, density 6.6-6.7 g/cm³, 260 N/mm² shear strength)
Plate Thickness & Relief Depth 4.0 mm (0.16″) base structural plate thickness; 3D sculpted bas-relief crest rising to 5.5 mm (0.22″)
Ergonomic Waistline Curvature Anatomical curved cross-section (R160 mm to R180 mm radius); sits flush against waistline without abdominal pinching
Swivel Wire Bail Dimensions Φ4.0 mm cold-drawn 65Mn spring steel / SUS304 wire bail; 40.0 mm (1.57″) inner clearance for standard 38 mm (1.5″) belts
Hinge Bracket Architecture Dual integrated cast brackets (wall thickness ≥ 3.5 mm) with R1.0 mm stress-relief fillet transitions
Locking Prong Mechanics Integrated cylindrical locking peg (length 8.5 mm, Φ4.5 mm mushroom head) with 15° negative undercut angle
Tensile Proof Load Rating Sustained 1,000 N (100 kgf / 220 lbs) static pull test for 60 seconds with 0.00 mm permanent plastic deformation
Surface Inlay & Protection High-definition full-color graphic infill sealed under a crystal-clear, non-yellowing polyurethane epoxy dome
Decorative Plating & Sealing Satin antique silver with sulfide shadow relieving, mirror bright chrome, 24K gold rack plating Explore Industrial Plating Finishes
Global Chemical Safety Standards EN 1811:2023 compliant (nickel release < 0.2 μg/cm²/week); California Proposition 65 compliant (lead < 90 ppm, cadmium < 100 ppm)
Facility Social Compliance ISO 9001:2015 quality certified · Sedex SMETA 4-Pillar audited · Disney FAMA facility authorization (FAC-086164)

High-Pressure Die-Cast Zamak 5 Buckles vs Stamped Brass Buckles

Selecting between high-pressure die-cast Zamak 5 and heavy stamped brass depends on sculptural complexity, relief depth, and production economics. Both provide substantial weight and durability, but their mechanical forming processes solve different merchandise requirements.

• High-Pressure Die-Cast Zamak 5 (Complex 3D Relief & Sculpted Silhouettes)

Best for: Pop-culture franchise merchandise, comic conventions, motorsport clubs, western rodeo awards, and custom corporate lifestyle accessories requiring intricate multi-tier dimensional sculpting.

  • Unlimited 3D Sculptural Freedom: Molten alloy injected at 420°C captures intricate organic contours, sharp perimeter cutouts, and 8-12 mm vertical sculptural variations impossible on mechanical stamping presses.
  • Integral One-Piece Hinge Brackets: The rear hinge brackets and locking prong are die-cast simultaneously with the main plate, eliminating secondary brazing joints and weak solder seams.
  • Balanced Mass Distribution: Tooling incorporates structural cored-out pockets on the reverse, maintaining a solid 130 g to 150 g handfeel while eliminating sink marks and trouser sag.

• Heavy Stamped H65 Brass (Flat Heritage Profiles & Raw Tensile Rigidity)

Best for: Military dress uniform buckles, police department service accessories, luxury heritage leather goods, and minimalist monogram plates where flat planar surfaces are preferred.

  • Superior Raw Tensile Rigidity: Solid forged H65 brass (density 8.5 g/cm³) provides extreme metallurgical hardness and heritage prestige for ceremonial dress apparel.
  • Planar 2D Stamping Limits: Heavy hydraulic presses form crisp 2D line work and shallow coin-style relief (≤ 0.5 mm), but cannot produce steep dimensional undercuts or complex organic silhouettes.
  • Secondary Brazed Wire Hardware: Wire bails and brass prong studs must be hand-brazed at high temperature onto the flat rear plate, increasing unit labor costs on custom runs. Review our Explore Custom Metal Bag Hangers & Hooks for alternative tabletop hardware.
💡 Practical Craft Selection Tip: 💡 Factory Sourcing Rule of Thumb: For comic IPs, motorsport events, and sculpted lifestyle merchandise requiring organic contours and recessed enamel fills, choose high-pressure die-cast Zamak 5. For traditional military dress uniforms and minimalist luxury monogram plates, choose heavy stamped brass.

Buckle Architecture & Waist Ergonomics: Six Core Engineering Features

A commercial metal belt buckle must withstand constant pelvic torque, maintain secure locking engagement under strenuous movement, and sit comfortably against the human body throughout long days. Here is how our engineering department designs each element.

Ergonomic R160mm Anatomical Contour

Lateral curvature radius

The buckle body is cast with a subtle R160 mm to R180 mm curvature matching the natural human pelvic arc. This prevents the upper rim or lower wings from digging into the ribs or abdomen when sitting or bending over.

High-Ductility Zamak 5 Alloy Core

260 N/mm² shear strength

Melted from virgin #5 zinc alloy ingots with 0.75-1.25% copper content. Delivers 330 N/mm² tensile strength and 260 N/mm² shear resistance, preventing brittle fracture at stress-concentrated bracket holes during sudden loads.

Heavy-Gauge Φ4.0mm Steel Wire Bail

40mm strap opening

Formed from hardened 65Mn spring steel or SUS304 wire with resistance-welded joints. The 40.0 mm (1.57″) inner clearance fits standard 38 mm (1.5″) thick leather straps, swinging 180 degrees without binding.

15° Negative-Angle Locking Prong

Anti-slip retention post

The rear cylindrical locking peg features an engineered 10° to 15° negative backward tilt. Outward leather belt tension automatically pulls the prong deeper into the belt hole, preventing accidental detachment during walking or crouching.

Reinforced Hinge Mounting Brackets

R1.0mm stress fillets

Integrated rear brackets feature heavy 3.5 mm wall thickness and smooth R1.0 mm radius fillets at the base junction. Eliminates sharp internal corners where mechanical shearing and stress cracks could develop.

Baked 3H Protective Clear Lacquer

Perspiration barrier coat

Dipped in modified acrylic clear lacquer and baked at 150°C for 25 minutes. Achieves 3H pencil hardness to protect electroplated finishes against acidic body sweat, denim dye crocking, and abrasive friction.

Surface Finishing, Patina Treatments & Custom Inlay Techniques

Surface finishing defines how light interacts with sculpted metal bevels, antique recesses, and colorful emblem artwork. We apply multilayer barrier plating and hand-rubbed patinas sealed beneath industrial protective coatings.

Process / Effect Technical Formulation & Appearance Best Applications
Satin Antique Silver & Pewter Patina Heavy copper and bright nickel base coats followed by chemical sulfide darkening. Hand-relieved across abrasive wheels to reveal bright highlights on raised metal curves while preserving deep charcoal shading in recessed crevices. Vintage comic merchandise, western rodeo buckles, biker motorcycle rallies
Specular Bright Mirror Chrome Plating Multilayer electrolytic finish featuring leveling copper, ductile bright nickel, and hard specular chrome. Polished to an 8K mirror reflection with outstanding resistance against keys, coins, and everyday pocket friction. Modern corporate apparel, automotive enthusiast merchandise, executive gifts
Polished 24K Real Gold Electroplating High-purity 24K gold flash deposited over dense bright nickel barrier layers. Delivers a rich, warm jewelry-grade luster sealed under clear baked lacquer to maintain brilliant festive shine. Championship trophy awards, anniversary commemorations, luxury retail collections
Scratch-Resistant Gunmetal & Black Rhodium Dark alloy electroplating providing a contemporary matte or semi-gloss metallic graphite tone. Resists fingerprint smudges and harsh ambient atmospheric exposure. Tactical law enforcement uniforms, streetwear fashion brands, industrial hardware
Hand-Polished Imitation Hard Enamel High-temperature baked resin paste ground flat and polished flush with raised metal containment ribs. Produces a porcelain-smooth, scratch-resistant surface with vibrant color separation. Official brand logos, university crests, military heraldic insignia
Crystal-Clear Polyurethane Epoxy Dome High-definition CMYK or Pantone spot printed graphic insert sealed beneath a thick, self-leveling crystal polyurethane dome with exceptional UV resistance and tactile depth. Intricate multi-color character art, photographic scenes, licensed pop-culture editions

All electroplated finishes receive an electrostatic dip-coating of baked acrylic clear lacquer (film thickness 8-12 μm, cured at 150°C, pencil hardness ≥ 3H) to guard against hand perspiration and atmospheric tarnish.

Retail Presentation Packaging & Collector Gift Solutions

Tailored packaging solutions transform functional metal belt buckles into collector merchandise ready for retail display, commemorative gift sets, or executive presentations.

Protective OPP Sleeve with Anti-Tarnish Film (Factory Baseline)Individual heavy-gauge clear polypropylene envelope lined with archival anti-tarnish paper. Seals out airborne moisture and eliminates friction scratches during bulk export shipping at zero added packaging cost. Printed Hanging Pegboard Blister Card (Retail Impulse Packaging)Form-fitted clear thermoformed PET blister bubble heat-sealed onto a 350 gsm full-color backing card. Engineered with standard euro-slot hanger hole for commercial retail pegboard hooks in travel plazas and apparel shops. Drawstring Black Velvet Pouch (Collector Edition Storage)Plush woven black velvet pouch with matching double braided drawstring closure. Hot-stamped with metallic silver or gold corporate foil branding, providing soft everyday storage in luggage and wardrobes. Matte Black Rigid Presentation Box with EVA Foam (VIP Gift Box)Heavyweight two-piece rigid cardboard box lined with matte black art paper. Houses a high-density, custom laser-cut EVA foam bed wrapped in plush black velour, securing the buckle upright for unboxing impact.
Packaging options for belt buckles

Packaging options for belt buckles

From Tooling to Quality Assurance: Factory Manufacturing Workflow

1. 3D Digital Sculpting & Tool Steel Machining Customer 2D vector concepts are translated into multi-plane 3D digital CAD topologies. Hardened Cr12MoV tool steel dies are machined via high-speed CNC milling and precision sinker EDM spark erosion.
2. High-Pressure Hot-Chamber Zinc Die Casting Virgin Zamak 5 zinc alloy ingots melted at 420°C are injected into preheated tool steel cavities under 88-ton hydraulic pressure. Rapid solidification yields dense, void-free castings with sharp contours.
3. Vibratory Deburring & Sisal Wheel Buffing Cast buckle blanks undergo vibratory tumbling with ceramic media, followed by coarse sisal wheel polishing and fine cotton mop buffing to produce an 8K specular surface baseline.
4. Multi-Layer Electroplating & Antique Relieving Blanks pass through automated plating lines: alkaline copper strike, acid copper leveling, bright nickel, and decorative silver or gold. Antique finishes are chemically oxidized and hand-relieved.
5. Enamel Infill & Crystal Epoxy Dome Curing Graphic recesses receive soft enamel color dispensing or printed metallic foil inserts, topped with self-leveling polyurethane epoxy resin cured in dust-free convection ovens at 60°C.
6. Wire Bail Assembly & 1,000 N Pull Testing Φ4.0 mm steel wire bails are inserted into rear brackets and mechanically staked. Random batch samples undergo destructive and proof pull testing on universal tensile test machines.
Gold Valley Quality Assurance & Mechanical Engineering Department Every custom metal belt buckle leaving our Dongguan facility reflects rigorous process controls across ISO 9001:2015 frameworks, Sedex SMETA 4-Pillar ethical standards, and full compliance with European EN 1811:2023 nickel release safety.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the technical baseline below directly into your request for quotation, or contact our tooling engineering team for an itemized factory quotation and 3D mechanical layout proof within 2 to 4 working hours:

• Product Category: Custom Metal Belt Buckle (3D High-Relief Sculpted Contour Model)
• Base Dimensions: Width: 108.0 mm (4.25″) · Height: 58.0 mm (2.28″) · Plate Thickness: 4.0 mm · Relief: 5.5 mm
• Metallurgy & Density: High-pressure die-cast Zamak 5 zinc alloy (density 6.6-6.7 g/cm³, 260 N/mm² shear strength)
• Anatomical Curvature: Ergonomic curved cross-section (R160 mm to R180 mm radius) for flush, pinch-free waist fit
• Wire Bail Specification: Φ4.0 mm hardened 65Mn spring steel / SUS304 wire loop; 40.0 mm (1.57″) inner clearance
• Belt Strap Compatibility: Fits standard 38.0 mm (1.50″) leather belt straps (also custom-machined for 44 mm straps)
• Locking Prong Geometry: Cast rear peg (length 8.5 mm, Φ4.5 mm mushroom head) with 15° negative undercut angle
• Mechanical Proof Rating: ≥ 1,000 N (100 kgf / 220 lbs) sustained 60-second tensile proof load without deformation
• Graphic Infill & Coating: Offset printing with crystal polyurethane epoxy dome · soft enamel infill · 3H clear coat
• International Safety Audits: ISO 9001:2015 · Sedex SMETA 4-Pillar · Disney FAMA (FAC-086164) · EN 1811:2023 nickel-safe (< 0.2 μg/cm²/week)
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Frequently Asked Questions: Custom Metal Belt Buckles

How does the ergonomic curved profile improve wearing comfort compared to traditional flat buckles?

A: Human waists and pelvises are naturally contoured rather than flat. A traditional flat buckle acts like a stiff board across the beltline; when you sit in an office chair, drive a vehicle, or crouch down, its straight edges dig painfully into the ribs and lower abdomen. We cast our buckles with an intentional R160 mm to R180 mm radius curvature that drapes naturally across the waistline, distributing pressure evenly and eliminating sharp edge contact.

Will the rear steel wire loop or locking prong bend, loosen, or snap under heavy body strain?

A: No. We construct the swivel bail from heavy-gauge Φ4.0 mm cold-drawn spring steel or SUS304 wire anchored inside reinforced cast brackets with R1.0 mm stress-relieving fillets. The locking prong is engineered with an intentional 15° negative backward tilt so that outward waistband tension naturally pulls the peg deeper into the leather hole. Every production batch undergoes axial tensile proof testing at 1,000 N (100 kgf / 220 lbs) for 60 seconds with zero permanent bending or detachment.

What leather belt strap widths and thicknesses do your rear wire bail loops accommodate?

A: Our standard production wire bail features an internal clearance width of 40.0 mm (1.57″), precisely calibrated for standard 38.0 mm (1.50″) casual, western, and denim leather straps up to 4.5 mm (0.18″) in leather thickness. For heavy-duty tactical webbing or military duty belts, we can custom-cast the brackets to house a 44.0 mm (1.75″) wider wire bail loop upon request.

What are your minimum order quantities, prototype lead times, and mass manufacturing schedules?

A: Pilot production runs begin at 100 pieces per custom die design, allowing brands and event organizers to test merchandise sales without excessive upfront inventory. Custom tooling and physical pre-production samples take 5 to 7 working days; full mass manufacturing takes 12 to 16 working days. Expedited 72-hour prototyping is available for urgent event dates. You can submit your artwork directly to our tooling engineering team to get started.

How long does Gold Valley store our custom steel production dies for future repeat orders?

A: Production tooling dies are cataloged and preserved in our climate-controlled Dongguan factory mold vault for two full years free of charge. Every subsequent reorder automatically renews tooling retention for another two years. When ordering replenishment runs for annual merchandise or seasonal client campaigns, your tooling fee is $0.00. You can review your mold specifications anytime with our tooling engineering team.

What chemical safety, nickel release, and social compliance credentials govern this product?

A: Gold Valley operates an audited direct-manufacturing facility in Dongguan conforming to ISO 9001:2015 quality standards and Sedex SMETA 4-Pillar ethical guidelines. We hold official Disney FAMA authorization (FAC-086164) for licensed manufacturing. All electroplated finishes meet European EN 1811:2023 nickel release thresholds (< 0.2 μg/cm²/week) and California Proposition 65 limits for total lead and cadmium, ensuring hypoallergenic daily skin contact.
Related Products
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email