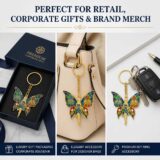
Custom Metal Keychains | Die-Cast Zinc Alloy Factory Direct

product banner
img mw0abj74 923c1f2e
img mw0a682v d5c8f5bc
img mw0a610n b1756fac
img mw0a6ehz 5e789e26
img mw0a6bmk da21e1a6
img mw0a5kk6 24819ce4
img mw0a5ay9 fff22d6d
img mw0abj74 923c1f2e
img mw0a682v d5c8f5bc
img mw0a610n b1756fac
img mw0a6ehz 5e789e26
img mw0a6bmk da21e1a6
img mw0a5kk6 24819ce4
img mw0a5ay9 fff22d6d
Custom Metal Keychains | Die-Cast Zinc Alloy Factory Direct
Description :
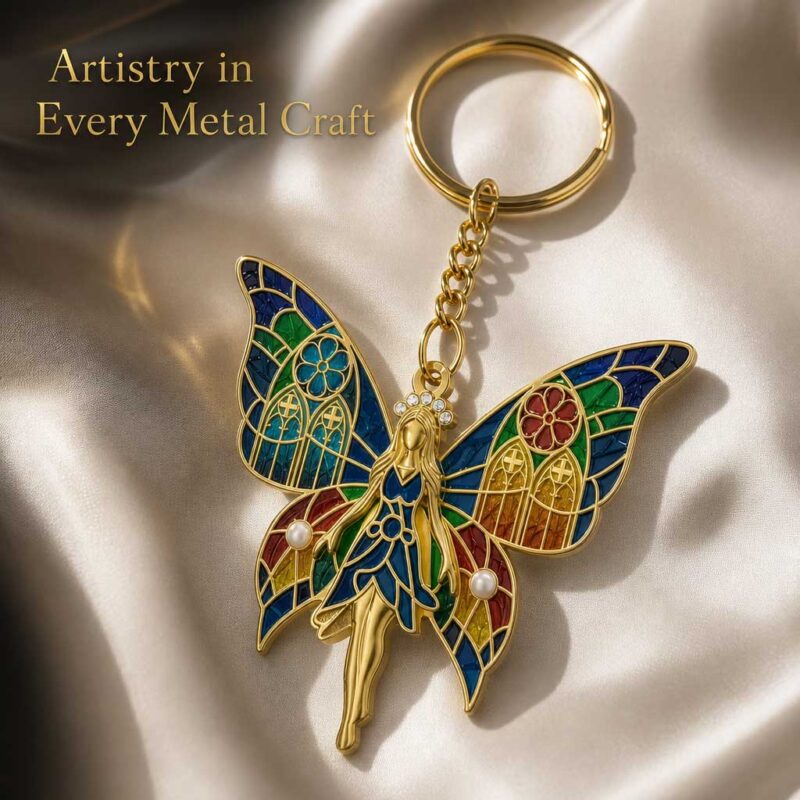
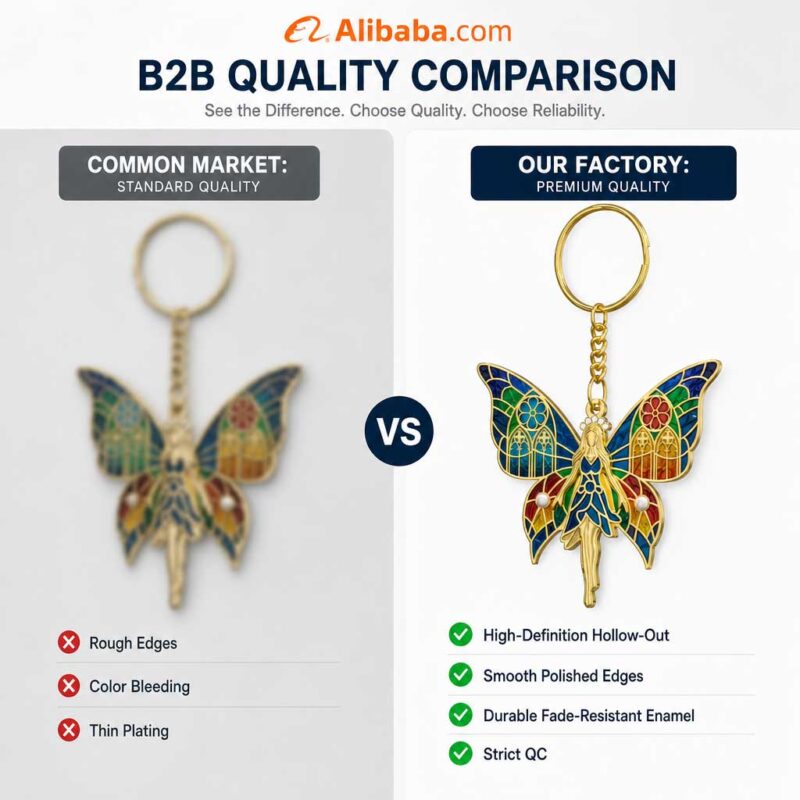
  • Tactile heft and crisp line definition. Pressure die-cast from Zamak 3 zinc alloy at 6.6-6.7 g/cm³ density rather than stamped sheet iron. The piece sits with a reassuring, weighted feel in hand, capturing intricate multi-level contours and clean 0.25 mm (0.010″) enamel separation lines without warping or porous surface pitting.
  • Engineered against daily pocket abrasion. Everyday keys cause severe point contact and friction. Our multi-layer electroplating barrier—alkaline copper, leveling acid copper, bright nickel barrier (≥ 8-10 μm), and finish plating—is sealed under a baked acrylic protective clear coat tested to 48 hours of neutral salt spray (ASTM B117), resisting sweat tarnish and edge chipping.
  • Reinforced hardware and zero-cost reorder retention. Built with an integrated 2.5 mm minimum single-wall eyelet rated to 150 N (15 kgf) axial tensile pull, paired with a heat-treated flat split ring and 360° swivel link that cancels pocket twisting torque. Digital 3D vector proofs are delivered within 2 to 4 working hours, with tooling preserved in our archive for 2 years with zero mold fees on reorders.
Base Metallurgy & Density Hot-Chamber Die-Cast Zamak 3 Zinc Alloy (6.6-6.7 g/cm³)
Standard Dimensions & Profile 40-55 mm × 35-45 mm (1.57″-2.17″ × 1.38″-1.77″); thickness 3.0-4.0 mm (0.118″-0.157″)
Structural Integrity Integrated hanging eyelet single-wall ≥ 2.5 mm; axial pull strength ≥ 150 N (15 kgf)
Attachment Assembly Φ30 mm (1.18″) tempered spring steel flat split ring (100% elastic rebound) + 360° swivel joint
Minimum Order Quantity Pilot batches from 50-100 pcs; price breaks scale at 300, 500, and 1,000+ units
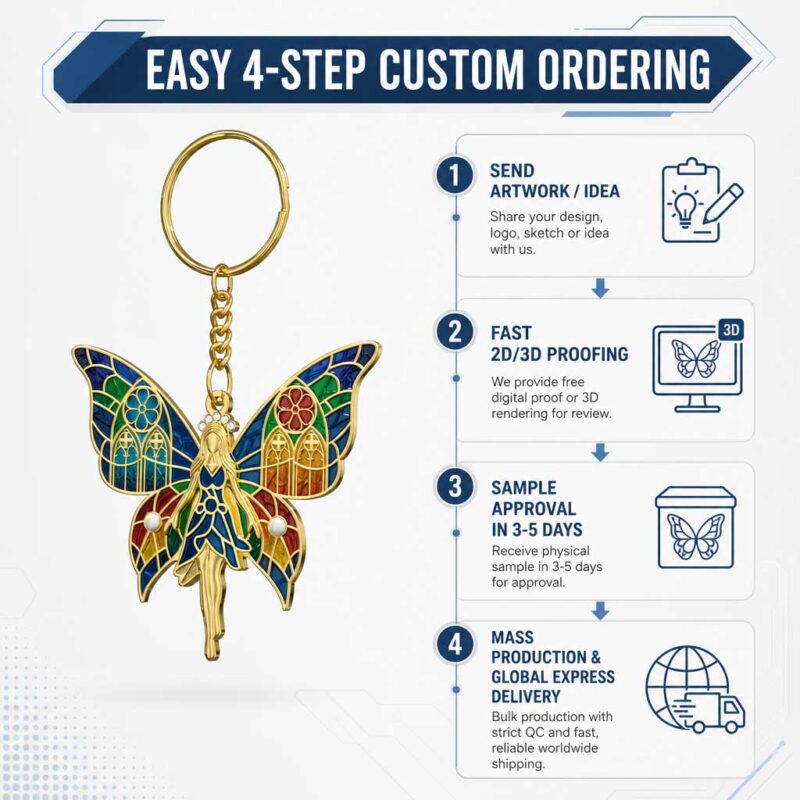
Production Lead Time 3D proof: 2-4 working hours | Physical sample: 3-7 working days | Mass run: 12-18 working days
Tooling Archive Policy 2 years free archive retention (renewed automatically on reorders); $0.00 tooling fee on reorders
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Material & Density Hot-Chamber Die-Cast Zamak 3 Zinc Alloy (6.6-6.7 g/cm³) Explore Custom Metal Keychains Collection
Tooling & Dimensional Tolerances CNC H13 steel die machining tolerance: ±0.03 mm (±0.0012″); finished part outer contour tolerance: ±0.10 mm (after cloth-wheel buffing and plating deposition)
Standard Thickness & Relief Depth Body thickness: 3.0-4.0 mm (0.118″-0.157″); 2D/3D relief height delta: 0.6-1.5 mm; draft angle: 1.5°-3.0°
Enamel Line Geometry & Color Raised metal separator line: ≥ 0.25 mm (0.010″); fill channel depth: ≥ 0.35 mm (0.014″); Pantone PMS Solid Coated matched under D65 daylight (Delta E ≤ 1.5)
Hanging Eyelet & Pull Strength Cast eyelet single-wall thickness: ≥ 2.5 mm (0.098″); deburred internal radius: R ≥ 0.3 mm; static axial tensile load: ≥ 150 N (15 kgf / 33 lbf) without cracking
Connecting Hardware & Ring Rebound Φ30 mm (1.18″) tempered high-carbon spring steel flat split ring (100% elastic rebound, zero residual gap); 360° anti-torsion swivel link
Electroplating & Surface Protection Shiny gold, bright nickel, mirror chrome, gunmetal, antique brass, antique bronze; multi-layer barrier electroplating with baked acrylic protective clear coat (cured at 150°C, 3H pencil hardness)
Environmental & Mechanical Testing 48-Hour Neutral Salt Spray (NSS) to ASTM B117 with zero corrosion; cross-hatch paint adhesion to ASTM D3359 Grade 5B (0% flaking)
Production & Sampling Turnaround Digital 3D Vector Proof: 2-4 Working Hours | Physical Pre-Production Sample: 3-7 Working Days | Mass Production: 12-18 Working Days
Factory Compliance & Audits ISO 9001:2015 · Sedex SMETA 4-Pillar · Disney FAMA (FAC-086164) · NBCUniversal (L-8360-DT-004) · EN 1811 nickel release · RoHS 2.0

Die-Cast Zamak 3 Zinc Alloy vs Stamped H65 Brass: Selecting the Right Base

Both zinc alloy and brass are core metals in commercial keychain manufacturing. The deciding factors come down to dimensional sculpture, cross-sectional thickness, and unit economics across different production volumes.

• Die-Cast Zamak 3 Zinc Alloy (High-Detail 3D Sculpture)

Best for: Three-dimensional character mascots, multi-level architectural bas-reliefs, custom cutouts, and high-volume corporate merchandising.

  • Tactile Heft & Feel: Flowing into high-precision tool steel dies, Zamak 3 fills intricate cavities effortlessly. With a solid density of 6.6-6.7 g/cm³, a 3.5 mm thick cast piece delivers a substantial, tactile hand feel without feeling unwieldy on a car key fob.
  • Visual Detail & Sculptural Freedom: Supports true 3D organic contours, pierced through-holes, and varying cross sections that stamping dies cannot form. Metal separation walls hold sharp definition at 0.25 mm (0.010″), keeping adjacent enamel fills neatly isolated.
  • Commercial Balance: Fast casting cycles and minimal post-machining make die casting the economical choice for runs from 300 to 50,000 pieces. Intricate 3D shapes require no secondary trimming operations.

• Stamped H65 Brass (High-Density Planar Coining)

Best for: Flat corporate medallions, luxury hotel key tags, formal military or service tokens, and designs demanding heavy mechanical rigidity.

  • Tactile Heft & Feel: Heavy cold coining compresses solid H65 brass (8.4-8.5 g/cm³) under high-tonnage friction screw presses, yielding an exceptionally dense, rigid token that produces a distinct metallic ring upon impact.
  • Visual Detail & Sculptural Freedom: Delivers razor-sharp 2D planar crests and micro-engraved typography. However, it cannot achieve fluid 3D organic curves or varying thickness transitions without expensive progressive multi-stage stamping tooling.
  • Commercial Balance: Raw brass sheet carries a higher baseline material cost, making it best reserved for executive milestone gifts, heritage automotive tokens, and premium retail lines. For lightweight, flexible alternatives suited to outdoor sports and casual gear, review our Custom PVC Keychains Specification.
💡 Practical Craft Selection Tip: When your artwork involves organic cartoon characters, varying cross sections, pierced geometric cutouts, or 3D curved surfaces, die-cast Zamak 3 is the standard choice. Choose stamped brass only when your piece is predominantly flat and requires the absolute highest metallic density.

EDC Connecting Hardware: Engineered for Pocket Durability

A custom keychain is only as reliable as its connection hardware. Keys bounce, rotate, and undergo constant mechanical leverage inside pockets and bags. We equip every piece with fatigue-tested fittings engineered to prevent accidental detachment and stress fractures.

Tempered Spring Steel Flat Split Ring

Standard EDC configuration

Stamped from high-carbon spring steel and heat-treated for resilience. The Φ30 mm (1.18″) flat profile spreads open smoothly to receive thick car fobs and snaps back to zero residual gap without permanent deformation.

360° Anti-Torsion Swivel Joint

Pocket carry and tangle prevention

Precision-machined dual-axis brass or zinc swivel link installed between the charm and key ring. It dissipates rotational torque during walking or movement, eliminating torsional fatigue on the chain links.

Heavy-Duty Swivel Lobster Clasp

Quick-clip backpack and belt loop carry

Die-cast zinc alloy carabiner snap hook with a phosphor bronze internal spring mechanism. Pull-tested to 12.0 kgf (26 lbf) retention, allowing users to clip keys quickly onto belt loops, purse rings, or gym lockers.

Horseshoe D-Ring with Screw Pin

Modern automotive smart keys

U-shaped solid zinc alloy shackle secured with an M2.5 stainless steel threaded cross-pin. Assembled with anaerobic threadlocker compound to resist high-frequency engine vibration and prevent accidental loosening.

Reinforced Integral Hanging Eyelet

Heavy daily wear and active carry

Engineered directly into the zinc casting body with a minimum single-wall thickness of 2.5 mm (0.098″) and deburred R0.3 mm internal fillets. Resists over 150 N (15 kgf) of axial pull without stretching or shearing.

Multi-Charm Auxiliary Jump Ring Assembly

Collector sets and multi-piece merchandising

Heavy-gauge welded or tight-coiled brass jump rings (wire diameter ≥ 1.4 mm) configured to mount secondary branded mini-tags, acrylic charms, or engraved serial coins onto a single central key ring.

Special Electroplated Finishes & Compounding Effects

A keychain surface encounters daily coin friction, pocket moisture, and keys. We apply industrial electroplating barriers protected by thermal-cured coats, offering diverse visual treatments suited to different brand styles.

Process / Effect Technical Formulation & Appearance Best Applications
Mirror Chrome & Polished Gold High-leveling acid copper undercoat, followed by ≥ 8-10 μm bright nickel and mirror-polished chromium or 24K gold flash. Sealed with a baked acrylic protective clear coat for exceptional tarnish resistance. Corporate automotive gifts, premium retail merchandise, commemorative editions
Antique Pewter & Brushed Bronze Chemically blackened with liquid sulfide and manually relieved across scotch-brite buffing wheels. Deep recesses retain rich carbon tones while raised relief highlights warm metal; naturally disguises daily micro-scratches. Heritage institutions, museum gift shops, outdoor and motorcycle lifestyle brands
Translucent Enamel & Shimmer Inlay Formulated with semi-opaque pigments or heat-stable mica powder cured over textured metal die cavities. Captures ambient light with depth and visual motion while maintaining a tough, flat protective surface. Gaming accessories, comic convention merchandising, character IP licensing
Two-Tone Selective Masking High-viscosity peelable lacquer is hand-masked across specific design elements before applying the second electroplating bath. Boundary alignment is maintained within ±0.3 mm for razor-sharp multi-metal separation. High-tier corporate anniversaries, executive club tokens, multi-color emblem keychains

For detailed plating stack thickness, salt spray specifications, and masking tolerances, review our Industrial Electroplating & Finishes Standard.

Retail Presentation & Commercial Packaging Solutions

Packaging transforms an industrial metal casting into a store-ready consumer accessory. We supply four standard packaging formats tailored to bulk distributions, retail display pegs, and executive gift programs.

Individual Self-Sealing Polybag (Included Default)
The zero-cost packaging baseline. Each metal keychain is individually sealed in an archival crystal-clear OPP bag to protect electroplated finishes against transit rubbing and scratches.
Custom Printed Backing Card (Retail Peg Upgrade)
350 g/m² coated art board with full-color offset printing, matte lamination, and a standard Euro-slot punch. Keys hang securely on retail pegs; back panel accommodates UPC barcodes and brand storytelling.
Optical Clear Acrylic Display Capsule (Archival Display Upgrade)
Snap-fit optical polystyrene capsule with a custom die-cut high-density EVA foam ring. Holds the keychain suspended in place, providing collectors with 360-degree visibility while protecting against dust.
Hinged Velvet Presentation Box (Executive Gift Presentation)
Sturdy cardboard hinged gift box wrapped in plush black or royal navy velvet, featuring a precision laser-cut velvet-lined EVA insert shaped to your keychain profile. Perfect for automotive handovers and corporate awards.
 

From Concept to Creation: Direct-Factory Production & Quality Assurance

1. Vector Artwork Analysis & Tooling Path Your vector files are evaluated 1:1 for casting feasibility. Relief geometry is cut into pre-hardened H13 tool steel dies via high-speed CNC engraving and sinker EDM, while parting line trimming tools are wire-EDM cut. Separation line widths are verified to meet the ≥ 0.25 mm threshold.
2. Hot-Chamber Die Casting Zamak 3 zinc alloy ingots are liquefied at 410°C in hot-chamber die-casting machines. Liquid metal is injected into the steel mold under high hydraulic pressure, solidifying within seconds with zero internal porosity.
3. Hand Mirror Buffing & Parting Line Deburring Skilled technicians manually dress each raw casting across coarse emery belts to flush parting lines, followed by multi-stage soft cloth-wheel buffing. All outer perimeter edges are rounded to ensure a snag-free touch in pockets.
4. Multi-Layer Plating & Protective Clear Coat Castings undergo ultrasonic alkaline degreasing, copper strike, leveling acid copper, and bright nickel barrier plating (≥ 8-10 μm) prior to final face plating. The piece is sealed with a baked acrylic protective clear coat cured at 150°C for superior sweat resistance.
5. Precision Enamel Dispensing & Thermal Curing Synthetic enamel paste is precisely batched against Pantone Solid Coated formulations and pneumatically dispensed into recessed cavities. Parts pass through multi-stage temperature-regulated conveyor ovens to fully polymerize each color block.
6. 100% Optical Inspection & Mechanical Testing Every keychain undergoes visual piece-by-piece inspection under illuminated magnifying lamps for plating pinholes, color overflow, or burrs. Batch samples undergo destructive 150 N axial pull testing on dedicated tensile fixtures.
 
Factory Assurance: Manufacturing procedures and quality standards are certified by Tooling & Quality Director Lin Jianhua (Gold Valley Dongguan Works). The 3,000 m² plant operates under ISO 9001:2015 quality certification and a verified Sedex SMETA 4-Pillar ethical audit.

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or submit directly to our Direct Engineering Desk for rapid 2-4h factory pricing:

• Base Metallurgy: Hot-chamber die-cast Zamak 3 zinc alloy (density 6.6-6.7 g/cm³)
• Dimensional Specs: Standard body size 40-55 mm (1.57″-2.17″); thickness 3.0-4.0 mm (0.118″-0.157″); 2D/3D relief height delta 0.6-1.5 mm
• Tooling Tolerances: Steel die CNC machining: ±0.03 mm (±0.0012″); finished part profile tolerance: ±0.10 mm; draft angle 1.5°-3.0°
• Eyelet & Mechanics: Integrated cast eyelet single wall ≥ 2.5 mm; deburred inner fillet R ≥ 0.3 mm; axial tensile strength ≥ 150 N (15 kgf)
• Hardware Fitting: Φ30 mm (1.18″) high-carbon tempered spring steel flat split ring (100% elastic rebound) + 360° anti-torsion swivel joint
• Plating & Coating: Multi-layer barrier plating (bright nickel barrier ≥ 8-10 μm) + baked acrylic protective clear coat; 48-hour ASTM B117 NSS passed
• Quality Standard: ASTM D3359 Grade 5B adhesion; ISO 2859-1 AQL 1.5 Major / 4.0 Minor; Pantone Delta E ≤ 1.5 under D65
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Custom Metal Keychains: Ordering & Production FAQ

What are the primary advantages of die-cast zinc alloy over stamped iron or brass for keychains?

A: Die-cast Zamak 3 zinc alloy allows full 3D sculptural depth, curved ergonomic profiles, and complex pierced cutouts that mechanical stamping dies cannot produce. Stamped iron is flat, lightweight, and prone to edge rust once scratched, while brass carries high raw material costs. Zinc alloy provides a solid, weighted hand feel (6.6-6.7 g/cm³) with exceptional detail replication at an economical production price point.

What is your minimum order quantity for custom metal keychains?

A: Pilot production batches start at 50 to 100 pieces (with one-time mold setup). Commercial volume pricing scales favorably at 300, 500, and 1,000+ units as fixed CNC tooling costs are distributed across the batch. Multiple colorways or character variations sharing identical mold geometry can be batched together in one run. Contact us for an itemized quotation based on your quantity.

How do you prevent the hanging eyelet from snapping during daily pocket use?

A: Eyelet failure is the most common flaw in low-cost metal keychains. We engineer all cast hanging eyelets with a minimum single-wall thickness of 2.5 mm (0.098″) and incorporate internal corner chamfers (R ≥ 0.3 mm) to eliminate micro-stress concentrations. Every production lot is pull-tested to withstand at least 150 N (15 kgf) of axial static pull on a calibrated tensile testing rig.

What vector file formats do you require, and how accurate is color matching?

A: We accept vector artwork in .AI, .EPS, .PDF, or .SVG formats. All enamel color paste is formulated against Pantone Solid Coated guides and verified under a standard D65 daylight viewing booth to keep spectrophotometer Delta E within 1.5. If you only possess a raster sketch or rough reference photo, our engineering team will produce a clean 3D vector production proof within 2 to 4 working hours at zero charge. Submit your draft to our Direct Engineering RFQ Desk.

Can you accommodate tight deadlines for trade shows or corporate launch dates?

A: Standard sampling requires 3 to 7 working days, and mass production runs take 12 to 18 working days. For urgent event deadlines, we operate dedicated rush tooling shifts capable of delivering physical pre-production samples within 48 to 72 hours. International express air transit typically reaches North America and Western Europe within 3 to 5 business days.

What international certifications and audit compliance standards does your factory hold?

A: Our 3,000 m² Dongguan manufacturing plant operates under ISO 9001:2015 quality certification and holds a certified Sedex SMETA 4-Pillar audit. For licensed entertainment and brand merchandise programs, we maintain active Disney FAMA authorization (FAC-086164) and NBCUniversal audit approval (L-8360-DT-004). All electroplated components comply with European EN 1811 nickel release limits (< 0.5 μg/cm²/week) and RoHS 2.0 environmental standards.
Related Products
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email