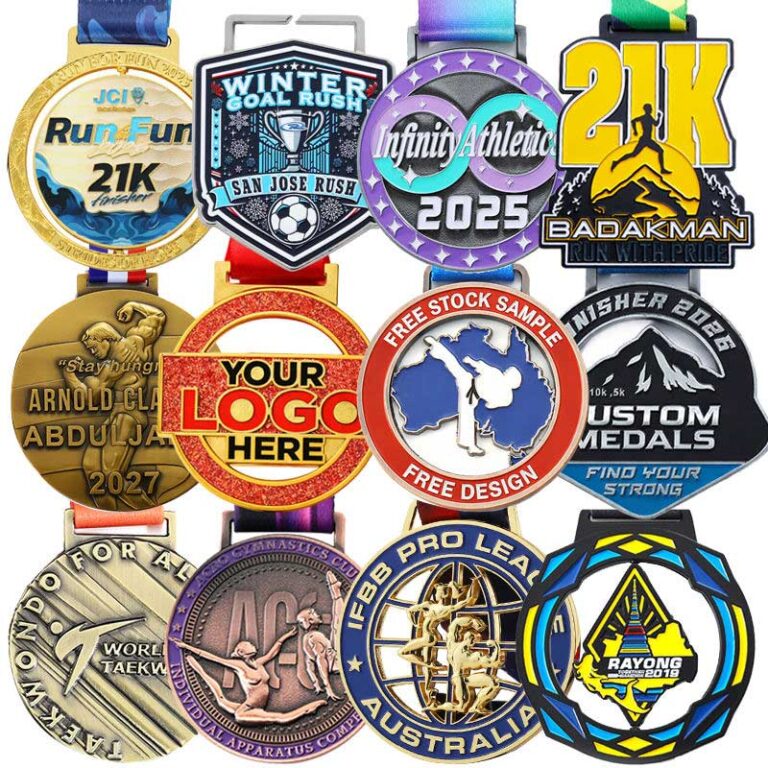
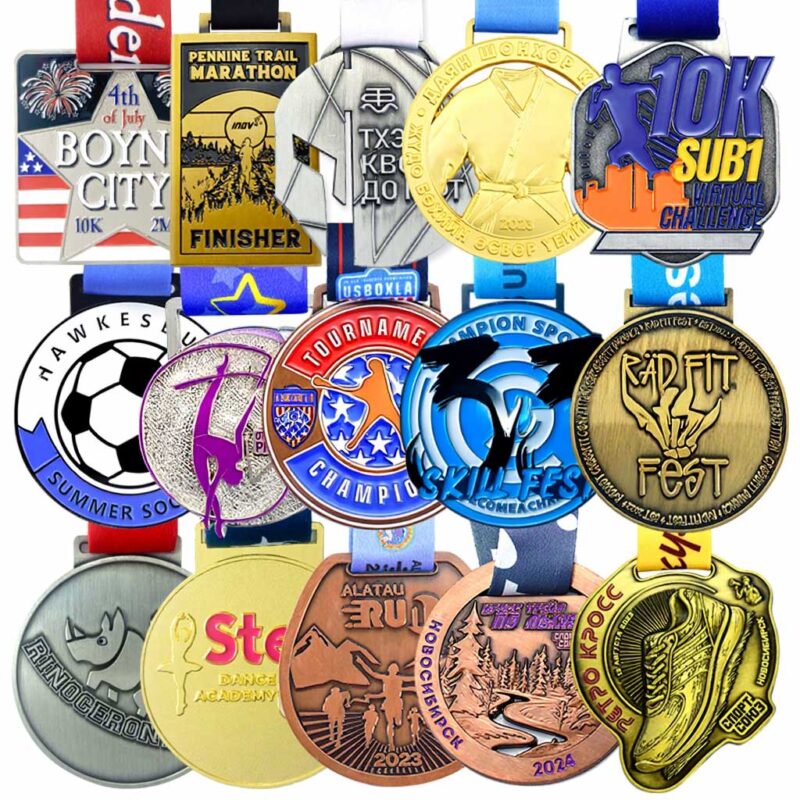
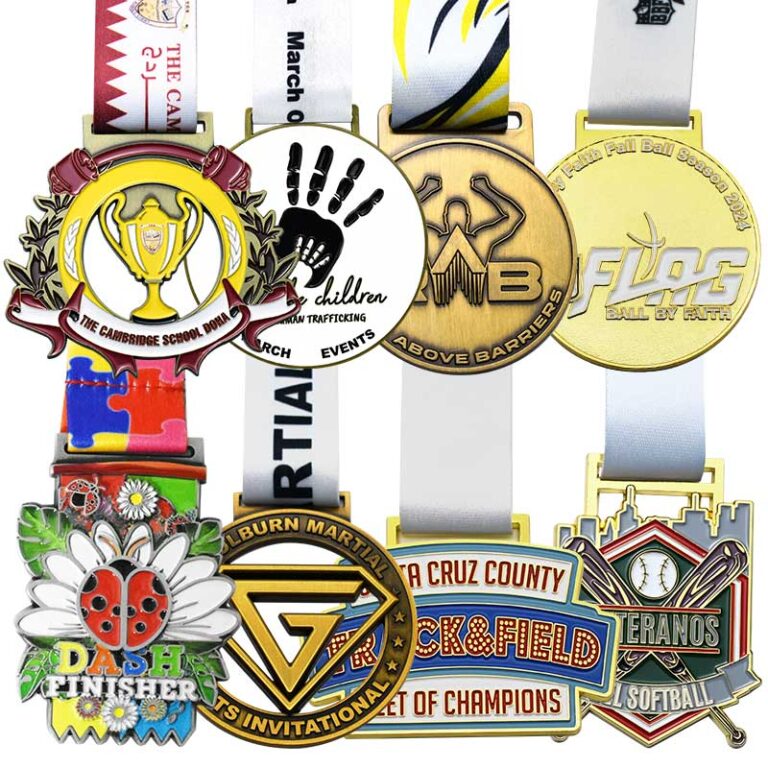
Personalized Metal Craft Award Medals | Gold Valley

product banner
H1398a079a2ba45cb8bc1dd33ae9be550m
H1001c2860f15428b8f963b1a6f62506dP
H71d896349c8841b4acc6c1baf386e5b2c
H62af939c4b7c481bbc295a79e8a690fdk
H9cd0380ad518425da61116ee649f34fb8
H3b1f5b07c60c4e4791b289c16c10f561z
H1398a079a2ba45cb8bc1dd33ae9be550m
H1001c2860f15428b8f963b1a6f62506dP
H71d896349c8841b4acc6c1baf386e5b2c
H62af939c4b7c481bbc295a79e8a690fdk
H9cd0380ad518425da61116ee649f34fb8
H3b1f5b07c60c4e4791b289c16c10f561z
Personalized Metal Craft Award Medals | Gold Valley
Description :
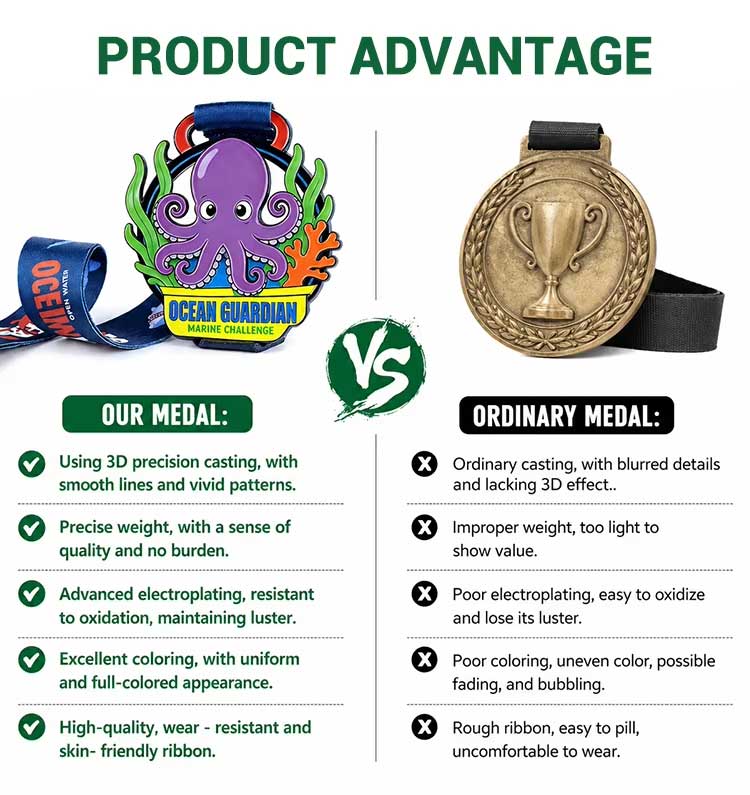
  • Substantial in-hand heft with deep 3D sculptural relief. Die-cast from high-density Zamak 3/5 zinc alloy (6.6-6.7 g/cm³) across standard 70 mm to 90 mm diameters. Generous 3.5 mm to 5.0 mm profile thickness creates an authentic 120g to 180g weighted presence that stays balanced against athletic jerseys at podium ceremonies.
  • Sweat-resistant plating and reinforced safety ribbons. Finished with multi-barrier electroplating sealed beneath a baked acrylic protective clear coat, tested against 48-hour neutral salt spray and synthetic perspiration. Paired with 30 mm or 38 mm high-density polyester neck ribbons secured by double-pass Box-X stitching, rated to withstand 200 N to 300 N sudden vertical pull loads.
  • Rapid 2-4h engineering proofs with 2-year die storage. Receive complimentary 3D production artwork proofs within 2 to 4 working hours, physical evaluation samples in 5 to 7 working days, and your custom tooling stays cataloged in our factory archive for 2 years with zero reorder mold fees.
Base Metallurgy & Density High-pressure die-cast Zamak 3/5 zinc alloy (6.6-6.7 g/cm³)
Standard Dimensions Diameter: 70 mm to 90 mm (2.75″ to 3.54″); thickness: 3.5 mm to 5.0 mm (0.138″ to 0.197″)
Suspension System 30 mm or 38 mm wide high-density polyester ribbon; reinforced Box-X stitching; optional breakaway clasp
Production Turnaround 3D proof: 2-4 working hours | Samples: 5-7 working days | Mass run: 12-18 working days
Tooling Retention 2 years free archive retention (renewed automatically on reorders); $0.00 mold fee on reorders

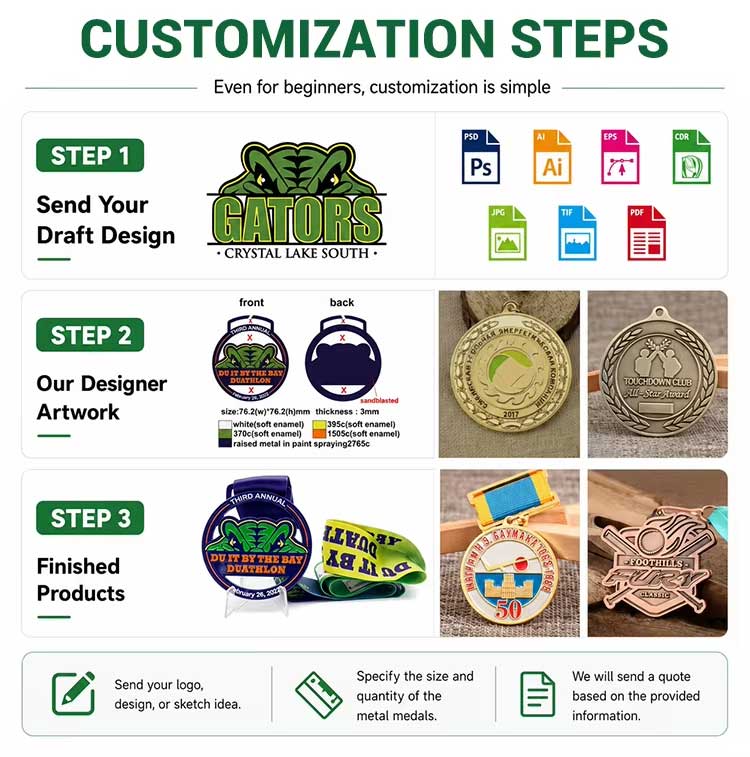
Submit your tournament insignia, event theme, or vector design (.AI, .EPS, .PDF or .SVG) for a line-item direct-factory quotation and a 3D production layout proof within 2 to 4 working hours.
Product Description:

详情 05

详情 07

详情 08

详情 09

详情 10

详情 12

详情 13

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Base Metallurgy & Density High-Pressure Die-Cast Zamak 3 / Zamak 5 Zinc Alloy (6.6-6.7 g/cm³) Explore Custom Sports Medals Collection
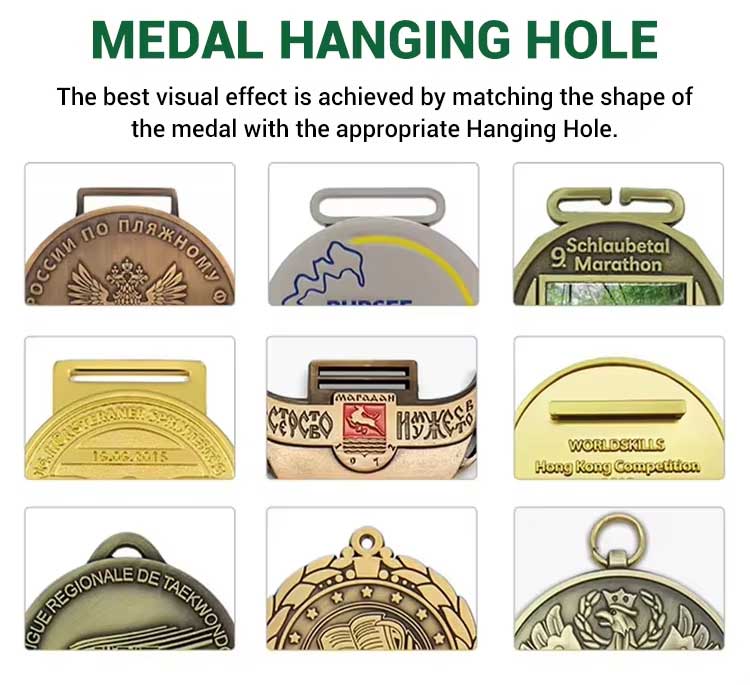
Suspension Loop Construction Integrated die-cast top slot; wall thickness ≥ 2.0 mm; inner edges radiused to R ≥ 0.5 mm and tumble-deburred
Dimensional & Cavity Tolerances CNC tooling cavity precision: ±0.03 mm (±0.0012″); finished medal outer profile: ±0.08 mm after edge buffing
Standard Medal Dimensions Diameter: 70 mm to 90 mm (2.75″ to 3.54″); core body thickness: 3.5 mm to 5.0 mm; relief depth up to 4.5 mm
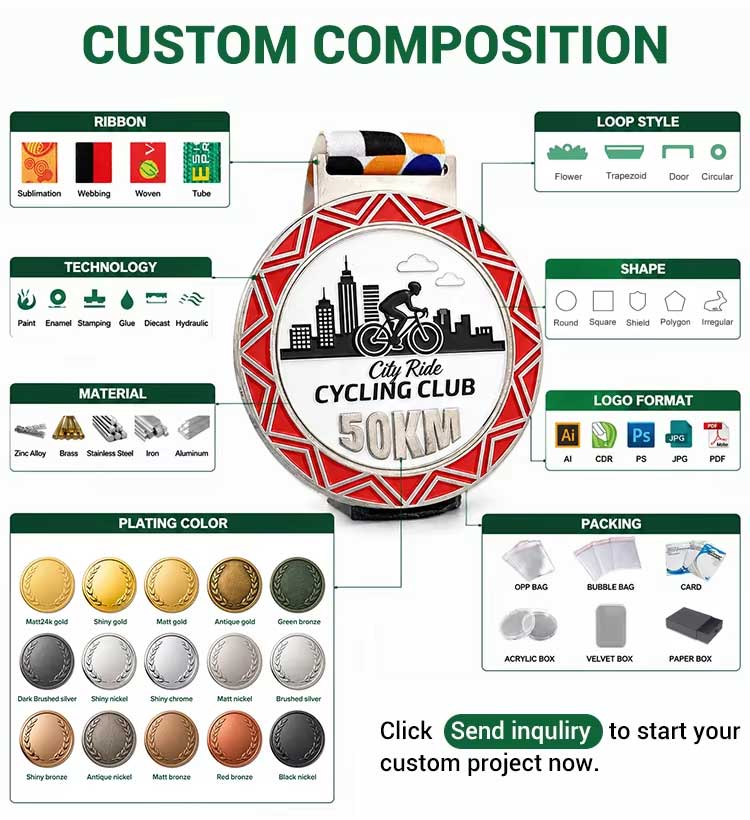
Ribbon Specifications & Weave 30 mm to 38 mm wide high-density polyester ribbon; double-sided 220°C dye-sublimation print; colorfastness Grade ≥ 4.5
Ribbon Stitching & Tensile Rating Reinforced Box-X cross-stitching with bonded nylon thread; instantaneous tensile break load ≥ 200 N to 300 N
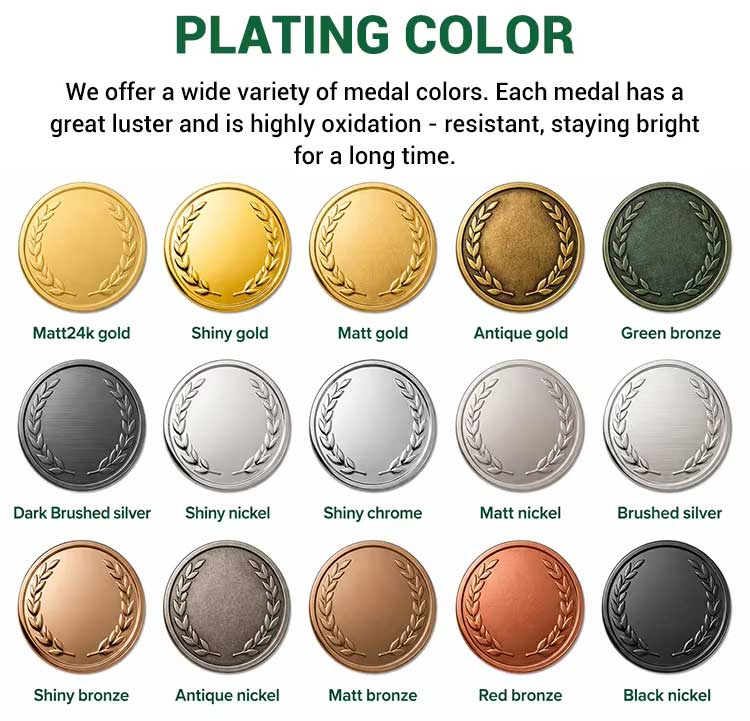
Plating & Protective Sealing Antique bronze, antique silver, bright gold, satin nickel; sealed under baked acrylic clear coat (8-12 μm, 3H)
Corrosion & Sweat Resistance 48-Hour Neutral Salt Spray (NSS) to ASTM B117 / ISO 9227; ISO 3160-2 synthetic sweat resistance (pH 4.7, 48h)
Safety & Regulatory Standards OEKO-TEX Standard 100 Class II (ribbon); REACH Annex XVII Entry 43 (azo dyes) & Entry 27 (nickel release < 0.5 μg/cm²/week)

High-Relief 3D Die-Cast Zinc or Classic Heavy-Stamped Brass?

Selecting the right manufacturing path depends on your medal geometry, dimensional relief depth, and volume budget. Both routes utilize hardened steel tooling, but their metallurgical formation dictates distinct tactile and aesthetic characteristics.

• High-Relief 3D Die-Cast Zinc Alloy (Zamak 3/5)

Best for: Marathon finisher medals, multi-sport tournaments, cycling races, obstacle challenges, and commemorative events requiring bold 3D architectural topography, cutouts, or integrated mechanical bottle openers.

  • Tactile Heft & Balance: Dense Zamak alloy casting produces a substantial 120g to 180g weighted presence. The mass hangs plumb against running shirts, resisting flippant twisting or edge flutter while athletes move across the finish area.
  • Sculptural Depth & Cutouts: Liquid alloy injection under high pressure captures intricate cityscape reliefs, mountain contours, and complete through-hole cutouts without the tooling stress fractures associated with heavy stamping.
  • Commercial Efficiency: Lower tooling entry cost and modular casting cavities make zinc alloy the dominant choice for mid-to-large sporting events requiring intricate multi-tier reliefs within strict per-unit budgets.

• Solid Stamped Brass Insignia (H65)

Best for: Military decorations, state honor awards, academic society medallions, and corporate jubilee medals where razor-sharp planar facets and mirror-like flat surfaces take precedence.

  • Tactile Heft & Balance: Solid H65 brass delivers high density (8.5 g/cm³) with a resonant metallic chime upon contact, imparting traditional institutional prestige.
  • Sculptural Depth & Cutouts: Stamping under heavy friction screw presses yields sharp graphic lettering and mirror-flat background fields, though relief depth remains limited to stepped 2D elevations.
  • Commercial Efficiency: Involves hardened coin-die tooling and heavier baseline material costs. For formal collegiate honors or uniform insignia requiring mirror flat polish, explore our Explore Custom Stamped Medals.
💡 Practical Craft Selection Tip: 💡 Factory Sourcing Rule of Thumb: For sports events, trail runs, and road races with detailed 3D scenery, landmarks, or cutout slots, die-cast Zamak alloy provides maximum sculptural freedom and superior cost efficiency. For formal military-style uniform decorations requiring mirror-flat planes and fine serif lettering, specify stamped H65 brass.

Tournament Suspension Hardware & Ribbon Engineering Options

A championship medal relies on its suspension system as much as its metal core. We engineer dedicated hardware fittings and woven ribbon assemblies tested against vigorous athlete movement and international safety regulations.

Full-Color Sublimated Ribbon

Standard for race branding

Woven from dense polyester yarn and printed via 220°C double-sided thermal gas dispersion. Captures complex sponsor gradients and sharp typography without bleeding, achieving Grade 4.5 wash and sweat colorfastness.

Reinforced Box-X Stitching

High-load assembly anchor

Ribbon folds are secured through automated Box-X perimeter sewing with dual diagonal cross-stitches using bonded nylon thread. Withstands over 200 N of vertical shock load without seam unraveling.

Quick-Release Breakaway Clasp

Youth & school race safety

Molded plastic safety buckle fitted behind the neck releases smoothly under 25 N to 40 N of tensile force. Fully compliant with EN 14682 standards to prevent strangulation risks during youth sports and trail runs.

Heavy-Duty Metal Ribbon Clips

Modular presentation build

Die-cast spring clips or lobster clasps anchored to the ribbon neck allow organizers to attach or swap medals rapidly during finish line staging without hand-sewing individual loop ribbons.

High-Density Jacquard Weave

Premium heritage events

Thread-dyed structural weaving where race titles, heraldic crests, and date milestones are woven directly into the fabric texture, delivering an authentic vintage appearance for traditional regattas and invitationals.

Integrated Top-Slot Casting

Snag-free ribbon passage

The upper ribbon slot is cast as an integral extension of the medal body. Internal tunnel edges are chamfered to R ≥ 0.5 mm and vibratory-tumbled smooth to eliminate sharp burrs that could fray fine satin ribbons.

Special Finishes & Surface Treatment Variations

Surface finishing establishes contrast between raised anatomical figures, architectural landmarks, and recessed background textures. These four proven electroplating and color infill treatments withstand outdoor weathering and podium spotlights.

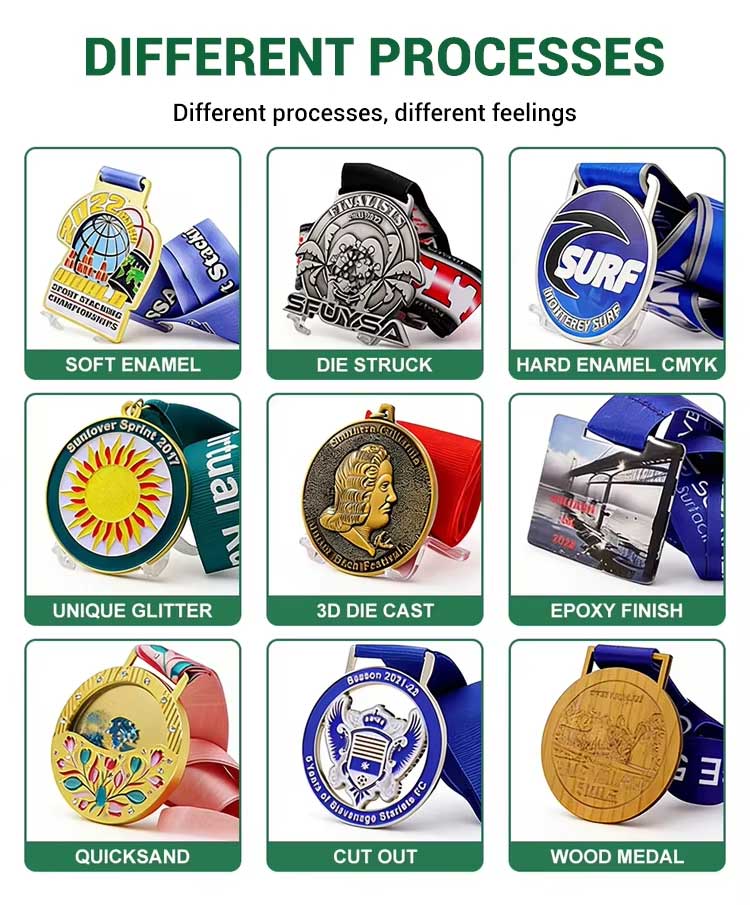
Process / Effect Technical Formulation & Appearance Best Applications
Antique Bronze, Silver & Gold Patina Controlled chemical sulfur darkening followed by hand cloth-wheel relieffing. Dark patina settles into deep topographic crevices while raised lettering and figures gleam with warm metallic highlights. City marathons, trail running, cycling tours, obstacle course races
Mirror-Polished Gold & Bright Chrome Multi-stage copper leveling under bright nickel, topped with electroplated genuine gold flash or specular chrome. Delivers radiant podium reflection under stadium floodlights. Corporate achievement awards, championship tournaments, academic honors
Recessed Vibrant Soft Enamel Color Infill Fluid resin color pastes manually dispensed into recessed metal cavities and oven-cured. Vibrant Pantone PMS colors contrast boldly against raised metal retaining ridges. Youth sports meets, charity 5K/10K fun runs, club athletic leagues
Stained Glass Translucent Tinted Enamel Transparent tinted resin poured across precision pierced cutouts. Ambient light passes through like cathedral stained glass, creating striking visual interest against outdoor skies. Coastal marathons, triathlons, summer solstice festivals, collector series

For comprehensive electroplating bath specifications, salt spray resistance data, and thickness standards, review our Industrial Electroplating & Finishes Standard.

Presentation & Merchandising Solutions

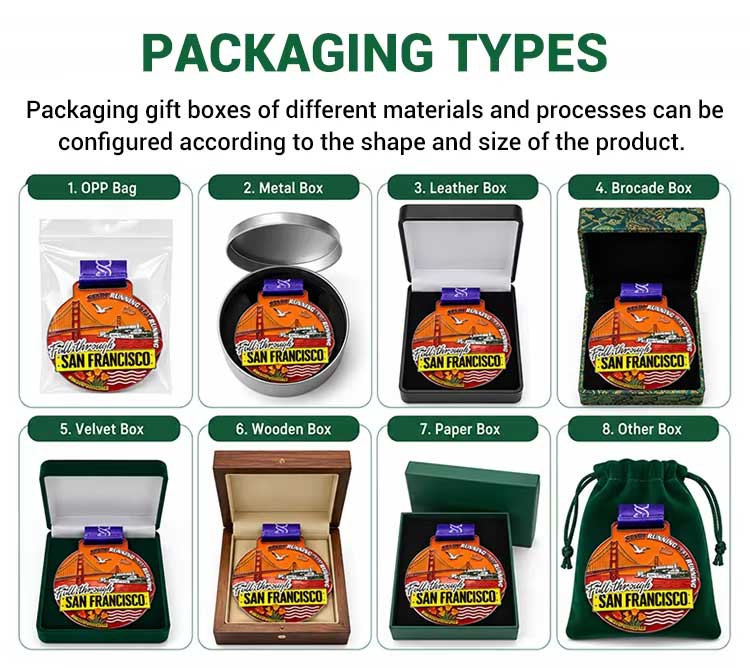
Retail and presentation packaging safeguards medal surfaces from transit friction and creates a tangible sense of achievement during formal presentation ceremonies.

Individual Peel-and-Seal Poly Sleeve (Included Default)
Heavyweight crystal-clear poly sleeve with peel-and-seal adhesive flap. Shields plated surfaces from scuffs and moisture during shipment while providing a lightweight bulk distribution format.
Custom Printed Euro-Slot Backing Card (Retail Peg Upgrade)
350g rigid art paperboard printed in full-color CMYK with Euro-hook hanger slot. Displays race maps, sponsor branding, and barcodes for sports retail merchandising and souvenir shop display.
Archival Clear Acrylic Display Capsule (Archival Display Upgrade)
Two-piece optical acrylic case featuring custom die-cut EVA closed-cell foam inserts. Keeps commemorative finisher medals dust-free and ready for upright mantlepiece or desk display.
Hinged Velvet Presentation Case (Executive Gift Presentation)
Premium spring-hinged jeweler box wrapped in rich navy, royal blue, or burgundy velvet with satin ribbon lid liner and contoured medal recess for presidential and VIP honors.
 

From Concept to Creation: Direct-Factory Production & Quality Assurance

1. 3D CNC Tooling Engraving Tooling engineers translate your vector emblems and elevation drawings into matched H13 hot-work die steel blocks, carved with high-speed CNC cutters down to ±0.03 mm precision.
2. High-Pressure Hot-Chamber Casting Zamak 3/5 alloy is injected into automated hot-chamber die casting machines under high clamping pressure, filling intricate 3D architectural reliefs, through-hole cutouts, and ribbon slots without porosity.
3. Hand Buffing & Slot Deburring Every raw casting undergoes mechanical gate trimming, vibratory tumbling, and multi-stage manual cloth-wheel buffing to remove parting lines and radius the interior ribbon loop edges.
4. Multi-Layer Plating & Anti-Tarnish Bake Cleaned medal bodies pass through ultrasonic degreasing, copper strike, acid copper leveling, and electroplating, sealed under a baked acrylic protective clear coat tested to 48h salt spray.
5. Precision Pantone Color Dispensing Computer-metered color pastes formulated to Pantone PMS standards are dispensed into recessed enamel reservoirs and thermally cured to a resilient, scratch-resistant surface.
6. Tensile Ribbon Assembly & 100% Inspection Technicians stitch sublimated ribbons using reinforced Box-X sewing, verify neck loop pull strength against calibrated test fixtures, and conduct individual optical inspections under daylight lamps.
 
Factory Assurance: Tooling tolerances, ribbon stitching integrity, and plating corrosion resistance are verified under the supervision of Tooling & Quality Director Lin Jianhua (Gold Valley Dongguan Works). Our manufacturing operations adhere to ISO 9001:2015 quality benchmarks, Sedex SMETA 4-Pillar workplace standards, and authorized audit credentials including Disney FAMA (FAC-086164) and NBCUniversal (L-8360-DT-004).

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the baseline below straight into your request for quotation, or submit directly to our Direct Engineering Desk for rapid 2-4h factory pricing:

• Base Metallurgy: High-Pressure Die-Cast Zamak 3 / Zamak 5 Zinc Alloy (density 6.6-6.7 g/cm³)
• Dimensional Envelope: Diameter: 70 mm to 90 mm (2.75″ to 3.54″); core thickness: 3.5 mm to 5.0 mm; relief depth: up to 4.5 mm
• Ribbon Construction: 30 mm to 38 mm wide high-density polyester ribbon; double-sided 220°C dye-sublimation; reinforced Box-X stitching
• Tensile & Safety Standard: Instantaneous suspension break load ≥ 200 N to 300 N; optional EN 14682 breakaway safety release clasp
• Surface Plating & Protection: Antique bronze / antique silver / bright gold / chrome; sealed under baked acrylic clear coat (8-12 μm, 3H)
• Quality Benchmark: ISO 2859-1 AQL 1.0 Major / 2.5 Minor; 48-hour ASTM B117 salt spray certified; ASTM D3359 Grade 5B adhesion
(Engineered to Gold Valley Factory Tolerances — Dongguan Facility)

Personalized Award Medals: Ordering & Production FAQ

How durable is the ribbon attachment, and will the stitching tear under athlete handling?

A: The ribbon connection is engineered for intense celebration. We cast the upper suspension loop as an integral element of the zinc medal body with a minimum wall thickness of 2.0 mm, tumbling inner surfaces to an R ≥ 0.5 mm radius so sharp burrs cannot cut the fabric. The ribbon itself is fastened using automated Box-X perimeter and diagonal cross-stitching in bonded nylon thread, tested to endure over 200 N to 300 N of vertical shock load without thread failure.

Will the plated finish tarnish, blister, or oxidize from sweat during summer marathons?

A: No. Sports medals encounter aggressive exposure to human sweat containing lactic acid and chlorides. Our medal bodies undergo ultrasonic cleaning followed by multi-barrier electroplating, topped with an automated baked acrylic protective clear coat (8-12 μm thickness, 3H pencil hardness). Finished pieces pass 48-hour neutral salt spray tests to ASTM B117 and synthetic sweat immersion to ISO 3160-2 (pH 4.7) without pitting, peeling, or green discoloration.

What is your mold fee policy, and how long do you store production tooling?

A: Your custom steel tooling is preserved in our temperature-controlled factory archive for 2 years free of charge. Tooling retention automatically renews for an additional 2 years upon each reorder run. When you reorder medals for annual championships or recurring race dates, your mold fee is $0.00.

What artwork formats do you require, and how quickly can we review production drawings?

A: We accept vector files in .AI, .EPS, .PDF, or high-resolution layered .PSD formats. If your committee only has preliminary event sketches, raster logos, or architectural reference photos, our engineering desk will construct a 3D production-ready layout proof showing metal elevations and Pantone color mappings within 2 to 4 working hours at no charge. Submit files through our Direct Engineering RFQ Desk.

What are the minimum order quantities, sample lead times, and mass production schedules?

A: Pilot trial runs start from 100 units per design, enabling boutique events or club invitationals to access factory-direct pricing. Significant scale economies unlock at 300, 500, and 1,000+ units where tooling amortizes across the volume. Tooling and physical samples require 5 to 7 working days, while mass manufacturing takes 12 to 18 working days depending on batch size. Rush manufacturing within 72 hours is available for fixed calendar dates.

What factory credentials and product safety standards govern your medal production?

A: Gold Valley operates an audited 3,000 m² facility in Dongguan under ISO 9001:2015 quality certification and annual Sedex SMETA 4-Pillar ethical audits. For licensed client programs, we maintain verified Disney FAMA (FAC-086164) and NBCUniversal (L-8360-DT-004) authorisations. Our ribbons conform to OEKO-TEX Standard 100 Class II and REACH Annex XVII Entry 43 (azo-free dyes), while the metallic castings meet RoHS 2.0 10-substance restrictions and REACH Entry 27 nickel release thresholds (< 0.5 μg/cm²/week to EN 1811:2023).
Related Products
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email