Custom Award Medals | Guitar Cutout Music Medal Factory

product banner
guitar medal irregular front white processed
guitar medal irregular angle studio processed
guitar medal irregular back studio processed
guitar medal irregular hand scene processed
guitar medal irregular front white processed
guitar medal irregular angle studio processed
guitar medal irregular back studio processed
guitar medal irregular hand scene processed
Custom Award Medals | Guitar Cutout Music Medal Factory
Description :
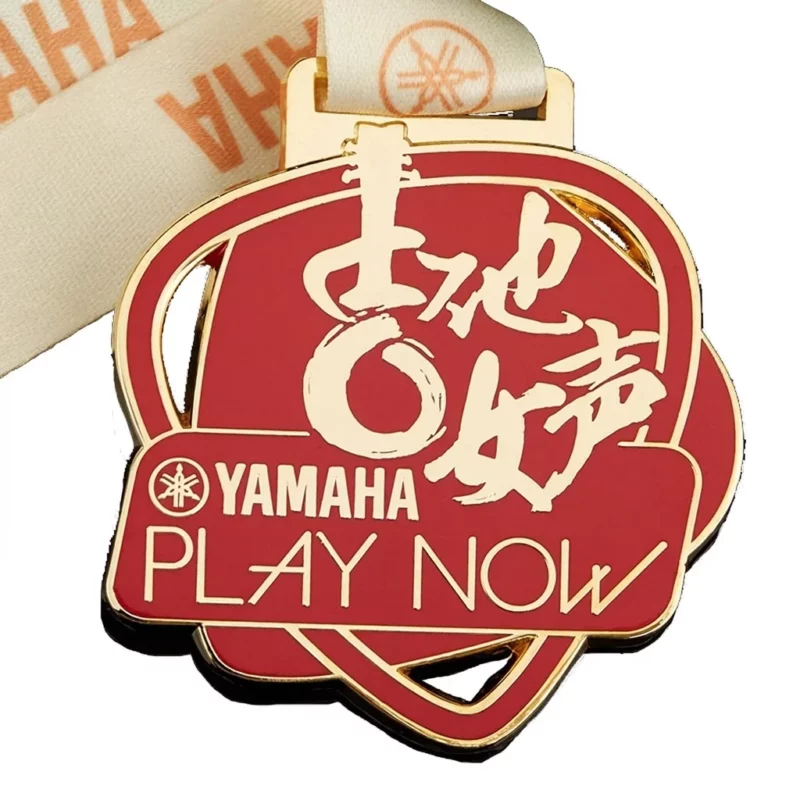
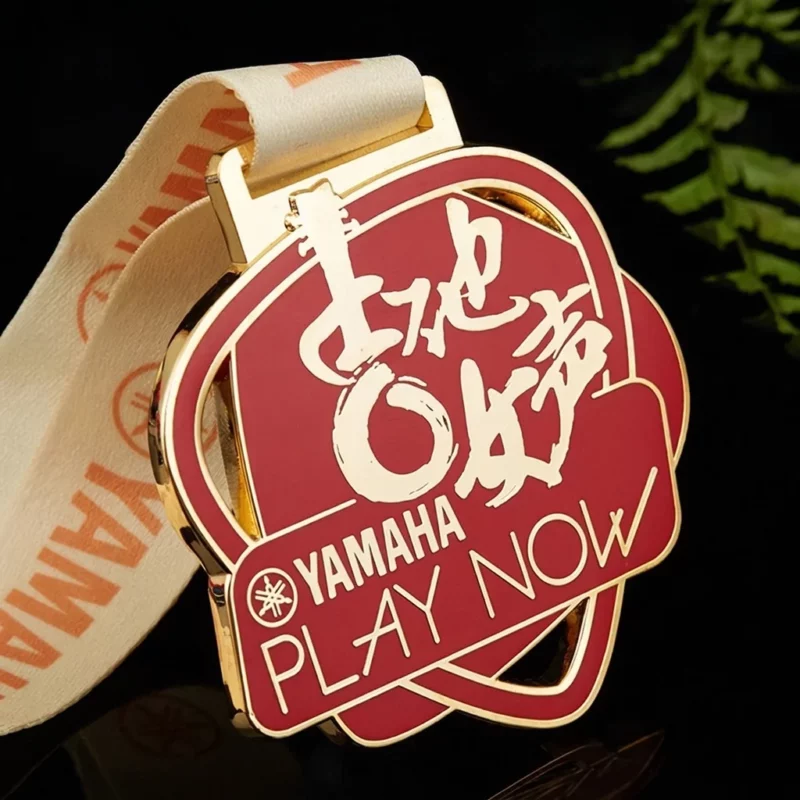
  • Complex pierced cut-out architecture with guitar pick geometry. High-pressure die-cast from Zamak 3 zinc alloy across a 75.0 mm × 68.0 mm (2.95″ × 2.68″) contour, integrating open-work pierced windows, guitar headstock contours, and pick-shaped silhouette layers that conventional metal stamping cannot reproduce.
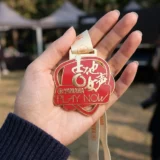
  • Mirror real gold electroplating with recessed crimson soft enamel. Finished in high-luster gold flash plating sealed with a baked acrylic barrier coat, framing deep recessed crimson red soft enamel that cures beneath raised polished metal borders to prevent surface scuffing during podium ceremonies.
  • Heavyweight 85g podium drape with certified 250 N ribbon attachment. Engineered with a 3.5 mm solid profile core providing an authentic 85g weighted drape in hand. Features an integrated cast-in 28 mm suspension bar paired with a Box-X stitched dye-sublimated neck lanyard rated to withstand ≥ 250 N tensile pull force.
Base Metallurgy & Density High-pressure die-cast Zamak 3 zinc alloy (density 6.6-6.7 g/cm³)
Finished Dimensions & Profile 75.0 mm × 68.0 mm × 3.5 mm (2.95″ × 2.68″ × 0.138″); Net medal weight: 85.0 g ± 3.0 g
Surface Plating & Enamel High-polish mirror gold electroplating + recessed crimson red soft enamel infill
Cut-Out & Relief Engineering 3 precision through-hole cutouts + multi-tier raised 3D relievo calligraphy & sponsor typography
Neck Ribbon Assembly 25 mm × 860 mm (1.0″ × 33.8″) high-density polyester dye-sublimated ribbon w/ reinforced Box-X stitch
Production Turnaround 2D/3D proof: 2-4 working hours | Physical prototype: 5-7 working days | Mass run: 12-16 working days
Tooling Retention Policy 2 years free climate-controlled vault storage (automatically renewed on reorders); $0.00 reorder mold fee
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Outer Silhouette Dimensions 75.0 mm × 68.0 mm × 3.5 mm (2.95″ × 2.68″ × 0.138″) contoured guitar pick geometry
Base Alloy & Material Density High-grade die-cast Zamak 3 zinc alloy (density 6.6-6.7 g/cm³) Explore Custom Sports Medals & Awards
Structural Weight & Heft 85.0 g ± 3.0 g (3.0 oz); delivers an authentic weighted presence that hangs stably against clothing
Cut-Out Window Engineering 3 distinct pierced through-hole apertures CNC-machined into the die steel to reduce wind resistance and deliver multi-dimensional visual depth
Tooling & Cavity Precision High-speed CNC engraving tolerance within ±0.03 mm; finished die-cast edge tolerance within ±0.10 mm
Surface Electroplating Finish High-polish mirror real gold flash plating (thickness ≥ 0.05 μm) over alkaline copper and bright nickel base coats
Protective Coating System Thermally baked acrylic protective clear coat (thickness 8-12 μm, 3H pencil hardness) resisting human sweat corrosion
Enamel Infill Chemistry Industrial-grade baked soft enamel (Pantone 201C crimson red) cured at 160°C within recessed metal cells
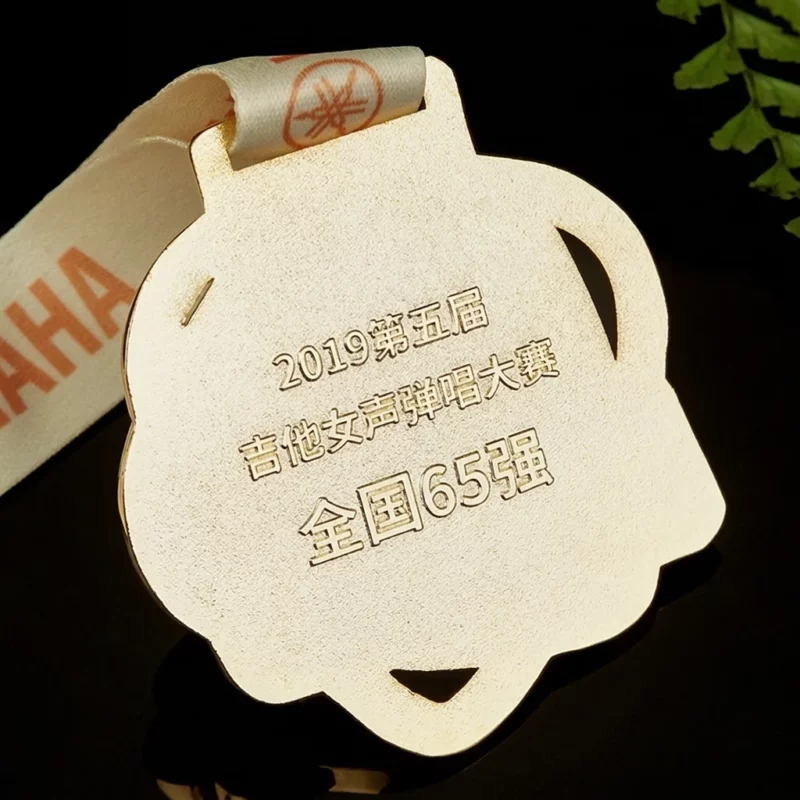
Reverse Texture & Text Uniform micro-sandblasted matte background with raised 3D die-cast commemorative event typography
Suspension Loop Structure Integrated rectangular cast-in ribbon bar (inner slot: 28.0 mm × 5.0 mm; wall thickness ≥ 2.5 mm)
Neck Ribbon Specification 25.0 mm × 860 mm (1.0″ × 33.8″) double-sided continuous dye-sublimated lanyard with heavy-duty Box-X stitch
Mechanical Tensile Benchmark Integrated suspension loop and ribbon seam tested to sustain axial tensile pull forces ≥ 250 N (25.5 kgf)
Corrosion Resistance Rating ASTM B117 48-hour neutral salt spray certified with zero surface blistering, green tarnishing, or plating peel
Environmental Compliance Certified CPSIA lead safety (Pb ≤ 90 ppm), RoHS Directive 2011/65/EU, and OEKO-TEX Standard 100 textile safety
Factory Audit Authorizations ISO 9001:2015 quality certified · Sedex SMETA 4-Pillar audit · Disney FAMA facility authorization (FAC-086164)

Die-Cast Zamak 3 Soft Enamel vs Stamped H65 Brass Hard Enamel

Selecting the appropriate metal forming and colorization method for music competitions, collegiate festivals, and performing arts awards requires balancing intricate cut-out architecture, three-dimensional sculptural freedom, and volume budget parameters.

• Die-Cast Zamak 3 Soft Enamel with Pierced Cut-Outs (Featured)

Best for: Music festivals, instrumental competitions, band tournaments, and artistic performing awards requiring pierced negative space, intricate asymmetric contours, and weighted hand feel.

  • Pierced Geometric Freedom: Fluid molten zinc injection effortlessly fills intricate open-work holes, guitar strings, and multi-layered overlapping contours that mechanical stamping dies cannot pierce without tearing metal sheets.
  • Deep 3D Relievo Definition: Accommodates high-relief sculptural tiers, flowing cursive calligraphy, and raised corporate sponsor lettering framed by 0.35 mm metal boundary ridges.
  • Substantial Weight Economy: High-density alloy (6.6-6.7 g/cm³) delivers authentic 85g hand heft while reducing raw material and machining costs on mid-to-large dimension awards (70 mm to 90 mm) compared to stamped brass.

• Stamped H65 Brass Hard Enamel (Flat-Lapped Traditional Cloisonné)

Best for: Formal governmental civil decorations, university academic honors, and century-old military fraternal orders requiring mirror-flat lapped surfaces and scratch-proof mineral enamel Explore Custom Sports Medals & Awards.

  • Stonelapped Planar Surface: Enamel colors are filled flush with metal ridges and hand-lapped across diamond wheels to yield a flat, seamless jewel-like finish.
  • Mineral Hardness: Vitreous glass-based hard enamel cures into an exceptionally hard ceramic surface (Mohs 6-7) that withstands decades of contact without dulling.
  • Geometric Limitations: High-tonnage stamping presses cannot incorporate internal pierced cut-out windows or complex multi-level 3D fluid transitions, restricting silhouettes to symmetrical discs or starbursts.
💡 Practical Craft Selection Tip: 💡 Engineering Selection Rule: Choose Die-Cast Zamak 3 Soft Enamel whenever your design incorporates musical instruments, architectural cut-outs, asymmetric silhouettes, or multi-tiered relief where physical negative space enhances artistic value. Reserve Stamped Brass Hard Enamel for traditional round or shield-shaped medals requiring a perfectly flat, flush-polished surface finish without pierced windows.

Category-Specific Feature & Hardware Variations

Sublimated Satin Neck Ribbon

Standard Tournament Neck Lanyard

25 mm to 38 mm wide high-density polyester ribbon featuring 220°C dye-sublimation print for razor-sharp multi-color sponsor graphics and sweat-proof washability.

Integrated Heavy-Duty Suspension Bar

Cast-In Structural Anchor

Solid Zamak 3 cast ribbon slot (wall thickness ≥ 2.5 mm) engineered flush with the medal perimeter, tested to withstand 250 N axial pull force without bending.

Precision Pierced Cut-Out Windows

Internal Negative Space Architecture

Multi-station tool-cut apertures within the guitar framework that create striking light transmission and accentuate 3D spatial depth across the front face.

Micro-Sandblasted Reverse Relief

Commemorative Typography Platform

Fine matte sandblast backplate providing crisp visual contrast behind raised 3D lettering, leaving dedicated flat zones for optional laser date engraving.

Safety Breakaway Clasp Option

Youth & Child Safety Mechanism

Quick-release plastic clasp integrated into the neck ribbon that automatically detaches under 25 N to 40 N pull tension to satisfy international youth safety standards.

Reinforced Box-X Ribbon Seam

Heavyweight Stitching Benchmark

Industrial cross-box stitching using bonded high-tensile nylon thread, ensuring the ribbon loop never unravels under the continuous dynamic motion of the award.

Special Finishes & Advanced Compounding Effects

Process / Effect Technical Formulation & Appearance Best Applications
High-Polish Mirror Gold Electroplating Multi-layer electrolytic deposition (acid copper + bright nickel + genuine gold flash) creating brilliant mirror reflectivity across raised ridges. Grand championship first-place trophies and premier honors.
Antique Silver & Antique Bronze Chemical blackening followed by hand-buffed relief highlighting that accentuates deep crevices and guitar headstock fret lines. Second-place, third-place, and vintage collegiate music festivals.
Recessed Industrial Soft Enamel Liquid enamel resin dispensed into sunken recesses and baked at 160°C, producing vibrant gloss color saturation shielded by metal borders. Vibrant festival branding, sponsor emblems, and flag colorways.
Dual-Tone Selective Plating Precision masking allowing simultaneous mirror gold and bright nickel plating across contrasting design zones on a single casting. Special commemorative milestones and anniversary jubilees.

Inspect our complete portfolio of certified electroplating finishes, antique patinas, and ribbon variations on the Gold Valley Factory Customization Services Hub.

Retail Presentation & Archival Packaging Solutions

Individual Self-Adhesive Polybag (Included Default)
Crystal-clear 0.05 mm OPP protective bag sealed with resealable adhesive tape, guarding polished gold surfaces against scratches during transit.
Printed Header Card Polybag (Retail Peg Upgrade)
350gsm artboard header with full-color process printing and standardized euro peg hole, suited for retail music shop racks and merchandise booths.
Deluxe Velvet Drawstring Pouch (Archival Display Upgrade)
Plush midnight blue or black velour pouch with matching braided cords and gold foil stamped event logo for an upscale presentation touch.
Custom Hinged Velour Presentation Case (Executive Gift Presentation)
Premium leatherette or velvet clam-shell gift box featuring contoured high-density foam recessed to match the guitar medal and neatly folded ribbon.
Packaging Types

Packaging Types

From Concept to Creation: Direct-Factory Production & Quality Assurance

3D Digital Sculpting & Toolpath Modeling Engineering artists translate musical vectors into 3D CAD topologies, balancing cut-out drafts, molten metal flow channels, and relief depths.
CNC Steel Die Milling & Sinker EDM Hardened H13 die steel blocks are milled on high-speed CNC centers; pierced cut-out cores are formed via sinker EDM to micron tolerances.
Hot-Chamber Zamak 3 Die-Casting Zinc alloy is injected under 120-ton hydraulic pressure at 420°C, filling complex pierced cavities and flowing contours in a 15-second cycle.
Automated Vibratory Deburring & Edge Buffing Raw castings pass through ceramic tumbling media to deburr parting lines, followed by skilled manual cotton-wheel buffing to mirror luster.
Multi-Color Soft Enamel Infill & Oven Baking Automated dispensing nozzles meter Pantone-matched enamel into recessed cells before passing through a 160°C thermal curing tunnel.
Electroplating, Ribbon Sewing & Final QC Medals receive multi-layer gold plating, are ultrasonic cleaned, and assembled with Box-X stitched neck lanyards under ISO 9001 AQL 1.5 inspection.
Medal Hanging Hole

Medal Hanging Hole

Director of Quality & Engineering Every production lot of custom award medals is manufactured in strict compliance with our documented engineering drawings and ISO 9001:2015 quality management procedures. Our in-house metallurgical testing validates Zamak 3 chemical purity, while finished medals undergo 48-hour neutral salt spray exposure (ASTM B117) and 250 N suspension tensile testing before dispatch under our Disney FAMA authorization (FAC-086164).

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the engineering baseline below straight into your request for quotation, or Request Your Engineering Proof for an itemized direct-factory quotation and 3D digital mechanical proof within 2 to 4 working hours:

• Base Metallurgy & Material Density: High-pressure die-cast Zamak 3 zinc alloy; density 6.6-6.7 g/cm³
• Silhouette Geometry & Dimensions: 75 mm × 68 mm × 3.5 mm (2.95″ × 2.68″ × 0.138″) contoured guitar pick form
• Mechanical Cut-Out Features: 3 precision through-hole cutouts; multi-level 3D relievo calligraphy & lettering
• Surface Electroplating & Coating: High-polish mirror gold electroplating (≥ 0.05 μm) + baked acrylic protective clear coat
• Enamel Chemistry & Pantone Accuracy: High-temperature baked soft enamel (Pantone 201C crimson red); color tolerance ΔE ≤ 1.5
• Reverse Typography & Treatment: Uniform micro-sandblasted matte background with raised 3D commemorative lettering
• Suspension Anchor & Ribbon Assembly: Integrated 28 mm cast bar (wall thickness ≥ 2.5 mm) + 25 mm Box-X stitched sublimated ribbon
• Mechanical & Environmental Ratings: Ribbon tensile load ≥ 250 N; ASTM B117 48h salt spray certified; CPSIA Pb ≤ 90 ppm
*Production baseline: Tooling prototype completed within 5 to 7 working days; bulk production delivered within 12 to 16 working days; tooling cataloged in climate-controlled storage for 2 years with zero reorder mold fees.*

Custom Award Medals: Ordering & Production FAQ

What are the tooling advantages of die-cast Zamak 3 for medals with internal cut-outs?

A: High-pressure hot-chamber die casting in Zamak 3 zinc alloy allows complex pierced through-holes, asymmetrical guitar outlines, and variable profile thicknesses to be cast simultaneously in a single cycle. Traditional metal stamping requires secondary piercing punches that deform sheet metal edges and restrict design complexity. Furthermore, our dedicated steel tooling is cataloged in climate-controlled storage for 2 full years, waiving all die fees on future event reorders.

How do you guarantee exact color matching for festival sponsors on medals and neck ribbons?

A: We calibrate all enamel color fills and dye-sublimation ribbon inks against physical Pantone Formula Guide Solid Coated (PMS C) standards. Our computerized pigment dispensing system controls color boundary tolerances within ΔE ≤ 1.5. For neck ribbons, we employ 220°C high-temperature thermal gas transfer into 300D dense polyester yarns, ensuring vivid, bleed-free sponsor logo reproduction that resists perspiration staining.

What tensile pull strength is engineered into the medal hanging slot and ribbon connection?

A: Our integrated suspension slot is cast directly into the medal perimeter with a robust structural wall thickness of ≥ 2.5 mm. Combined with our industrial Box-X reinforced sewing pattern on the neck ribbon, the complete assembly is calibrated to sustain axial tensile forces of over 250 N (25.5 kgf). This eliminates loop snapping or ribbon tear-out when athletes or performers wear the award on stage or during dynamic celebrations.

What is your minimum order quantity (MOQ) and sample prototyping timeline?

A: Our standard production MOQ is 100 pieces per design, accommodating both boutique regional music recitals and massive multi-city stadium festivals. Following vector artwork confirmation, we provide an engineering layout proof within 2 to 4 working hours. Physical pre-production samples are completed within 5 to 7 working days. Before cutting tooling, connect with our engineering team to Review Your Medal Artwork and verify dimensional parameters.

Can we order staggered medal finishes (Gold, Silver, Bronze) within a single production run?

A: Yes. You can split your total order quantity across multiple electroplating finishes—such as first-place mirror gold, second-place bright nickel or antique silver, and third-place antique bronze—from a single shared casting mold at zero additional tooling cost. Contact our production specialists to Claim Your Free Production Slot and calculate tiered volume pricing.

What chemical and environmental safety certifications apply to your medals and ribbons?

A: All Gold Valley award medals comply with US CPSIA lead requirements (Pb ≤ 90 ppm), the European RoHS Directive (2011/65/EU), and REACH Annex XVII regulations. Our polyester neck ribbons are certified under OEKO-TEX Standard 100 for direct skin contact safety (free from harmful aromatic azo dyes, heavy metals, and formaldehyde). Certified third-party testing documentation can be provided upon order placement.
Related Products
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email