Corporate Challenge Coins | Custom Company Honor Coins Factory

product banner
Company Honor Coins
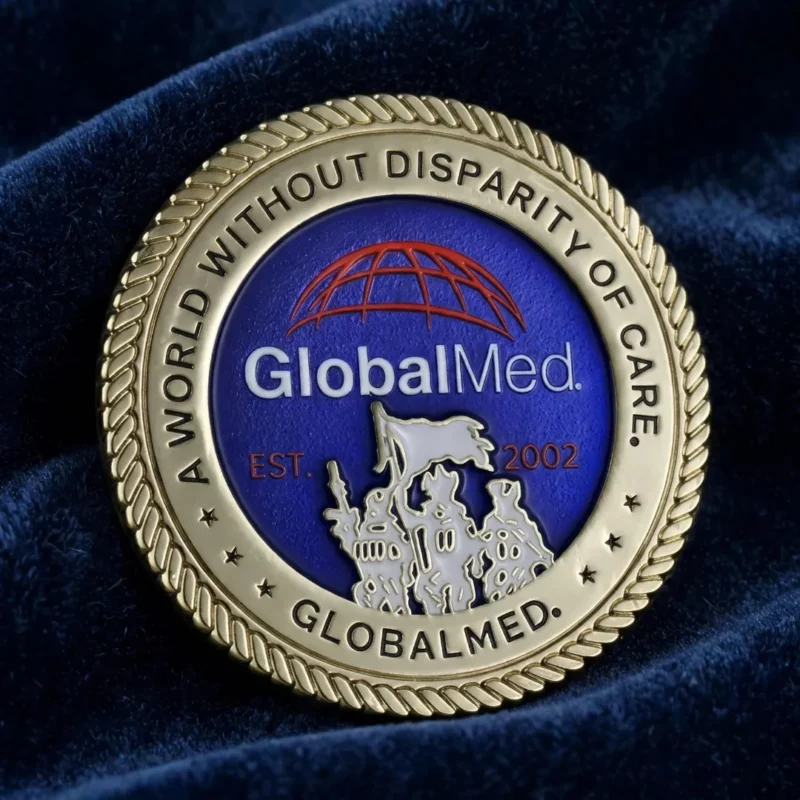
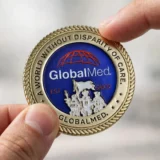
globalmed honor challenge coin gold velvet tray 01 processed
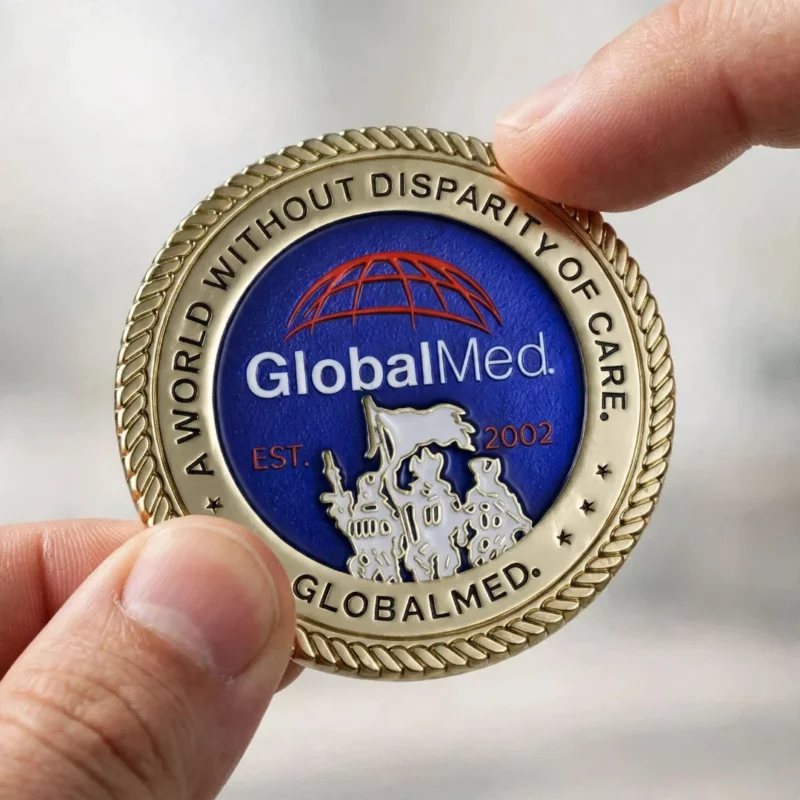
globalmed honor challenge coin gold flip 01 processed
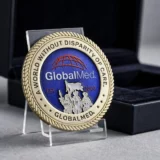
globalmed honor challenge coin gold easel 01 processed
Company Honor Coins
globalmed honor challenge coin gold velvet tray 01 processed
globalmed honor challenge coin gold flip 01 processed
globalmed honor challenge coin gold easel 01 processed
Corporate Challenge Coins | Custom Company Honor Coins Factory
Description :
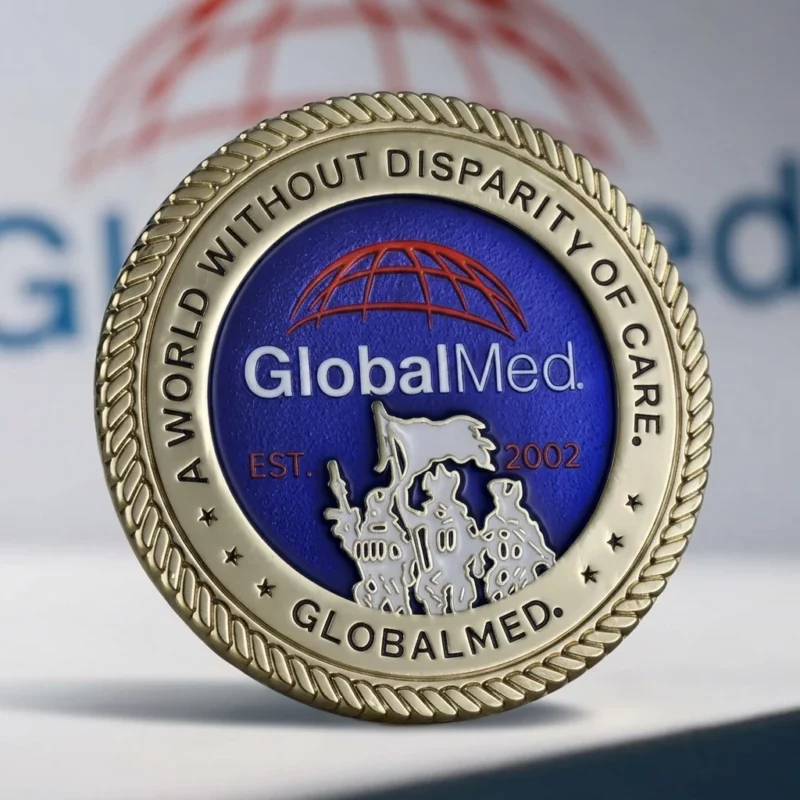
  • Substantial 8.5 g/cm³ brass density with resonant acoustic ring. Precision-struck from solid H65 semi-hard brass under an 800-ton hydraulic coining press across a 1.75″ (44.5 mm) profile, delivering a weighty 58g hand feel and a crisp, clear acoustic chime when flicked or stacked during executive award ceremonies.
  • Precision CNC diamond cut rope edge with multi-layer 3D bas-relief. Features a mechanical 45-degree spiral rope pattern machined by dedicated diamond tooling, framing a deep cobalt blue sandblasted bed, vivid multi-color soft enamel, and raised 3D team figures bordered by 0.35 mm polished gold ridges.
  • Museum-grade mirror gold electroplating with 48h salt spray certification. Plated in high-purity real gold flash with an optically clear, thermally baked acrylic seal that resists acidic skin perspiration and fingerprint oxidation, backed by Disney FAMA (FAC-086164) and ISO 9001 certified manufacturing.
Base Metallurgy & Density Stamped H65 semi-hard brass alloy (density 8.4-8.5 g/cm³; Mohs hardness 3.5)
Finished Dimensions & Profile Diameter: 1.75″ (44.5 mm); Core thickness: 3.5 mm (0.138″); Net unit weight: 58.0 g ± 1.5 g
Outer Edge Milling Pattern Precision CNC diamond cut rope edge (45° spiral braided facets with mirror polish)
Surface Electroplating Finish High-polish mirror real gold flash plating (thickness ≥ 0.05 μm) + baked protective clear coat
Enamel Infill & Background Recessed soft enamel (Cobalt Blue, Crimson Red, White) over micro-sandblasted relief bed
Production Turnaround 2D/3D proof: 2-4 working hours | Physical prototype: 5-7 working days | Mass run: 12-16 working days
Tooling Retention Policy 2 years free climate-controlled vault storage (automatically renewed on reorders); $0.00 reorder mold fee
Product Description:

Product Specifications & Custom Craftsmanship Overview

Specification & Benchmark Gold Valley Direct-Factory Standard
Outer Silhouette Dimensions Diameter: 44.5 mm (1.75″); Core profile thickness: 3.5 mm (0.138″) Explore Custom Challenge Coins
Base Metallurgy & Material Density Stamped H65 semi-hard cartridge brass (density 8.4-8.5 g/cm³); delivers authentic heavy hand heft
Coining Press Tonnage Formed under 500 to 800 tons of instantaneous hydraulic strike pressure for razor-sharp micro-relief
Finished Unit Weight 58.0 g ± 1.5 g (2.05 oz); authoritative physical mass without lightweight hollow resonance
Edge Milling Treatment Four-axis CNC machined diamond cut rope edge with faceted light-reflecting spiral angles
Tooling & Cavity Precision High-speed CNC engraving tolerance within ±0.03 mm; finished diameter tolerance within ±0.05 mm
Surface Electroplating Layer High-polish mirror real gold flash plating (≥ 0.05 μm) over alkaline copper and bright nickel base coats
Protective Sealant Coating Thermally baked acrylic protective clear coat (thickness 8-12 μm, 3H pencil hardness) resisting oxidation
Enamel Formulation & Placement Triple-tone industrial soft enamel (Cobalt Blue Pantone 286C, Crimson Red, White) cured at 160°C
Reverse Background Treatment Uniform micro-sandblasted matte background with high-relief commemorative anniversary typography
Acoustic Resonance Benchmark Struck solid brass produces a sustained high-frequency metallic chime when balanced and struck
Corrosion Resistance Rating ASTM B117 48-hour neutral salt spray certified with zero surface greening, pitting, or plating peel
Environmental Compliance Certified CPSIA lead safety (Pb ≤ 90 ppm), European RoHS Directive 2011/65/EU, and REACH SVHC
Quality Control Standard 100% cotton-glove visual inspection, micrometer edge measurement, and AQL 1.5 / 4.0 sampling before packing
Factory Audit Authorizations ISO 9001:2015 quality certified · Sedex SMETA 4-Pillar audit · Disney FAMA facility authorization (FAC-086164)

Hydraulic Stamped H65 Brass vs High-Pressure Die-Cast Zamak 3

Selecting between solid stamped H65 brass and high-pressure die-cast zinc alloy for corporate challenge coins depends on sensory weight expectations, edge milling requirements, and multi-tier relief geometry. Both metallurgical paths yield exceptional custom medallions, but their mechanical properties fulfill distinct institutional objectives.

• Hydraulic Stamped H65 Brass with Diamond Edge (Featured)

Best for: Corporate anniversaries, executive recognition, board of directors honors, and retirement commemoratives where authoritative physical heft and sharp acoustic resonance signal prestige.

  • Authoritative Density & Heft: Stamped brass delivers a substantial 8.5 g/cm³ density, giving a 1.75″ medallion a commanding 58g weighted drape in the recipient’s palm.
  • Crisp Diamond Edge Milling: Ductile brass enables dedicated four-axis diamond cutting tools to carve mirror-bright rope, cross-cut, or reed patterns directly into the solid perimeter rim.
  • Clear Acoustic Ring: The structural integrity of cold-struck cartridge brass produces a distinct metallic chime upon contact, serving as a traditional tactile hallmark of authentic military and corporate coins.

• High-Pressure Die-Cast Zamak 3 Zinc Alloy (Complex 3D Relief)

Best for: Large-diameter medals (over 2.5 inches), designs requiring pierced through-hole cutouts, or fully rounded 3D high-relief sculptures Custom Military Challenge Coins.

  • Deep 3D Sculptural Flow: Liquid molten zinc injected under hydraulic pressure easily fills multi-level spherical surfaces and deep undercuts up to 2.0 mm relief depth without die deformation.
  • Cost Efficiency on Large Profiles: Low material melting temperature and rapid cycle times provide an economical manufacturing path for oversized medallions or complex asymmetric emblems.
  • Internal Cut-Out Windows: Permits pierced negative space and hollowed-out centers directly from the casting mold without secondary piercing press setups.
💡 Practical Craft Selection Tip: 💡 Engineering Selection Rule: Choose Hydraulic Stamped H65 Brass when your medallion requires maximum hand heft, a traditional coin chime, and CNC diamond cut edge milling (such as rope, wave, or reeded patterns). Choose Die-Cast Zamak 3 when your design incorporates dramatic high-relief 3D portrait sculptures, pierced cut-out windows, or exceeds 2.25 inches in diameter where brass stamping tooling costs become prohibitive.

Category-Specific Feature & Hardware Variations

CNC Diamond Cut Rope Edge

Specialized Rim Faceting

Mechanical four-axis diamond fly-cutter carves 45-degree spiral grooves around the brass perimeter, catching directional light with mirror-bright prismatic flashes.

Sandblasted Cobalt Blue Base

Micro-Textured Negative Space

Uniform fine-grit pneumatic sandblasting creates a matte non-glare bed beneath transparent and soft enamel, providing high visual contrast behind raised polished lettering.

Multi-Layer 3D Team Relief

Bas-Relief Sculptural Realism

Computer-modeled and hand-refined relief carving depicting company founders, staff figures, and architectural motifs bordered by razor-sharp 0.35 mm polished ridges.

Clear Acrylic Display Easel

Executive Desktop Presentation

Sturdy 75-degree angled optical acrylic mini-stand designed for stable desktop or credenza display, allowing both obverse and reverse coin faces to be admired.

Airtight Protective Acrylic Capsule

Archival Preservation Shield

Precision-molded crystal-clear PMMA screw-less capsule with silicone gasket, protecting electroplated and enameled surfaces from humidity, dust, and handling scuffs.

Deep Blue Velour Presentation Box

Deluxe Ceremony Gift Packaging

High-density hinged metal-reinforced presentation case lined in plush midnight blue velvet with a custom circular die-cut cavity for formal award presentations.

Special Finishes & Advanced Compounding Effects

Process / Effect Technical Formulation & Appearance Best Applications
High-Polish Mirror Real Gold Plating Electrolytic deposition of acid copper, bright nickel, and 24K real gold flash (≥ 0.05 μm) creating brilliant mirror reflectivity across raised lettering. Corporate annual awards, founder commemoratives, and executive gifts.
Dual-Tone Gold & Nickel Plating Selective chemical masking allowing mirror gold rims to frame lustrous rhodium-bright nickel central emblems on a single continuous coining blank. Multi-tier corporate departments, merger milestones, and joint ventures.
Antique Bronze & Antique Silver Chemical oxidation immersion followed by hand-buffed relief highlighting that accentuates fine typographic recesses and micro-sandblasted grounds. Heritage company retrospectives, safety milestones, and service longevity.
Deep Translucent Vitreous Enamel Specialized tinted resin suspended over machined guilloché or textured metal bases, yielding deep visual luminescence reminiscent of stained glass. High-tier investor relations, luxury brand gala favors, and club emblems.

Examine our complete selection of certified electroplating finishes, edge milling treatments, and custom packaging configurations on the Gold Valley Factory Customization Services Hub.

Retail Presentation & Archival Packaging Solutions

Individual PVC Coin Pouch (Included Default)
Flexible 0.25 mm clear vinyl sleeve providing basic scratch protection during bulk bulk freight handling and general warehouse storage.
Airtight Acrylic Capsule w/ Display Easel (Retail Peg Upgrade)
Heavy-gauge acrylic capsule paired with an angled transparent mini-easel stand, ready for immediate executive desktop or retail display.
Deep Blue Velour Presentation Box (Archival Display Upgrade)
Hinged hard-shell steel case wrapped in plush midnight blue velour with a satin lid liner, delivering an upscale ceremonial touch.
Custom Lacquered Wooden Presentation Case (Executive Gift Presentation)
Solid natural hardwood box with high-gloss piano lacquer finish, brass hardware hinges, and custom die-cut velvet insert for top-tier milestones.
coins packaging method

coins packaging method

From Concept to Creation: Direct-Factory Production & Quality Assurance

2D/3D Vector Engineering & Bas-Relief Modeling Engineering artists convert client branding into dimensioned 3D CAD models, calibrating draft angles, bas-relief heights, and enamel line separations.
CNC Steel Die Engraving & Cameo Polishing High-tensile H13 die steel blocks are carved on high-speed CNC milling centers and finished with manual diamond paste polishing to achieve cameo contrast.
800-Ton Hydraulic Cold Coining Solid H65 brass blanks are struck under an 800-ton hydraulic press, forcing ductile metal into every micro-cavity with exceptional strike crispness.
Four-Axis CNC Diamond Rope Edge Milling Coined brass blanks are mounted in high-speed rotary fixtures where diamond fly-cutters carve 45-degree faceted rope patterns into the perimeter rim.
Multi-Color Soft Enamel Infill & Curing Computerized micro-dispensing syringes deposit Pantone-formulated enamel into recessed cells before passing through a 160°C thermal baking oven.
Mirror Gold Electroplating & 100% Inspection Medals undergo multi-stage electroplating, baked acrylic clear coating, ultrasonic cleaning, and 100% cotton-glove inspection under ISO 9001 SOPs.
Director of Quality & Engineering Every production run of custom corporate challenge coins is manufactured in strict accordance with our ISO 9001:2015 quality management procedures and documented engineering tolerances. Our metallurgical lab validates H65 brass chemical purity, while finished coins undergo 48-hour neutral salt spray testing (ASTM B117) and 100% cotton-glove optical inspection before packaging under our Disney FAMA authorization (FAC-086164).

[RFQ] Sourcing Spec Sheet (Copy-Paste for Your RFQ)

Paste the engineering baseline below straight into your request for quotation, or Request Your Engineering Proof for an itemized direct-factory quotation and 3D digital mechanical layout proof within 2 to 4 working hours:

• Base Metallurgy & Material Density: Stamped H65 semi-hard cartridge brass; density 8.4-8.5 g/cm³; Mohs hardness 3.5
• Silhouette Profile & Dimensions: Diameter: 44.5 mm (1.75″); Core thickness: 3.5 mm (0.138″); Weight: 58.0 g ± 1.5 g
• Coining Forming Process: 500 to 800-ton hydraulic cold coining press with high-definition bas-relief strike
• Perimeter Edge Milling Pattern: Four-axis CNC diamond cut rope edge (45-degree spiral faceted light-reflecting grooves)
• Surface Electroplating & Clear Coat: High-polish mirror real gold flash (≥ 0.05 μm) + thermally baked acrylic clear sealant
• Enamel Chemistry & Pantone Accuracy: High-temperature baked soft enamel (Pantone 286C blue, red, white); tolerance ΔE ≤ 1.5
• Reverse Typography & Treatment: Fine micro-sandblasted matte background with high-relief commemorative anniversary lettering
• Environmental & Corrosion Ratings: ASTM B117 48-hour neutral salt spray certified; CPSIA Pb ≤ 90 ppm; RoHS compliant
*Production baseline: Tooling prototype completed within 5 to 7 working days; bulk production delivered within 12 to 16 working days; tooling cataloged in climate-controlled storage for 2 years with zero reorder mold fees.*

Corporate Challenge Coins: Ordering & Production FAQ

What makes stamped H65 brass superior to zinc alloy for executive corporate challenge coins?

A: Stamped H65 brass possesses a significantly higher material density (8.4-8.5 g/cm³) compared to zinc alloy (6.6-6.7 g/cm³), providing an immediate, authoritative heft in hand that recipients intuitively associate with high value. Furthermore, cold-coined brass produces a distinct metallic chime when struck, and its structural ductility allows specialized diamond fly-cutters to carve crisp, mirror-bright rope, cross-cut, or wave edges directly into the perimeter rim.

How do you achieve precise corporate brand colors on enameled metal coins?

A: All enamel color formulations are strictly matched against physical Pantone Formula Guide Solid Coated (PMS C) swatches. Our computerized dispensing system meters exact pigment weights to maintain tight color consistency within ΔE ≤ 1.5. Each color bay is enclosed by a minimum 0.35 mm raised metal barrier that prevents pigment bleed while maintaining crisp typographical legibility across small text and intricate corporate logos.

What is your minimum order quantity (MOQ) and sample prototyping timeline?

A: Our standard production MOQ is 50 pieces per design, accommodating boutique board-level recognitions as well as multi-thousand-piece enterprise anniversaries. Following digital vector approval, we deliver a dimensioned 3D mechanical layout proof within 2 to 4 working hours. Physical pre-production samples are completed within 5 to 7 working days. Connect with our engineering team to Review Your Coin Specs and verify tooling parameters before cutting steel dies.

What is your mold fee policy for future milestone reorders?

A: Your dedicated coining die is cataloged and preserved in our climate-controlled vault for 2 full years following your initial order. If your organization places a reorder within that 2-year window, the storage period automatically renews for another 2 years with a $0.00 mold fee. This policy allows companies to reorder coins for ongoing employee service awards or annual events without incurring repeat tooling expenses.

Can we include individualized sequential numbering or recipient names on coins?

A: Yes. We offer precision fiber laser engraving to etch unique sequential serial numbers (e.g., 001/500), employee ID numbers, service dates, or individual recipient names across a designated flat surface on the reverse face or along a smooth outer edge segment. Reach out to our customer engineering team to Claim Your Free Production Slot and review custom variable data engraving options.

How do you prevent electroplated gold coins from tarnishing or showing fingerprints?

A: After undergoing multi-stage electrolytic gold plating, all coins receive an automated spray of high-grade optical-clarity acrylic clear lacquer, which is subsequently baked in a convection oven at 160°C. This forms a transparent, non-yellowing 3H pencil-hardness protective shield that seals the gold layer against human sweat acidity, environmental oxidation, and surface scratches during handling.
Related Products
Leave a Message

If you are interested in any product, please contact us. We will introduce our products to you in more detail

    MESSAGE BOARD


    Products
    Contacts
    WhatsApp
       
    Email